Water-Based Coatings for Bags: Do They Match Solvent Performance?
Water-Based Coatings for Bags: Do They Match Solvent Performance?
Water-based coating is usually sold to a bag factory as a drop-in replacement for solvent coating. It is not one. The chemistry is different, the drying mechanism is different, and the failure modes are different, which means the qualification work is different too.
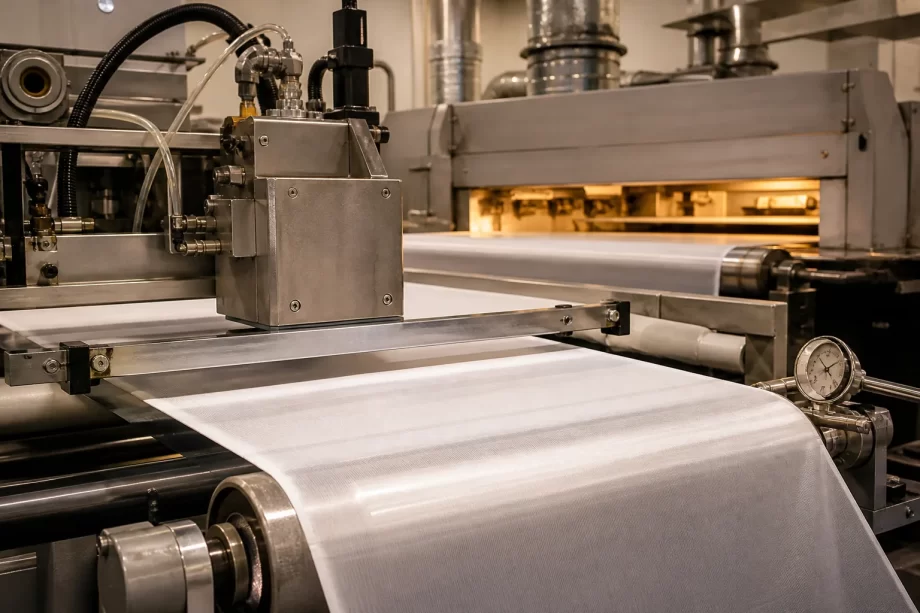
Coating head applying a thin film to nylon fabric running through a drying oven
This guide examines the claim directly. It compares water-based and solvent systems on the properties that matter in a backpack, covers the drying and energy consequences of the switch, and sets out what a factory has to change on the line before the first bulk order.
It then covers substrate preparation, ageing behaviour, appearance, defect risk, cost, regulatory drivers, and the testing regime that makes a claim defensible.
A water-based coating carries polymer dispersed in water rather than dissolved in solvent. Film formation depends on water evaporating and the polymer particles coalescing, and that mechanism explains nearly every difference that follows.
The System Table
System
Carrier
Water-based dispersion
Water
Water-based emulsion
Water and surfactant
Solvent-based
Organic solvent
Solventless
Reactive liquid
Hot melt
Thermoplastic
Powder
Dry particles
The Film Formation Table
Stage
Water-based behaviour
Application
Wet film laid down
Water evaporation
Requires energy
Particle packing
Close approach
Coalescence
Particles fuse
Film consolidation
Continuous film
Cure
Crosslink if present
The Component Table
Component
Function
Polymer dispersion
Film former
Coalescing agent
Aids fusion
Thickener
Rheology control
Wetting agent
Substrate wetting
Defoamer
Surface quality
Crosslinker
Durability
The System Comparison Table
Property
Water-based
Solvent
Solids content
Lower
Higher
Viscosity profile
Shear sensitive
More stable
Wetting on fabric
Harder
Easier
Drying demand
High
Moderate
Film build per pass
Thinner
Thicker
Adhesion on nylon
Requires primer often
Usually direct
The Claim Table
Marketing claim
What it means
Water-based
Carrier is water
Low VOC
Below a threshold
Solvent-free
No organic solvent added
Eco coating
Undefined, avoid
Non-toxic
Requires specification
Odour-free
Subjective, testable
Water-based does not mean lower performance by default, and it does not mean equivalent performance either; it means the film forms by a different route and must be validated on its own evidence.
The Performance Question, Stated Properly
The question a factory should ask is not whether water-based matches solvent, but which properties are affected, by how much, and whether the bag specification can absorb the difference.
The Property Table
Property
Practical concern
Adhesion
Coating lifting in use
Hydrostatic resistance
Water ingress
Abrasion
Surface wear
Flex fatigue
Cracking at folds
Blocking
Sticking in storage
Hand feel
Stiffness
The Bag Area Requirement Table
Bag area
Priority
Base panel
Abrasion and water
Body panel
Adhesion and flex
Roll top
Flex fatigue
Laptop sleeve
Softness
Shoulder strap
Flex and hand
Trim
Appearance
The Tolerance Table
Gap versus solvent
Verdict
Within test scatter
Acceptable
Small and consistent
Adjust specification
Large on one property
Redesign or blend
Large on several
Reconsider system
Fails minimum
Reject
Untested
Not a decision
The Test Reference Table
Test
Reference method
Adhesion
Peel or cross-hatch
Hydrostatic
Rising water column
Spray rating
Standard spray test
Abrasion
Taber or Martindale
Flex
Flex cycle test
Blocking
Stacked heat test
The Decision Table
Situation
Action
Adhesion passes, water fails
Add primer or increase build
Water passes, hand too stiff
Soften polymer or reduce coat weight
Both pass on lab
Pilot on production line
Pilot fails
Review drying and line speed
Supplier claims pass
Request their data set
No data available
Do not commit
Ask for the supplier’s test method before their result, because a performance figure quoted without a method cannot be compared with the specification the bag already has.
Adhesion and Film Formation on Nylon
Nylon is a hard substrate for water-based systems because it is smooth, low surface energy after calendering, and often carries residual spinning oils or dyeing auxiliaries that repel water.
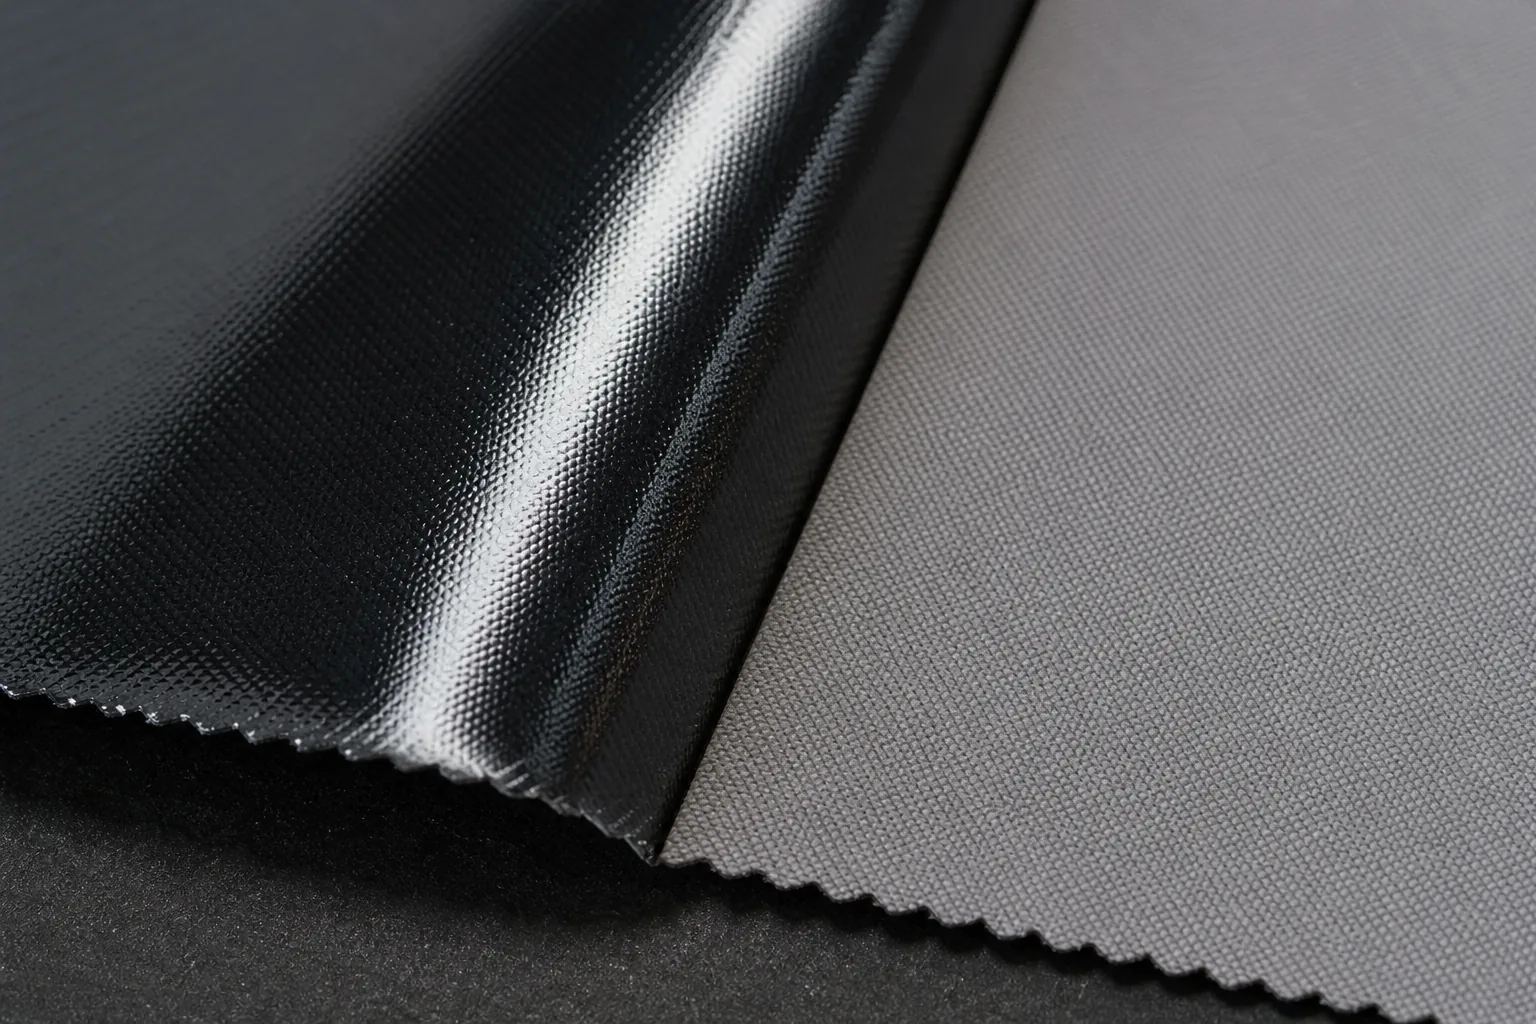
Two coated nylon swatches side by side, one glossy and one matte
The Adhesion Failure Table
Failure mode
Appearance
Interfacial release
Clean peel, no residue
Cohesive failure
Coating splits internally
Substrate failure
Fabric tears first
Edge lift
Lifting at cut edges
Blistering
Localised separation
Delamination after wash
Gradual loss
The Cause Table
Cause
Mechanism
Surface contamination
Poor wetting
Insufficient wetting
Voids at interface
Incomplete coalescence
Weak film
Over-thick film
Stress concentration
Under-cure
Low cohesion
Moisture in substrate
Blistering
The Preparation Table
Step
Purpose
Heat setting
Dimensional stability
Washing
Removes oils
Corona treatment
Raises surface energy
Primer coat
Anchoring layer
Drying
Removes moisture
Cooling control
Prevents condensation
The Process Window Table
Parameter
Sensitivity
Oven temperature
High
Line speed
High
Wet film thickness
High
Airflow
Moderate
Substrate moisture
High
Ambient humidity
Moderate
The Verification Table
Check
Method
Peel strength
Quantitative test
Cross-hatch
Qualitative rating
Wash durability
Cycles then re-test
Flex then peel
Combined ageing
Edge condition
Visual after cut
Batch consistency
Sampling plan
Adhesion failures on water-based coatings are usually process failures rather than chemistry failures, and they appear first at the cut edge, which is the cheapest place to look.
Hydrostatic Resistance and Water Repellency
Water resistance is the property buyers ask about first and the one where the two systems are most often compared unfairly, because a solvent coating can reach a given water column with a thinner film.
The Resistance Table
Measure
Meaning
Hydrostatic head
Pressure before leakage
Spray rating
Surface repellency
Bundesmann
Rain penetration
Water absorption
Uptake by mass
Seam leakage
Assembly performance
Retention after wash
Durability
The Build Table
System
Coats to reach target
Solvent high solids
One to two
Solvent standard
Two
Water-based high solids
Two to three
Water-based standard
Three to four
Water-based plus primer
Primer plus two
Foam coating
Multiple
The Influence Table
Factor
Effect on head
Film thickness
Increases
Pinholes
Destroys
Polymer type
Varies widely
Substrate roughness
Reduces
Coating uniformity
Critical
Ageing
Reduces
The Durability Table
Exposure
Effect
Flexing
Micro-cracks
Abrasion
Film thinning
Washing
Surfactant attack
UV
Polymer degradation
Heat
Softening
Cold
Embrittlement
The Testing Table
Test
Condition
Initial head
As produced
After flex
Cycled then tested
After abrasion
Worn then tested
After wash
Standard cycles
After ageing
Elevated temperature
Seam test
Assembled sample
Report hydrostatic resistance with the film weight and the number of coats, because a water column figure without build data cannot be reproduced by another factory.
Drying, Energy and Line Speed
Water has a higher latent heat of evaporation than most solvents, and the coating carries less solids per wet kilogram. Both effects push drying demand upward, and drying is where the switch most often fails in practice.
The Drying Table
Factor
Water-based effect
Latent heat
Higher per kilogram
Solids content
Lower
Water to remove
More per square metre
Oven length
Often insufficient
Airflow demand
Higher
Energy per metre
Higher
The Energy Table
Source
Share
Oven heating
Largest
Air movement
Significant
Chiller and dehumidification
Moderate
Coating line drives
Small
Extraction
Moderate
Lighting
Minimal
The Line Speed Table
Constraint
Consequence
Oven length fixed
Speed must fall
Throughput target
Second pass needed
Labour cost
Rises per metre
Energy cost
Rises per metre
Delivery schedule
Extended
Capacity
Reduced
The Retrofit Table
Measure
Purpose
Nozzle drying
Higher heat transfer
Air impingement
Faster evaporation
Zoning
Profile control
Heat recovery
Energy saving
Humidity control
Consistent drying
Tension control
Prevents distortion
The Measurement Table
Metric
Use
Energy per metre
Cost tracking
Oven temperature profile
Quality control
Residual moisture
Cure verification
Line speed
Throughput
Defect rate
Process stability
Rework rate
Cost impact
A factory that switches chemistry without measuring energy per metre is trading a visible solvent cost for an invisible drying cost, and the second one appears in the utility bill a month later.
Retrofitting the Coating Line
Most factories do not build a new line for water-based coating; they convert an existing one. The conversion is rarely just a drum swap, and the gaps show up in the first production week.
The Equipment Table
Element
Change needed
Coating head
Different rheology handling
Metering
Tighter control
Oven
Longer or more efficient
Air system
Higher flow capacity
Extraction
Less solvent duty
Cleaning
Water-based residue
The Compatibility Table
Component
Concern
Mild steel contact
Corrosion
Elastomer seals
Swelling
Pump type
Shear sensitivity
Filters
Finer rating needed
Pipework
Residue build-up
Storage tanks
Agitation needed
The Cleaning Table
Residue
Removal
Wet coating
Water rinse
Dried film
Alkaline cleaner
Crosslinked film
Difficult, avoid
Roller build-up
Scheduled clean
Filter clogging
Replace routine
Oven deposits
Periodic service
The Changeover Table
Step
Requirement
Drain and flush
Before new batch
Filter change
Prevent contamination
Viscosity check
Before run
Trial panel
First metres
Approval
Before full run
Records
Batch traceability
The Constraint Table
Constraint
Practical limit
Oven length
Caps line speed
Extraction capacity
Solvent duty mismatch
Tank agitation
Settling risk
Temperature control
Film defects
Floor space
Storage volume
Operator skill
New parameters
Before converting a line, run a single trial shift with water-based coating and measure drying, defects and throughput, because the retrofit cost is usually decided by the oven rather than by the coating head.
Appearance, Hand Feel and Buyer Perception
Water-based coatings tend to look different even when they perform acceptably, and buyers notice appearance before they read test data.
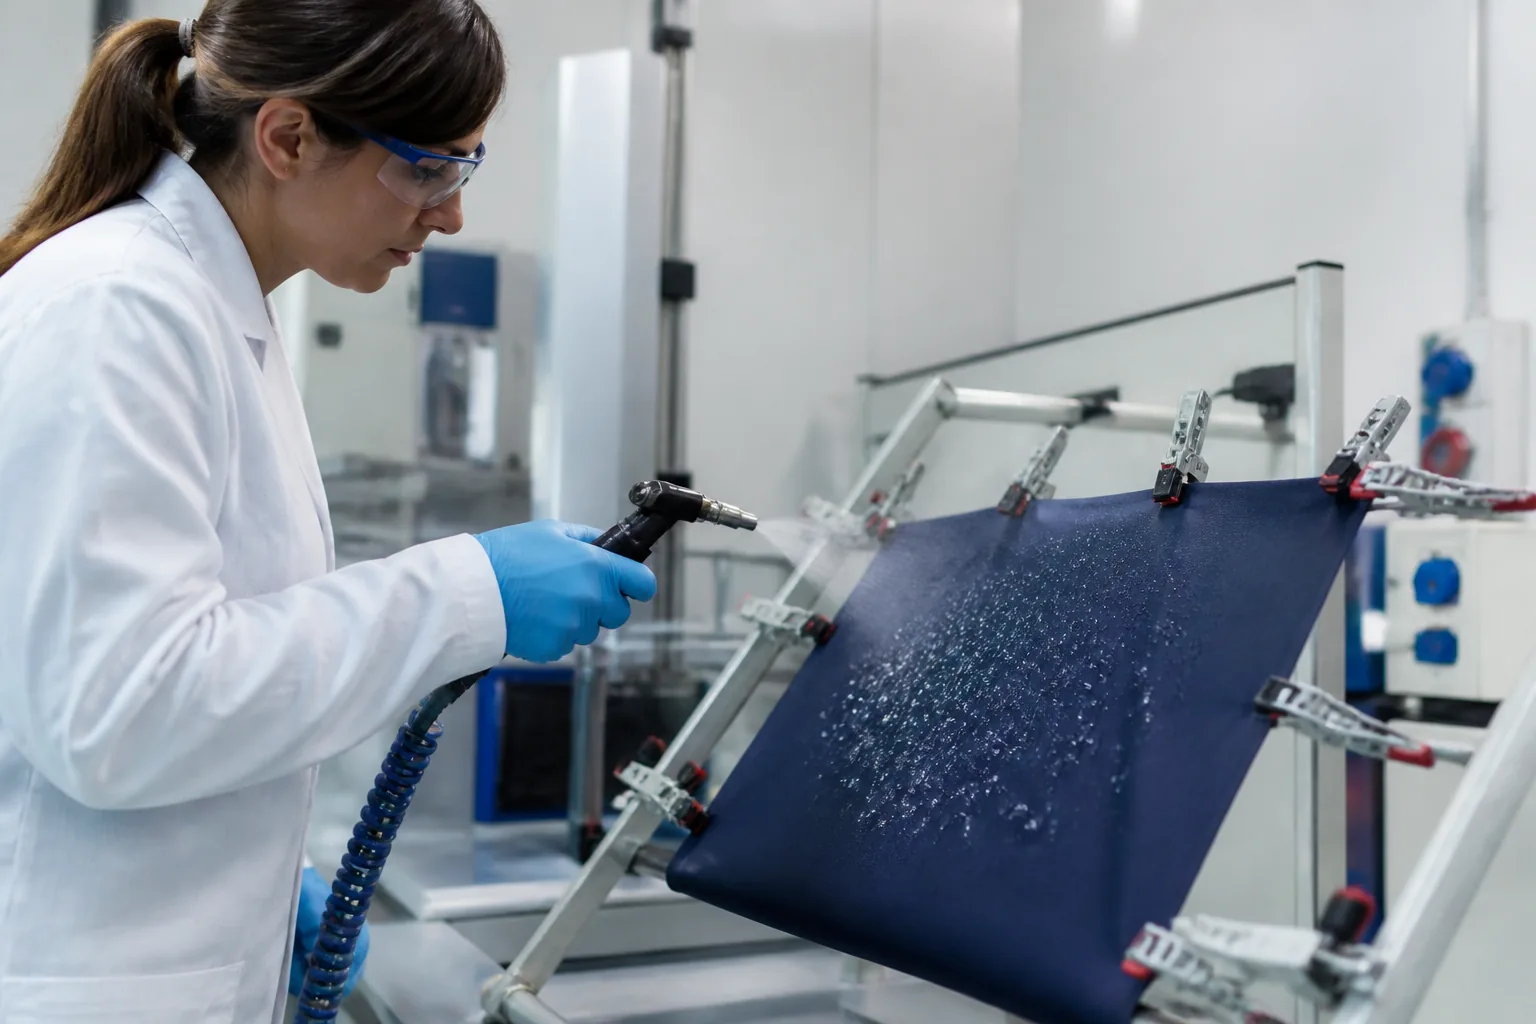
Lab technician running a water repellency spray test on coated nylon
The Appearance Table
Feature
Water-based tendency
Gloss level
Lower
Surface uniformity
Good to excellent
Colour shift
Slight
Depth of shade
Reduced
Mottling
Occasional
Edge definition
Comparable
The Hand Table
Attribute
Effect
Stiffness
Often higher
Drape
Slightly reduced
Surface touch
Drier
Warmth
Similar
Noise
Different
Recovery
Comparable
The Perception Table
Buyer reaction
Cause
Looks less premium
Lower gloss
Feels different
Higher stiffness
Colour not matching
Shade shift
Acceptable
Matched hand
Rejected
Unapproved change
Neutral
Early sample approval
The Adjustment Table
Issue
Lever
Too stiff
Reduce coat weight
Too matte
Polymer selection
Colour shift
Pigment adjustment
Mottling
Wetting agent
Surface tack
Coalescent ratio
Drape loss
Softer base fabric
The Approval Table
Stage
Deliverable
Swatch
Hand and gloss
Lab dip
Colour match
Coated panel
Full appearance
Pilot bag
In-use look
Buyer sign-off
Written
Bulk retention
Reference
Approve the hand and gloss at swatch stage rather than at first bulk, because a buyer who rejects the feel of a finished bag has already rejected the coating chemistry.
Ageing, Service Life and Failure Modes
A coating that passes on the day it is made can still fail within a season. The ageing behaviour of the two systems differs, and the difference matters most on the parts of a bag that flex.
The Ageing Table
Exposure
Water-based risk
Flex cycling
Micro-cracking
Abrasion
Film loss
Washing
Surfactant attack
Heat
Blocking and softening
Cold
Embrittlement
UV
Chalking and colour shift
The Ageing Failure Table
Mode
Where it appears
Cracking
Fold lines and roll top
Delamination
Body panel edges
Chalking
Sun-exposed surfaces
Tackiness
Storage contact points
Water ingress
Seams and base
Colour fade
Exterior panels
The Mechanism Table
Cause
Result
Incomplete coalescence
Early cracking
Excess coalescent
Long-term softening
Low crosslink density
Poor wash resistance
Film stress
Curling and lift
Plasticiser migration
Tackiness
Hydrolysis
Strength loss
The Service Table
Bag type
Dominant exposure
Commuter daypack
Flex and abrasion
Travel pack
Handling and abrasion
School bag
Abrasion and impact
Hiking pack
Flex, water, UV
Laptop sleeve
Flex and softness
Tool bag
Abrasion and oil
The Prediction Table
Test
Indicates
Flex cycles to crack
Service flex life
Abrasion to substrate
Surface life
Wash cycles to fail
Cleaning durability
Heat stack test
Storage blocking
UV hours to chalking
Exterior life
Humidity ageing
Tropical performance
Accelerated ageing does not predict a service life in years, but it reliably ranks two candidate coatings, which is what a specification decision actually needs.
Defect Risk and Yield
The switch to water-based coating changes the defect profile. New defects appear, familiar ones change frequency, and the cost lands in the cutting room where the fabric has already been bought.
The Defect Table
Defect
Cause
Pinholes
Wetting failure
Mottling
Uneven drying
Craters
Contamination
Streaks
Coating head wear
Orange peel
Viscosity mismatch
Curling
Film stress
Blocking
Residual tack
The Detection Table
Stage
Method
In-line
Visual scan
Roll end
Sampling
Cut spread
Inspection
After coating
Light box
Before sewing
Hand check
After assembly
Final audit
The Yield Table
Loss source
Effect
Coating rejects
Roll scrapped
Edge trim
Width loss
Pinhole zones
Panel exclusion
Colour variation
Shade sorting
Rework
Labour cost
Delivery delay
Penalty risk
The Control Table
Control
Purpose
Viscosity log
Stable application
Oven profile record
Consistent cure
First-metre check
Early detection
Roll retention
Dispute evidence
Defect coding
Trend analysis
Supplier feedback
Corrective loop
The Cost of Failure Table
Failure
Approximate impact
Roll rejection
Full material loss
Partial panel exclusion
Reduced yield
Rework
Labour and time
Late delivery
Contract penalty
Buyer rejection
Order loss
Field failure
Warranty cost
Most water-based coating defects are visible in the first fifty metres of a run, which makes the first-metre check the cheapest quality system available.
Cost Structure of the Switch
The commercial case is rarely a simple comparison of coating price per kilogram, because the switch moves cost between chemistry, energy, yield and throughput.
The Cost Table
Element
Direction of change
Coating material
Often higher per kilogram
Solids content
Lower, more material
Drying energy
Higher
Line speed
Lower
Labour per metre
Higher
Solvent handling
Lower
The Offset Table
Saving
Source
Solvent purchase
Removed
Solvent recovery
Removed
Extraction load
Reduced
Fire protection
Lower risk class
Permits
Simplified
Worker protection
Reduced exposure
The Investment Table
Item
Purpose
Oven upgrade
Drying capacity
Air system
Evaporation rate
Metering
Film control
Storage
Agitated tanks
Cleaning
Residue management
Training
New parameters
The Working Capital Table
Element
Effect of the switch
Coating inventory
More volume per film
Shelf life
Shorter, tighter ordering
Storage space
Pressurised by volume
Batch size
Smaller, more frequent
Line time
Longer per roll
Delivery buffer
Needs extending
The Fair Comparison Table
Basis
Fair comparison
Per kilogram coating
Misleading
Per metre coated
Better
Per finished bag
Best
Including energy
Required
Including yield
Required
Including throughput
Required
The Payback Table
Scenario
Outcome
High solvent cost
Faster payback
Tight permit regime
Faster payback
Long oven already
Faster payback
Short oven
Investment needed
Low volume
Slow payback
Premium product
Price absorbs
A switch that looks expensive per kilogram of coating can still be cheaper per finished bag, once solvent handling, permits and worker protection are counted on the same sheet.
Regulatory and Buyer Drivers
The move to water-based coating is usually triggered by regulation or by a customer commitment rather than by a performance discovery, and the trigger determines how much performance gap the programme can absorb.
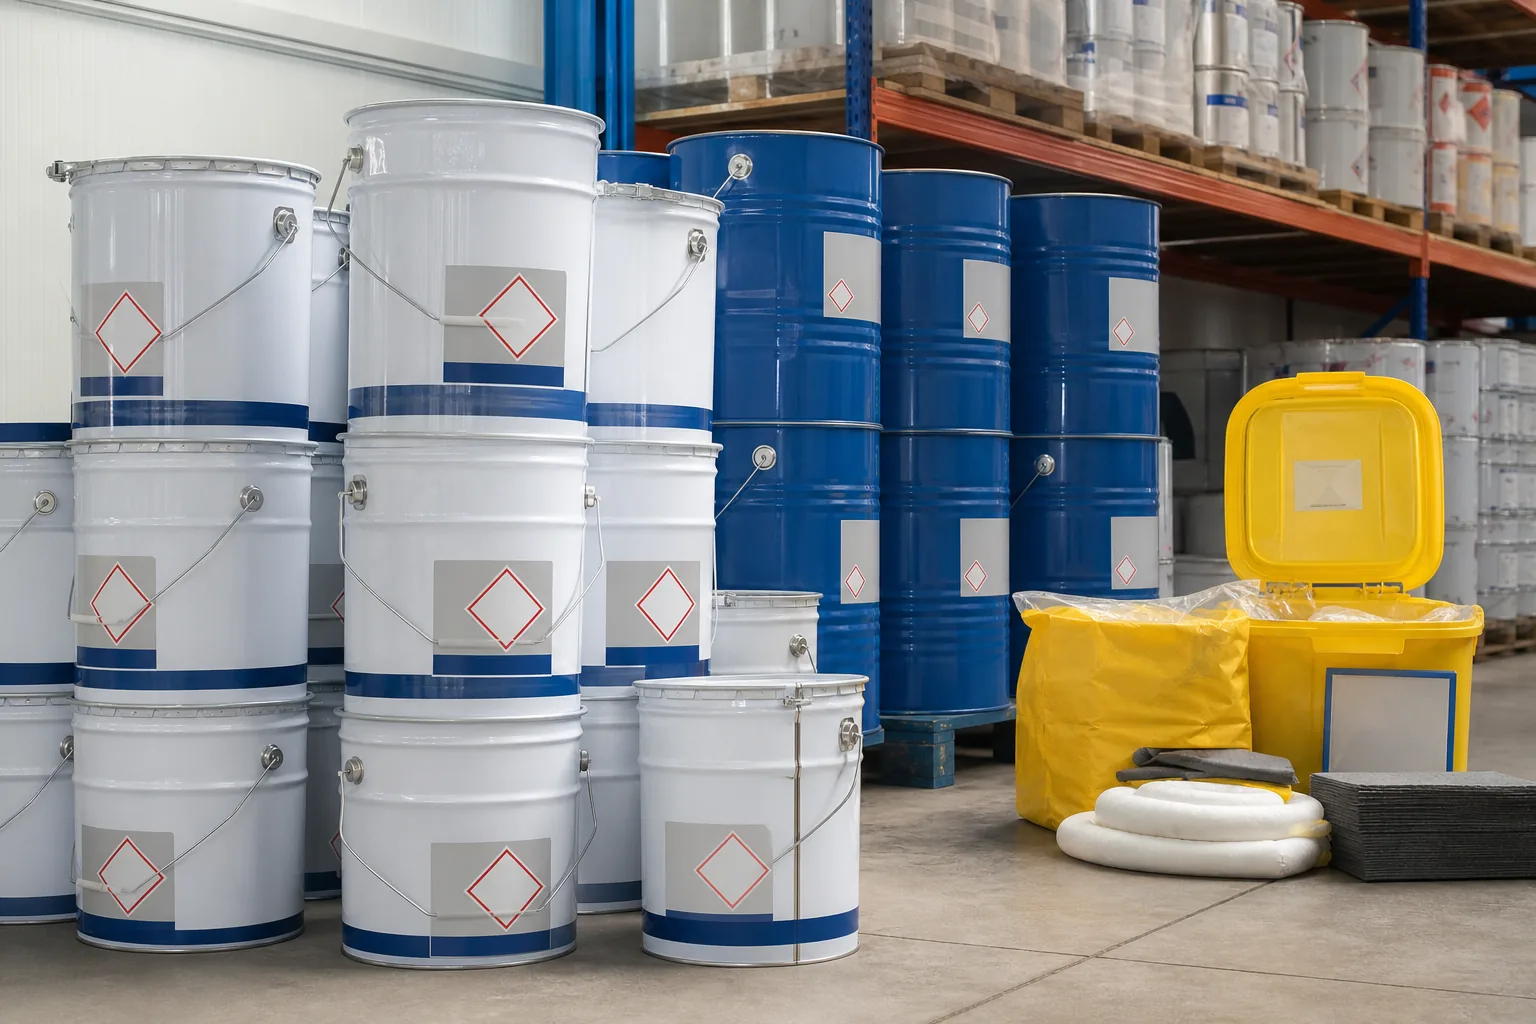
Sealed pails of water-based coating in a factory chemical store with a spill kit
The Driver Table
Driver
Typical source
VOC limits
Air quality regulation
Permit conditions
Operating licence
Worker exposure
Occupational health
Buyer chemicals policy
Brand restricted list
Retail requirement
Supplier programme
Reporting obligation
Customer disclosure
The Regulatory Requirement Table
Requirement
Evidence
VOC content
Test report
Restricted substances
Screening report
Worker exposure
Monitoring record
Substitution plan
Written programme
Performance equivalence
Test data
Disclosure
Declaration
The Documentation Table
Document
Purpose
Safety data sheet
Hazard communication
Technical data sheet
Performance specification
Test reports
Claim support
Declaration of conformity
Compliance statement
Batch certificate
Traceability
Storage guidance
Handling
The Buyer Question Table
Question
Underlying concern
Is it water-based
Chemistry change
Does it perform
Product risk
Is it verified
Reliability
What changed
Process stability
When did it change
Change control
What is next
Roadmap
The Communication Table
Audience
Message
Buyer technical
Test data
Buyer compliance
Declarations
Retailer
Programme status
Worker
Handling change
Regulator
Permit evidence
Management
Cost and risk
A chemistry change communicated after the fact reads as a substitution, and the same change communicated with test data before the order reads as an improvement.
Qualifying a Coating Supplier
Coating is the component of a bag where a supplier change is hardest to detect and most damaging to detect late. Qualification has to be deliberate.
The Qualification Table
Area
Evidence
Product data
Technical sheet
Performance
Independent test reports
Consistency
Batch records
Support
On-site technical help
Capacity
Volume commitment
Compliance
Declarations
The Trial Table
Stage
Scope
Lab application
Hand draw-down
Pilot metre
Small line run
Full roll
Production conditions
Bag making
Sewability
Field trial
Real use
Bulk
Confirmation
The Red Flag Table
Signal
Concern
No method with data
Unverifiable claim
Vague VOC figure
Compliance risk
Reluctance on trial
Confidence gap
Short shelf life undisclosed
Waste risk
No technical support
Line problems
Price far below market
Formulation risk
The Agreement Table
Clause
Purpose
Specification reference
Performance baseline
Batch consistency
Quality guarantee
Change notification
Prevents silent substitution
Test access
Verification right
Shelf life
Inventory planning
Technical support
Production continuity
The Review Table
Frequency
Activity
Per batch
Certificate and retention
Monthly
Defect trend
Quarterly
Performance re-test
Annually
Supplier review
On change
Full re-qualification
On complaint
Root cause
Ask a coating supplier for the batch record of the drum they are delivering, because consistency between drums is what separates a qualified supplier from a lucky one.
Specification and Change Control
A coating change is a product change, and the specification has to carry it as one. Factories that treat the switch as a purchasing decision discover the gap at the buyer’s inspection table.
The Specification Table
Field
Content
System type
Water-based, stated
Polymer
Class and grade
Film weight
Grams per square metre
Number of coats
Minimum
Primer
Required or not
Performance
Head, adhesion, flex
The Test Panel Table
Property
Threshold
Hydrostatic head
Minimum value
Adhesion
Rating or peel force
Spray rating
Minimum grade
Flex cycles
Before cracking
Abrasion
Cycles to substrate
Blocking
Pass or fail
The Change Table
Change
Approval
Coating supplier
Buyer and technical
Polymer class
Buyer
Film weight
Technical
Coats
Technical and buyer
Primer introduction
Buyer
Colour
Shade approval
The Record Table
Record
Retention
Specification version
Current and archive
Test reports
Batch-linked
Approval emails
Project file
Retention samples
Per style
Coating batch
Traceability
Line settings
Reference
The Notification Table
Trigger
Who is told
Formulation change
Buyer
Plant change
Buyer
Raw material source change
Buyer
Performance drift
Buyer and quality
Defect trend
Internal
Regulatory change
Compliance
Write the coating system into the specification with the same precision as the fabric, because a coating substitution is invisible in a photograph and obvious in a rain test.
Production Trials and Scale-Up
Scale-up is where laboratory results meet oven length, line speed and operator habit. The trial is not a formality; it is the only place where the two systems can be compared under the conditions that will actually apply.
The Trial Plan Table
Step
Output
Lab draw-down
Film quality
Pilot metre
Line behaviour
First roll
Full-width consistency
Bag sample
Sewability
Limited run
Yield data
Bulk
Confirmation
The Parameter Table
Setting
Trial focus
Oven profile
Cure and defects
Line speed
Throughput limit
Wet film weight
Target build
Air velocity
Evaporation rate
Tension
Distortion control
Cooling
Blocking prevention
The Data Table
Metric
Target
Metres per hour
Plan
Defect rate
Below threshold
Rework rate
Below baseline
Energy per metre
Measured
Yield
Within budget
Test results
On specification
The Sign-off Table
Party
Confirms
Production
Line capability
Quality
Test results
Technical
Specification met
Buyer
Appearance and hand
Management
Cost accepted
Compliance
Documentation
The Scale Table
Volume
Risk
Sample
Low, unrepresentative
Pilot
Moderate, informative
Limited run
Realistic
Full order
Committed
Repeat order
Proven
Multi-style
Complexity
Run the trial at the line speed intended for bulk, because a trial run slowly enough to hide a drying problem will produce a bulk order that cannot be dried.
Common Failures in Water-Based Conversion
The same failures recur across factories making the switch, and most are process failures dressed up as chemistry problems.
The Conversion Failure Table
Failure
Root cause
Adhesion loss
Contaminated substrate
Pinholes
Poor wetting
Blocking in storage
Under-cure
Cracking at folds
Over-thick film
Water head shortfall
Insufficient build
Colour mismatch
Pigment response
The Misdiagnosis Table
Symptom
Wrong conclusion
Coating peels
Chemistry unsuitable
Water fails
System cannot perform
Stiff hand
Nothing can be done
Mottling
Supplier quality
Blocking
Storage fault only
Cracking
Normal wear
The Corrective Table
Issue
First action
Adhesion
Check surface preparation
Pinholes
Review wetting and viscosity
Blocking
Verify cure and cooling
Cracking
Reduce film weight
Water head
Increase build or coats
Colour
Re-match with coated panel
The Discipline Table
Practice
Prevents
Substrate wash record
Adhesion loss
Viscosity log
Pinholes and mottle
Oven profile record
Under-cure
First-metre check
Bulk loss
Retention sample
Dispute
Change control
Silent substitution
The first question after any water-based failure should be what changed on the line, not what is wrong with the chemistry, because the chemistry rarely changes between two identical batches.
The Conversion Checklist
Chemistry
Item
Done
System selected and specified
☐
Film weight defined
☐
Primer requirement settled
☐
Performance data received
☐
Shelf life understood
☐
Storage arranged
☐
Line
Item
Done
Oven capacity verified
☐
Air system checked
☐
Metering set
☐
Cleaning procedure written
☐
Compatibility checked
☐
Trial shift run
☐
Product
Item
Done
Lab panel tested
☐
Pilot bag made
☐
Hand and gloss approved
☐
Colour approved
☐
Ageing test run
☐
Buyer sign-off received
☐
Commercial
Item
Done
Cost per bag compared
☐
Energy per metre measured
☐
Yield impact costed
☐
Throughput impact planned
☐
Change control set
☐
Review date booked
☐
FAQ
Do water-based coatings match solvent coatings on hydrostatic resistance?
They can reach the same water column, but usually with a thicker film or an additional coat, because water-based dispersions carry lower solids and build less film per pass. The practical consequence is that a specification written for one solvent coat may need two or three water-based coats to reach the same head, which changes both cost and line time. The honest comparison is per finished bag at equal performance, not per kilogram of coating. Where a bag needs a high water column at minimum weight, a solvent or reactive system may still be the more efficient route, and a hybrid approach by component is often the sensible outcome.
Why does water-based coating sometimes fail to adhere to nylon?
Usually because the substrate is not wetting properly rather than because the chemistry is unsuitable. Nylon after calendering is smooth and low in surface energy, and it often carries residual spinning oils, coning lubricants or dyeing auxiliaries that repel a water-borne film. Water-based systems are less tolerant of that contamination than solvent systems, which dissolve or displace some of it. The standard remedies are a thorough wash or heat-setting step before coating, a corona treatment to raise surface energy, and in stubborn cases a thin primer. Adhesion should be verified by a peel or cross-hatch test on the actual production substrate, not on a laboratory swatch.
Does switching to water-based coating increase energy consumption?
Frequently yes, per metre coated, even though the solvent handling burden disappears. Water has a higher latent heat of evaporation than most organic solvents, and a water-based coating delivers less solid material per wet kilogram, so more mass has to be evaporated to leave the same film. The result is higher oven demand, and where oven length is fixed, lower line speed. The net energy position depends on the existing oven efficiency: a line with modern nozzle drying and heat recovery may see a modest increase, while a line with an older oven may need capital investment before the switch is viable at all.
Will the hand and appearance change?
They usually do, and the change should be approved before bulk rather than discovered at inspection. Water-based coatings tend to sit at a lower gloss and can feel drier or slightly stiffer at equal film weight, and the depth of a dark shade can read differently because the film refracts light differently. None of these is inherently unacceptable, but they are visible to a buyer who has already approved a solvent-coated sample. The practical approach is to coat a panel of the actual fabric early, present it for hand and gloss approval at the same time as the colour approval, and keep the approved panel as the bulk reference.
Can an existing solvent coating line be converted?
In most cases yes, with the oven as the deciding constraint. The coating head, metering and pipework usually need attention because water-based products behave differently under shear and can settle in tanks without agitation, and mild steel contact points and some elastomer seals may need to be reviewed for corrosion and swelling. The oven is the harder question: if it cannot remove the additional water at the required line speed, the conversion will run slower or need additional passes, and that is an economic decision rather than a technical one. A single trial shift on the existing line, measured for defect rate and throughput, answers the question more reliably than a supplier’s datasheet.
What causes blocking in storage with water-based coatings?
Incomplete cure and residual tack, most often because the film did not reach full coalescence before the roll was wound. Water-based systems need enough heat and enough time for the polymer particles to fuse, and a line running fast or an oven running cool will produce a film that looks dry but still softens under stack pressure. Coalescing agents help fusion, but an excess leaves the film permanently plasticised and prone to sticking. The practical controls are an oven profile record per run, a cooling check before winding, and a heat stack test on the finished roll rather than on a single panel.
How should a coating change be communicated to buyers?
Before the order, with test data, and as a specification change rather than as a production note. A buyer who learns about a coating substitution at inspection will treat it as an unapproved change, whatever the performance data shows, and the commercial consequence is usually worse than the performance question. The workable package is the revised specification, comparative test results against the previous system on the same methods, an appearance sample for hand and gloss approval, and a statement of what changed in the process. Buyers with restricted substance lists will also want the screening declaration and the updated safety data sheet as part of the same submission.
Is water-based coating always the lower-impact choice?
Not automatically, and the honest answer depends on the boundary. It removes solvent emissions and reduces worker exposure, which are real and significant benefits, but it can increase energy use per metre and may require more material to reach the same performance. A life cycle comparison therefore has to include the coating mass, the drying energy and the line speed, not just the solvent content. Where the local grid is carbon-intensive and the oven is inefficient, the energy penalty can be substantial. The defensible position is to make the switch where the regulatory and exposure benefits are clear, measure the energy consequence, and avoid claiming an environmental improvement without a calculation behind it.
Conclusion
Water-based coating can match solvent performance on a backpack, but rarely by direct substitution. It matches on a specification written for it: the right film weight, the right number of coats, a properly prepared substrate, and an oven capable of removing the water at the intended line speed.
The properties that need the most attention are adhesion and water resistance. Adhesion because nylon is an unforgiving substrate for a water-borne film and contamination that a solvent would have tolerated will cause a clean peel.
Water resistance because lower solids mean more coats to reach the same head, which changes cost and throughput rather than the principle. Both are settled by testing on the production substrate rather than on a laboratory swatch.
The drying question is the one that decides whether the switch is economic. Water carries a higher evaporation load and delivers less solids, so energy per metre rises and line speed falls unless the oven is upgraded. A factory that measures energy per metre during the trial knows its position; one that compares coating prices per kilogram does not.
The commercial case is usually stronger than the chemistry case suggests, because solvent purchase, recovery, extraction load, fire risk classification and permits all move in the same direction. Those savings belong on the same sheet as the energy increase, and the comparison should be per finished bag.
For buyers, the useful questions are which system, what film weight and coat count, what the head and adhesion results were on the actual substrate, what changed in appearance, and what the energy consequence was. A supplier that answers all five has converted a line. A supplier that answers with a VOC figure has changed a purchase order.