Two hides can leave the same farm, pass through different tanneries, and become materials that behave nothing alike. One softens with age and darkens into a rich patina. The other holds color perfectly for years but cracks when it flexes. The difference is not the animal. It is the tanning method.
For a bag factory, tannage decides almost every downstream decision: how the leather cuts, how it stitches, whether edges can be burnished, how it resists water and heat, and what warranty a brand can honestly offer.
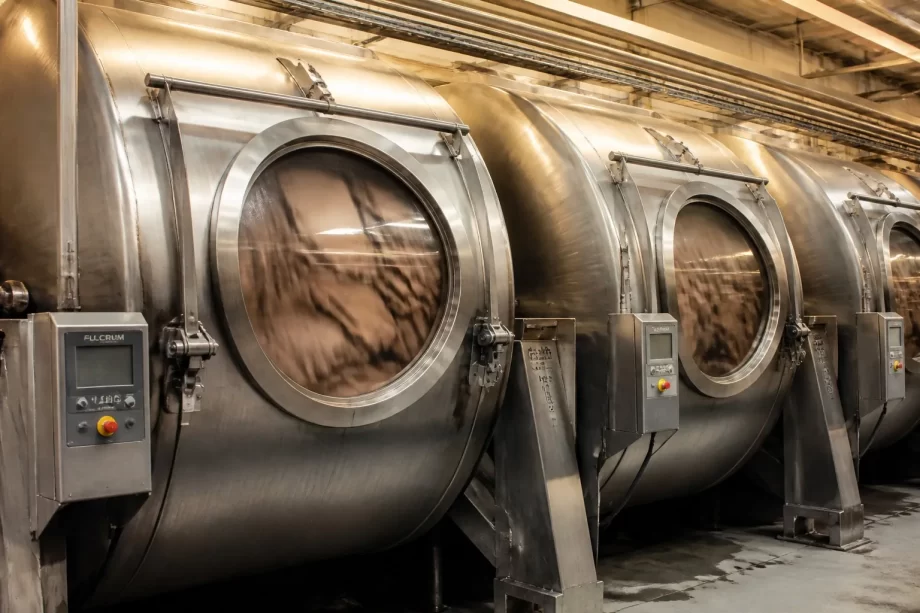
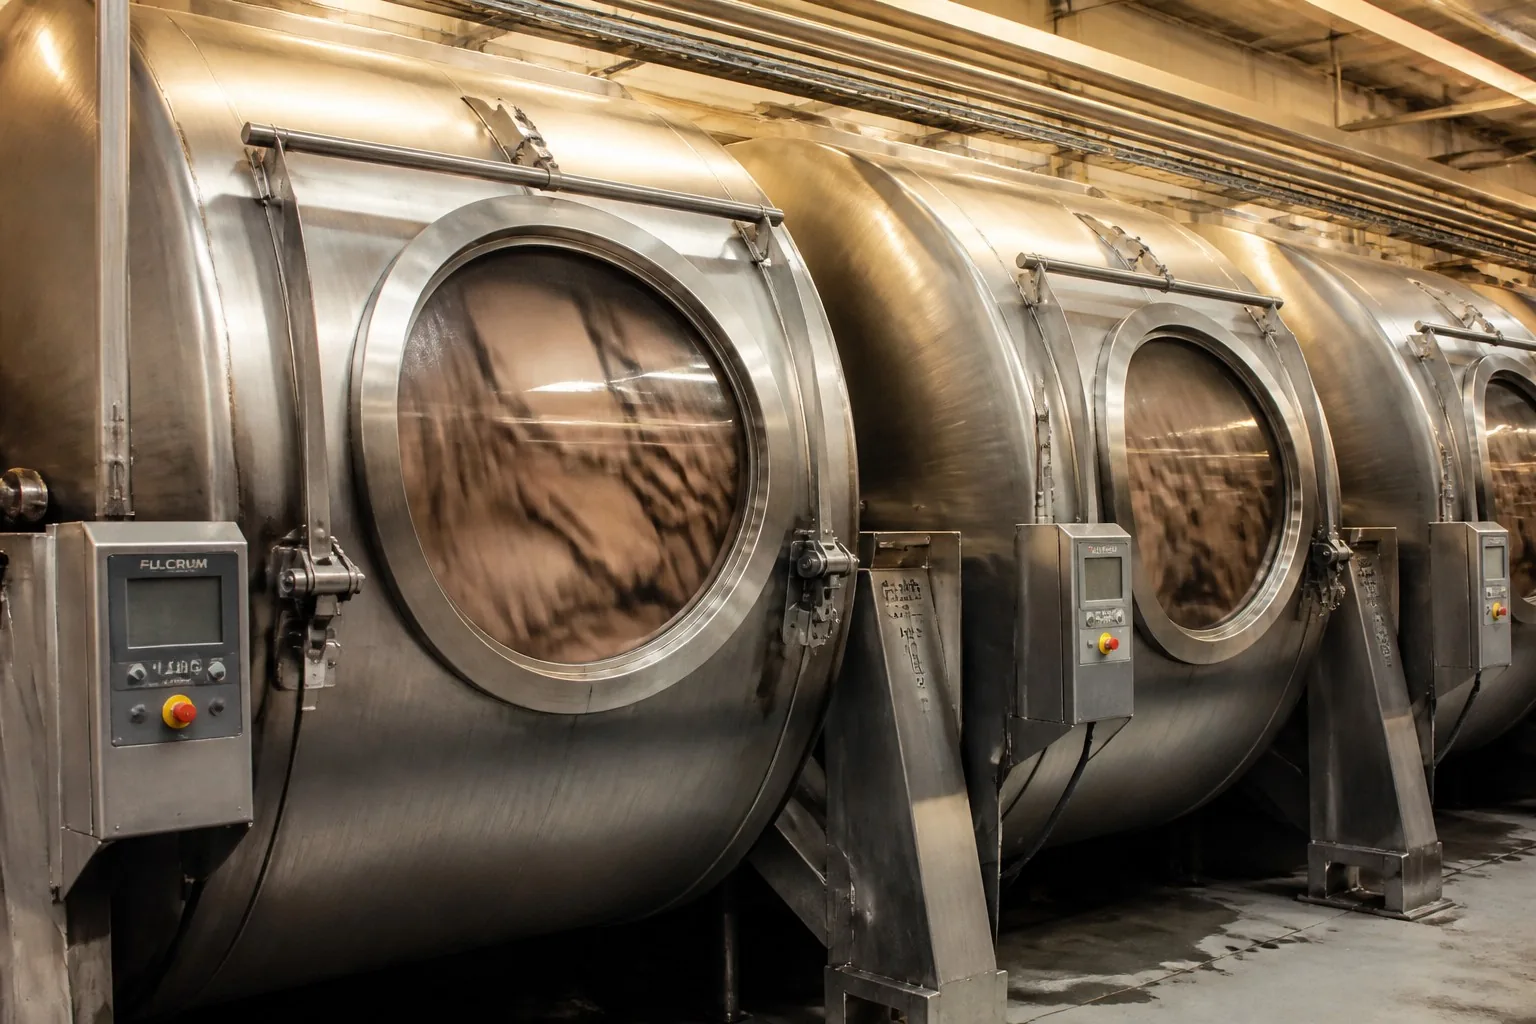
Tannery drums rotating with hides
This guide explains the tanning methods used for bag leather, what each one does to the material, and how to specify tannage so the leather you approve in sampling is the leather you receive in bulk.
Raw hide is a biological material that would rot within days. Tanning stabilizes it — but the chemistry used leaves a permanent fingerprint on the finished leather.
The Three Properties Tannage Controls
Property
Why it matters for bags
Fiber stability
Shape retention under load
Thermal resistance
Safe ironing and heat contact
Water response
Rain, humidity, spills
How Tannage Shows in the Finished Bag
Bag behavior
Tannage influence
Sagging over time
Fiber stability
Edge burnishing
Fiber openness
Color consistency
Dye uptake chemistry
Aging pattern
Tanning agent chemistry
Odor
Residual process chemicals
The Cost Line Item
Tannage is not a minor cost. It shapes the hide’s usable area, yield, and scrap rate.
Cost factor
Tannage effect
Material price per sq ft
Direct process cost
Cutting yield
Hide flexibility and size
Rework rate
Surface defects
Finishing labor
Additional treatments
Factory note: When a tannery changes its process mid-season without notice, the leather can look identical on arrival and behave completely differently on the line. Always re-approve bulk lots against a retained sample — not against memory.
Inside the Tanning Process
Tanning runs in four stages. Each stage changes the hide, and each can be varied to produce different finished leathers.
Stage 1: Beamhouse
Beamhouse work prepares the raw hide for tanning.
Step
Purpose
Soaking
Rehydrate preserved hides
Fleshing
Remove flesh and fat
Unhairing
Remove hair and epidermis
Liming
Swell fiber structure
Deliming
Neutralize lime
Bating
Soften and open fiber
Stage 2: Tanning
The tanning agent stabilizes the collagen fiber permanently.
Method
Agent
Vegetable
Plant tannins
Chrome
Chromium salts
Aldehyde
Glutaraldehyde, oxazolidine
Synthetic
Phenolic syntans
Combination
Two or more agents
Stage 3: Retanning and Dyeing
Retanning fills the fiber and adjusts the final hand.
Action
Result
Retanning
Fuller, firmer leather
Dyeing
Color throughout or surface
Fatliquoring
Softness and lubrication
Fixing
Color fastness
Stage 4: Finishing
The surface gets its final appearance and protection.
Finish step
Function
Buffing
Even surface
Coating
Protection and color
Embossing
Grain pattern
Ironing
Flatness and gloss
Measuring
Area for invoicing
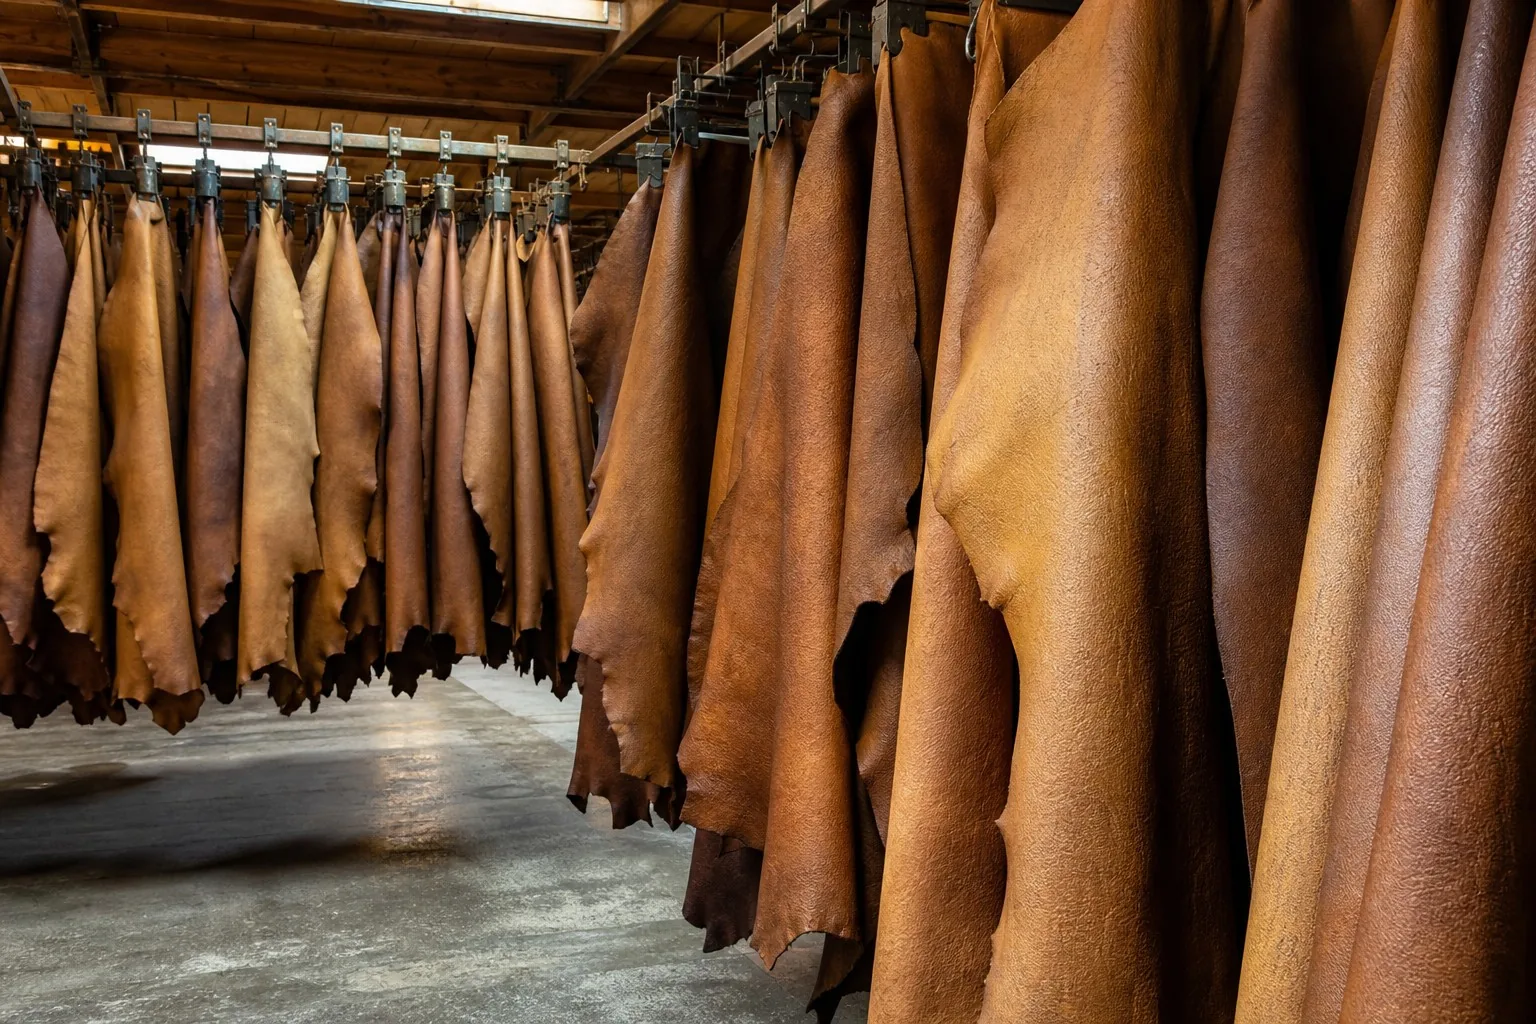
Raw hides hanging in tannery drying room
Vegetable Tanning
Vegetable tanning uses natural tannins from bark, wood, leaves, and fruit. It is the oldest method and still the reference for heritage leather goods.
How the Process Runs
Vegetable tanning is slow. Hides move through a series of pits or drums with progressively stronger tannin liquors.
Phase
Typical duration
Suspender pits
1–2 weeks
Layaway pits
6–12 weeks
Handlers
2–3 months
Final drums
Days
The Tannin Sources
Source
Character
Chestnut
Firm, warm tone
Mimosa
Fast, light color
Quebracho
Reddish, dense
Tara
Pale, soft
Oak
Traditional, slow
Why Bag Makers Choose It
Advantage
Explanation
Patina
Darkens with handling
Edge burnishing
Fibers fuse smoothly
Tooling response
Accepts carving
Repairability
Surface can be refinished
Natural appearance
No coating conceals grain
The Limitations
Limitation
Consequence
Water sensitivity
Spots easily
Heat sensitivity
Risk of scorching
Firm hand
Longer break-in
Cost
Slow process, premium price
Color range
Limited to earth tones
Factory note: Vegetable-tanned leather cannot tolerate the same ironing temperatures as chrome-tanned leather. If the tech pack specifies a high-heat operation without accounting for tannage, the finishing room will scorch the panels — and the damage only shows after polishing.
Where It Fits in Bags
Bag type
Suitability
Heritage briefcase
Excellent
Satchel and vintage styles
Excellent
Premium straps
Excellent
Structured backpack body
Good, heavy
Lining
Poor, too firm
Chrome Tanning
Chrome tanning uses chromium salts and dominates the global leather market — over 80% of leather by volume. It is fast, versatile, and produces soft, stable leather.
Why the Industry Adopted It
Advantage
Explanation
Speed
Hours instead of months
Softness
Supple hand
Thermal stability
Tolerates higher heat
Water resistance
Better than vegetable
Color range
Bright, consistent dyes
The Process Steps
Step
Function
Pickling
Acidify the hide
Chrome liquor
Penetrate fiber
Basification
Fix the chromium
Aging
Complete reaction
Retanning
Adjust hand and fullness
The Two Forms of Chrome
Form
Role
Trivalent (Cr III)
Active tanning agent
Hexavalent (Cr VI)
Regulated contaminant
The Hexavalent Question
Cr VI is the compliance issue that follows chrome-tanned leather into every market.
Aspect
Detail
Origin
Oxidation under heat, light, humidity
Regulation
Strict limits in EU and other markets
Testing
Standard extraction tests
Prevention
Proper fatliquor and pH control
Where It Fits in Bags
Bag type
Suitability
Everyday backpacks
Excellent
Travel bags
Excellent
Fashion bags
Excellent
Lining and interior
Excellent
Heritage patina styles
Poor fit
Combination and Hybrid Tanning
Most bag leather is not purely one chemistry. Combination tanning blends agents to capture the strengths of each.
The Common Combinations
Combination
Effect
Chrome + vegetable
Stability with patina
Chrome + synthetic
Softer hand, lower cost
Aldehyde + vegetable
Chrome-free with firmness
Vegetable + synthetic
Faster process, fuller body
Why Tanners Combine
Goal
Combination used
Softer feel
Chrome base + synthetic retan
Better aging
Chrome base + vegetable retan
Chrome-free label
Aldehyde + vegetable
Cost control
Reduced chrome + syntans
Color depth
Vegetable retan on chrome base
The Specification Trap
“Chrome-free” and “vegetable-tanned” are not the same claim.
Claim
Technical meaning
Chrome-free
No chromium used at any stage
Vegetable-tanned
Plant tannins are the primary agent
Combination-tanned
Two or more agents
Metal-free
No metal salts
What to Ask the Tannery
Question
Why
“What is the primary tanning agent?”
Determines behavior
“Is any chrome used in retanning?”
Label compliance
“What is the fatliquor type?”
Softness and aging
“Can you supply test reports?”
Market access
Alternative Tanning Methods
Beyond the two main routes, several methods serve specific markets and compliance needs.
Aldehyde Tanning
Property
Detail
Agent
Glutaraldehyde and related
Character
Soft, white, stable
Chrome content
None
Use
Chrome-free lines, automotive
Cost
Higher than chrome
Synthetic Tanning
Property
Detail
Agent
Phenolic syntans
Character
Light, filling
Role
Usually a retanning step
Alone
Rarely used as sole tannage
Benefit
Cost and hand control
Smoke and Brain Tanning
Method
Character
Use today
Smoke
Yellow-brown, aromatic
Craft and heritage
Brain
Very soft, weak
Traditional, niche
Fat liquoring only
Soft, perishable
Not bag-grade
The Chrome-Free Landscape
Chrome-free leather is growing because brands want the claim.
Driver
Effect on materials
Brand sustainability targets
Rising demand
Market regulation
Tighter limits
Performance gap
Narrowing but real
Cost
Still higher
Supply
Fewer qualified tanneries
Factory note: Chrome-free leather often feels different from the chrome-tanned leather in an existing sample. If a brand switches to chrome-free mid-program, the pattern, interlining, and ironing settings must be re-validated — the material’s stretch and thermal response change.
Comparing Tanning Methods
One matrix, every method, the criteria that matter in bag production.
Criterion
Vegetable
Chrome
Aldehyde
Synthetic
Process time
Weeks to months
Hours to days
Days
Hours
Softness
Firm
Soft
Soft
Medium
Water resistance
Low
High
Medium
Medium
Heat tolerance
Low
High
Medium
Medium
Patina
Strong
Slight
Slight
Slight
Color range
Earth tones
Full range
Light tones
Full range
Edge burnishing
Excellent
Limited
Limited
Poor
Chrome content
None
Present
None
None
Cost index
High
Baseline
Higher
Lower
Typical bags
Heritage
Everyday
Chrome-free lines
Retanning
The Selection Shortcut
If the priority is…
Choose
Aging and character
Vegetable
Durability and color range
Chrome
Chrome-free compliance
Aldehyde or vegetable
Cost efficiency
Chrome with synthetic retan
Craft tooling effects
Vegetable
How Tannage Affects Bag Manufacturing
Tannage is not a purchasing detail. It changes how the line works.
Cutting and Yield
Tannage
Cutting behavior
Vegetable
Firmer, holds shape, lower yield
Chrome
Softer, better yield on curves
Aldehyde
Soft, good yield
Synthetic-retanned
Variable
Stitching and Seams
Tannage
Stitching note
Vegetable
Needs hammering at seams
Chrome
Stitches cleanly
Aldehyde
Watch needle heat
Firm retans
Reduce bulk at corners
Edge Finishing
This is where tannage becomes visible to the customer.
Tannage
Edge treatment
Vegetable
Burnish and wax
Chrome
Paint or fold
Aldehyde
Paint or fold
Coated finishes
Paint only
Hardware and Reinforcement
Interaction
Consideration
Soft leather
Back reinforcement needed
Firm leather
Hard edges, skive corners
Stretch-prone areas
Avoid belly zones
Rivet points
Add reinforcement patch
Thermal Operations
Operation
Tannage sensitivity
Hot stamping
Chrome tolerates more heat
Edge painting dryers
Vegetal scorches easily
Heat-seal reinforcement
Chrome only
Ironing
Test temperature first
The Line Adjustment Checklist
When tannage changes
Re-validate
Needle and thread size
Yes
Stitch length
Yes
Presser foot pressure
Yes
Ironing temperature
Yes
Edge finishing method
Yes
Pattern allowances
Often
Choosing Tannage by Bag Type
The right tannage follows the product’s job, climate, and price position.
The Product Matrix
Bag type
Recommended tannage
Reason
Heritage briefcase
Vegetable
Patina and tooling
Everyday backpack
Chrome
Durability, color range
Travel duffel
Chrome
Water and abrasion
Fashion tote
Chrome or aldehyde
Color and softness
Minimalist leather pack
Aldehyde
Chrome-free positioning
Tool and work bags
Chrome, firm retan
Shape retention
Laptop sleeves
Chrome, soft
Flexibility
The Climate Adjustment
Climate
Prefer
Avoid
Humid tropical
Chrome
Untreated vegetable
Dry desert
Vegetable, conditioned
Over-dried chrome
Cold and wet
Chrome, treated
Aniline finishes
Four seasons
Chrome, semi-aniline
Extreme finishes
The Price Position
Tier
Typical tannage
Mass market
Chrome with synthetic retan
Mid premium
Chrome, quality retan
Premium heritage
Vegetable or hybrid
Luxury craft
Vegetable, aniline finish
Environmental and Regulatory Landscape
Tanning is one of the most regulated steps in the bag supply chain. Compliance travels with the leather.
The Environmental Issues
Issue
Source
Wastewater load
Beamhouse and tanning liquors
Chromium discharge
Chrome tanning effluent
Solid waste
Trimmings and sludge
Chemical handling
Acids, salts, biocides
Energy use
Drying and finishing
The Regulatory Framework
Framework
Scope
REACH
Chemical restrictions in EU market
LWG audit
Tannery environmental rating
ZDHC
Manufacturing restricted substances
Proposition 65
California chemical warnings
Labeling rules
Leather claims on products
The Chromium VI Limit
Cr VI is the number buyers should know.
Market
Typical restriction
EU
Strict limit on finished leather
USA
Federal and state variation
UK
Follows EU-style rules
Global brands
Internal limits often stricter
The Tannery Rating System
Rating
Meaning for buyers
LWG Gold
Audit leader
LWG Silver
Strong performer
LWG Bronze
Meets baseline
Unrated
Additional vetting needed
Finished leather hides inspected at tannery
What to Demand in Documentation
Document
Purpose
LWG certificate
Environmental assurance
Cr VI test report
Compliance proof
Restricted substances declaration
Market access
Traceability statement
Origin and chain
Batch reference
Complaint handling
Specifying Tannage in the Tech Pack
Tannage belongs in writing. Verbal descriptions produce disputes three months later.
The Spec Fields
Field
Example entry
Primary tannage
Chrome
Retanning
Synthetic and vegetable blend
Finish
Semi-aniline
Thickness
1.4 mm ±0.1
Color reference
Approved swatch
Cr VI
Below market limit, tested
Tannery rating
LWG Silver minimum
Traceability
Named tannery and lot
The Approval Workflow
Stage
Action
Material brief
Define tannage and finish
Lab dip
Color and hand approval
Sample
Full construction test
Bulk lot
Compare to retained sample
Production
In-line checks
Final
Test report review
The Documentation Package
Item
Kept by
Signed spec sheet
Buyer and factory
Retained sample
Buyer and factory
Test reports
Buyer, factory, tannery
Batch records
Tannery and factory
Inspection records
Factory QC
Testing and QC for Tanned Leather
Testing confirms the tannage does what the spec requires.
The Core Tests
Test
Purpose
Cr VI extraction
Compliance
Tensile strength
Structural capacity
Tear strength
Resistance to tearing
Flex endurance
Cracking resistance
Color fastness
Rub and light
pH
Skin contact and corrosion
Thickness
Spec compliance
The Incoming Inspection
Step
Check
1
Count and measure hides
2
Compare color to approved swatch
3
Check grain and defects
4
Measure thickness at points
5
Test edge burnishing behavior
6
Verify test reports against batch
7
Log acceptance or claim
The In-Line Checks
Stage
Check
Cutting
Defects excluded
Skiving
Thickness accuracy
Assembly
Seam behavior
Edge work
Finish adhesion
Final
Surface after handling
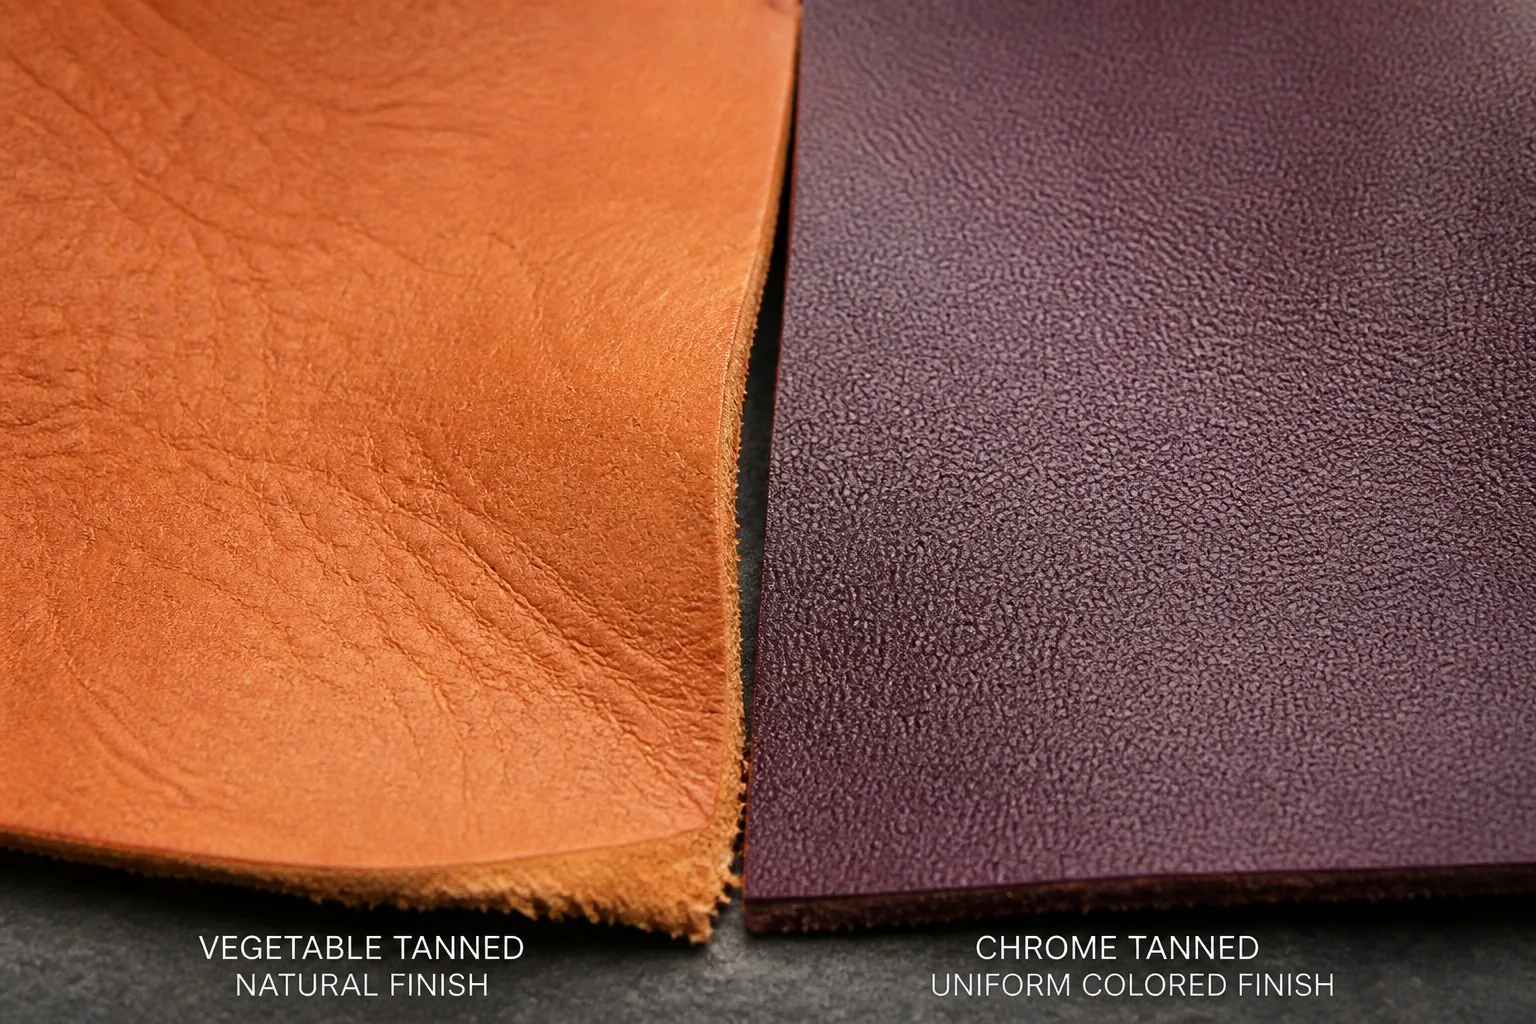
Comparing vegetable-tanned and chrome-tanned swatches
Common Problems and Root Causes
Most leather problems trace back to tannage, retanning, or finishing chemistry — not to operator skill.
The Problem Map
Symptom
Likely cause
Fading in weeks
Weak dye fixation
Cracking at folds
Insufficient fatliquor
Cr VI failure
Process control at tannery
Odor on opening
Residual chemicals
Uneven color across batch
Dye lot inconsistency
Edges won’t burnish
Chrome or coated surface
Hardening over time
Oxidation and dry fiber
Sticky finish
Wrong topcoat
The Corrective Path
Symptom
Action
Crack failures
Re-spec fatliquor and flex test
Color drift
Reserve dyed lot per season
Compliance failure
Change tannery or lot
Odor complaints
Request ventilation and re-test
Edge failures
Switch finish method
The Prevention Checklist
Practice
Benefit
Retain approved sample
Reference for disputes
Test before bulk
Early failure detection
Reserve color lots
Batch consistency
Name the tannery
Traceability
Re-validate on change
Line stability
Tannery Selection and Supplier Auditing
The tannery is a manufacturing partner, not a catalogue. Vetting it protects the whole program.
What to Verify
Area
Check
Capacity
Can it hold your seasonal volume
Rating
LWG status and audit date
Chemistry
Primary agents and retanning
Wastewater
Treatment capacity and records
Traceability
Raw hide source documentation
Consistency
Batch-to-batch variation history
The Audit Questions
Question
Red flag if…
“Which raw hide origins?”
Vague answer
“What is your Cr VI control?”
No test protocol
“May we see the wastewater plant?”
Refusal
“How do you control dye lots?”
No lot system
“Who else do you supply?”
No reference brands
The Sampling Protocol
Round
Purpose
1
Color and hand direction
2
Finish and surface match
3
Full bag sample
Bulk
Lot approval against retained sample
Factory note: Seasonal capacity is the real constraint. A tannery with excellent quality but no slot in August cannot deliver your autumn program. Confirm the production slot in writing at the same time you approve the sample.
Sourcing Tannage by Market and Certification
Different markets reward different claims. Buyers should choose tannage with the destination in mind.
The Market Priorities
Market
Buyer priority
EU
Restricted substances, traceability
North America
Durability, chromium disclosure
UK
Compliance, brand sustainability claims
Japan
Finish quality, hand feel
Australia
Outdoor performance, UV stability
Domestic China
Cost, color range, availability
The Certification Map
Certification
What it proves
LWG
Tannery environmental performance
ZDHC MRSL
Restricted substance management
OEKO-TEX
Finished material safety
REACH compliance
EU market access
Brand-specific RSL
Retailer requirement
The Claim Discipline
Claim
Requires
“Chrome-free”
Aldehyde or vegetable process
“Vegetable-tanned”
Plant tannins as primary agent
“Eco-tanned”
Defined by the brand or supplier
“Traceable”
Documented hide origin
“LWG Gold tannery”
Current certificate
Cost Modeling for Tanned Leather
Tannage changes cost in ways a unit price alone does not reveal. Model the whole picture.
The Cost Components
Component
Share
Raw hide
55–70%
Tanning process
15–25%
Finishing
10–20%
Logistics and duty
5–10%
The Tannage Cost Index
Method
Relative cost
Chrome
Baseline
Chrome with synthetic retan
Slightly lower
Aldehyde
Higher
Vegetable
Highest
Combination premium
High
The Hidden Cost Drivers
Factor
Cost effect
Lower cutting yield
Higher cost per panel
Higher reject rate
Material replacement
Extra finishing steps
Labor time
Compliance testing
Per-batch cost
Re-validation on change
Engineering time
The Total Cost View
Decision
Cheapest option
Best value option
Everyday bag body
Chrome, standard retan
Chrome, quality retan
Heritage bag body
Chrome with coating
Vegetable, aniline
Chrome-free line
Aldehyde standard
Aldehyde with verified reports
Interior panels
Split leather
Chrome, soft retan
Model the total: the cheap leather with 60% yield can cost more per finished panel than premium leather at 72% yield.
Working with the Factory on Tannage Changes
Tannage changes are the most common source of mid-season quality surprises. Handle them as engineering events, not purchasing swaps.
The Change Triggers
Trigger
Risk
Tannery raises price
Substitute material
Capacity shortage
Alternative tannery
Color unavailable
Similar shade
Compliance update
New chemistry
Cost reduction target
Lower grade
The Change Protocol
Step
Action
1
Document the proposed change
2
Request new samples
3
Re-test mechanical properties
4
Re-validate line settings
5
Approve revised spec sheet
6
Retain new reference sample
The Line Re-validation Items
Item
Why it changes
Needle and thread
Fiber firmness differs
Stitch density
Seam behavior differs
Ironing temperature
Thermal tolerance differs
Edge finishing
Burnishing response differs
Skiving depth
Thickness varies
Pattern allowance
Stretch varies
The Communication Rules
Rule
Effect
Written approval before change
No silent substitutions
Named tannery in the PO
Traceability
Batch reference on labels
Fast complaint handling
Retained samples per season
Dispute resolution
The Buyer’s Tanning Checklist
A single page that prevents most leather disputes.
Before Ordering
Check
Done
Primary tannage named
☐
Retanning described
☐
Finish defined
☐
Thickness and tolerance
☐
Tannery named and rated
☐
Test reports requested
☐
Color lot policy agreed
☐
Retained sample stored
☐
At Bulk Approval
Check
Done
Color within tolerance
☐
Grain and surface match
☐
Thickness measured
☐
Hand and drape compared
☐
Edge behavior confirmed
☐
Cr VI report reviewed
☐
At Production
Check
Done
Defect grading recorded
☐
Yield tracked
☐
In-line checks followed
☐
Non-conformities escalated
☐
Final inspection signed
☐
The Five Questions That Matter
Which tannery, and what is its rating?
What is the primary tanning agent and the retanning?
What is the Cr VI status of this batch?
Can we see the retained sample from approval?
What changes if we switch tannage next season?
Aging, Care and Warranty by Tannage
Tannage sets the aging curve. Brands should match care instructions and warranty terms to the chemistry they bought.
The Aging Patterns
Tannage
1 year
3 years
5 years
Vegetable
Darkens, softens
Rich patina
Characterful
Chrome, semi-aniline
Even wear
Gentle change
Stable
Chrome, pigmented
Minimal change
Coating wear begins
Touch-ups needed
Aldehyde
Slight softening
Stable
Stable
The Care Instructions by Tannage
Tannage
Recommended care
Vegetable
Condition twice yearly, avoid rain
Chrome semi-aniline
Occasional cream, damp wipe
Chrome pigmented
Damp cloth, mild soap
Aldehyde
Protect spray, gentle clean
The Warranty Mapping
Tannage
Reasonable warranty scope
Vegetable
Structural, with care exclusions
Chrome
Structural and finish
Aldehyde
Structural
Coated finishes
Limited due to coating wear
The Customer Communication
Message
Why it helps
“Leather changes with use”
Sets expectations
Care card by material
Fewer misuse claims
Patina as a feature
Turns change into value
Repair service notes
Longer product life
Factory note: Most warranty disputes are expectation disputes. A customer who was told the leather would darken does not complain when it darkens. A customer who was told it would stay flawless does. Print the care card for the tannage you actually used.
Lead Times and Seasonal Planning by Tannage
Tannage changes the calendar as well as the material. Plan backwards from the ship date.
The Lead Time Components
Stage
Chrome
Vegetable
Sampling
1–2 weeks
3–4 weeks
Tannery production
2–4 weeks
8–16 weeks
Finishing and drying
1 week
2–3 weeks
Transport
2–6 weeks
2–6 weeks
The Seasonal Reality
Season
Planning note
Spring program
Order leather before December
Autumn program
Order leather before May
Peak tannery months
Book slots early
Holiday orders
Add two weeks buffer
The Buffer Rules
Risk
Buffer
Color approval delay
2 weeks
Tannery capacity slip
3 weeks
Transport congestion
2 weeks
Compliance retest
1 week
Factory note: Vegetable-tanned programs need to be locked roughly a quarter earlier than chrome programs. Brands that discover this after the sample stage lose the season — not the order, but the sell-through window.
Tanning Terms Buyers Should Know
The vocabulary of tanning appears in tannery quotes and spec sheets. Buyers who read it precisely avoid expensive assumptions.
The Core Vocabulary
Term
Meaning
Beamhouse
Preparation stage before tanning
Bating
Enzyme softening of fiber
Pickling
Acidification before chrome tanning
Basification
Raising pH to fix chromium
Retanning
Secondary treatment after main tannage
Fatliquoring
Oil emulsion for softness
Syntan
Synthetic tanning agent
Crust
Tanned but unfinished leather
Finishing
Surface treatment stage
Substance
Leather thickness in mm
The Commercial Vocabulary
Term
Meaning
Sq ft
Common area unit for leather
Hide size
Average area per hide
Selection
Grade based on usable area
Lot
Production batch reference
RSL
Restricted substances list
Lab dip
Small color sample
The Terms That Cause Disputes
Phrase
Risk
“Same as last time”
No documented reference
“Premium tannage”
Undefined quality
“Eco leather”
Undefined chemistry
“Export quality”
Undefined standard
“Standard thickness”
No tolerance stated
FAQ
What is the difference between vegetable-tanned and chrome-tanned leather?
Vegetable tanning uses plant tannins over weeks or months and produces firm leather that develops a patina, burnishes beautifully, and stays sensitive to water and heat. Chrome tanning uses chromium salts in hours or days and produces softer, more water-resistant, more heat-stable leather with a wider color range. Most everyday bag leather is chrome-tanned or a combination.
Is chrome-tanned leather dangerous or banned?
Trivalent chromium is the active tanning agent and is not banned. The regulated concern is hexavalent chromium (Cr VI), which can form during processing or storage under heat and humidity. Markets such as the EU set strict limits on Cr VI in finished leather. Buyers should require test reports for every batch rather than avoiding chrome altogether.
Which tannage should I choose for a backpack that will be used daily?
Chrome-tanned leather with a quality retanning is the practical choice for daily backpacks: it resists water, handles color consistently, tolerates heat operations, and cuts efficiently. Reserve vegetable-tanned leather for heritage styles where patina and tooling effects are the selling points.
What does “combination tanned” mean?
Combination tanning uses two or more agents, most commonly a chrome base followed by vegetable or synthetic retanning. The chrome provides stability and water resistance, while the retanning adjusts hand, fullness, color depth, and aging behavior. Many premium bag leathers are combination tanned.
Can I specify chrome-free leather for my bag line?
Yes. Aldehyde tanning and vegetable tanning are the main chrome-free routes. Expect differences in softness, thermal tolerance, color range, and cost, and note that fewer tanneries offer qualified chrome-free production. Re-validate patterns, ironing temperatures, and edge finishing when switching to a chrome-free material.
How do I verify that the bulk leather matches the approved sample?
Compare the bulk lot against a retained sample on color, grain, thickness at multiple points, hand, and edge burnishing behavior, and check test reports against the batch reference. A 5 mm thick swatch and a signed spec sheet stored by both parties settle most disputes quickly.
Why does vegetable-tanned leather cost more?
The process takes weeks to months in pits and drums rather than hours, occupies far more tannery capacity, uses more expensive tanning agents, and produces lower yield from the same hide. The price reflects process time and capacity, not marketing.
Does tannage affect environmental compliance of the finished bag?
Yes. Tannery wastewater, chromium management, and chemical restrictions all sit upstream of your product, so tannery ratings and test reports are effectively part of your compliance file. Brands selling into the EU should expect to provide evidence of the tannery used and the restricted substances status of each leather lot.
Conclusion
Tanning is the step that turns a perishable hide into a material a customer can carry for a decade. Vegetable tanning delivers character, burnishing, and patina at the cost of water sensitivity and process time. Chrome tanning delivers softness, stability, and color range at the cost of compliance discipline. Aldehyde and synthetic routes fill specific needs, and most bag leather is a deliberate combination.
For production teams, the working rules are simple. Name the tannery, the primary tanning agent, the retanning, and the finish in writing. Keep a retained sample and signed spec sheet. Test Cr VI, tensile, and flex before bulk. Re-validate the line whenever tannage changes. Then match the promise — water resistance, aging, warranty — to the chemistry you actually bought.
Get tannage right, and the leather you approve in sampling is the leather your customers will still be carrying years later.