Leather Types for Bags: Full-Grain to Bonded Explained
Leather Types for Bags: Full-Grain to Bonded Explained
“Leather bag” tells a buyer almost nothing. The word covers materials that last thirty years and materials that peel apart in one season — sold under the same label, at prices that look comparable on a spec sheet.
For a bag factory, leather type drives everything downstream: the pattern engineering, the machines on the line, the cutting yield, the stitching method, the QC standard, and the warranty the brand can honestly offer.
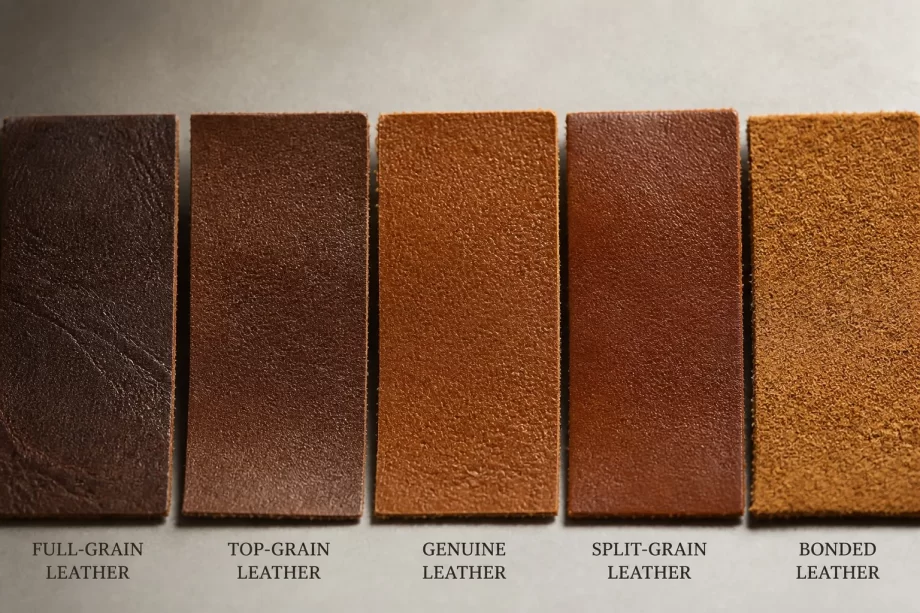
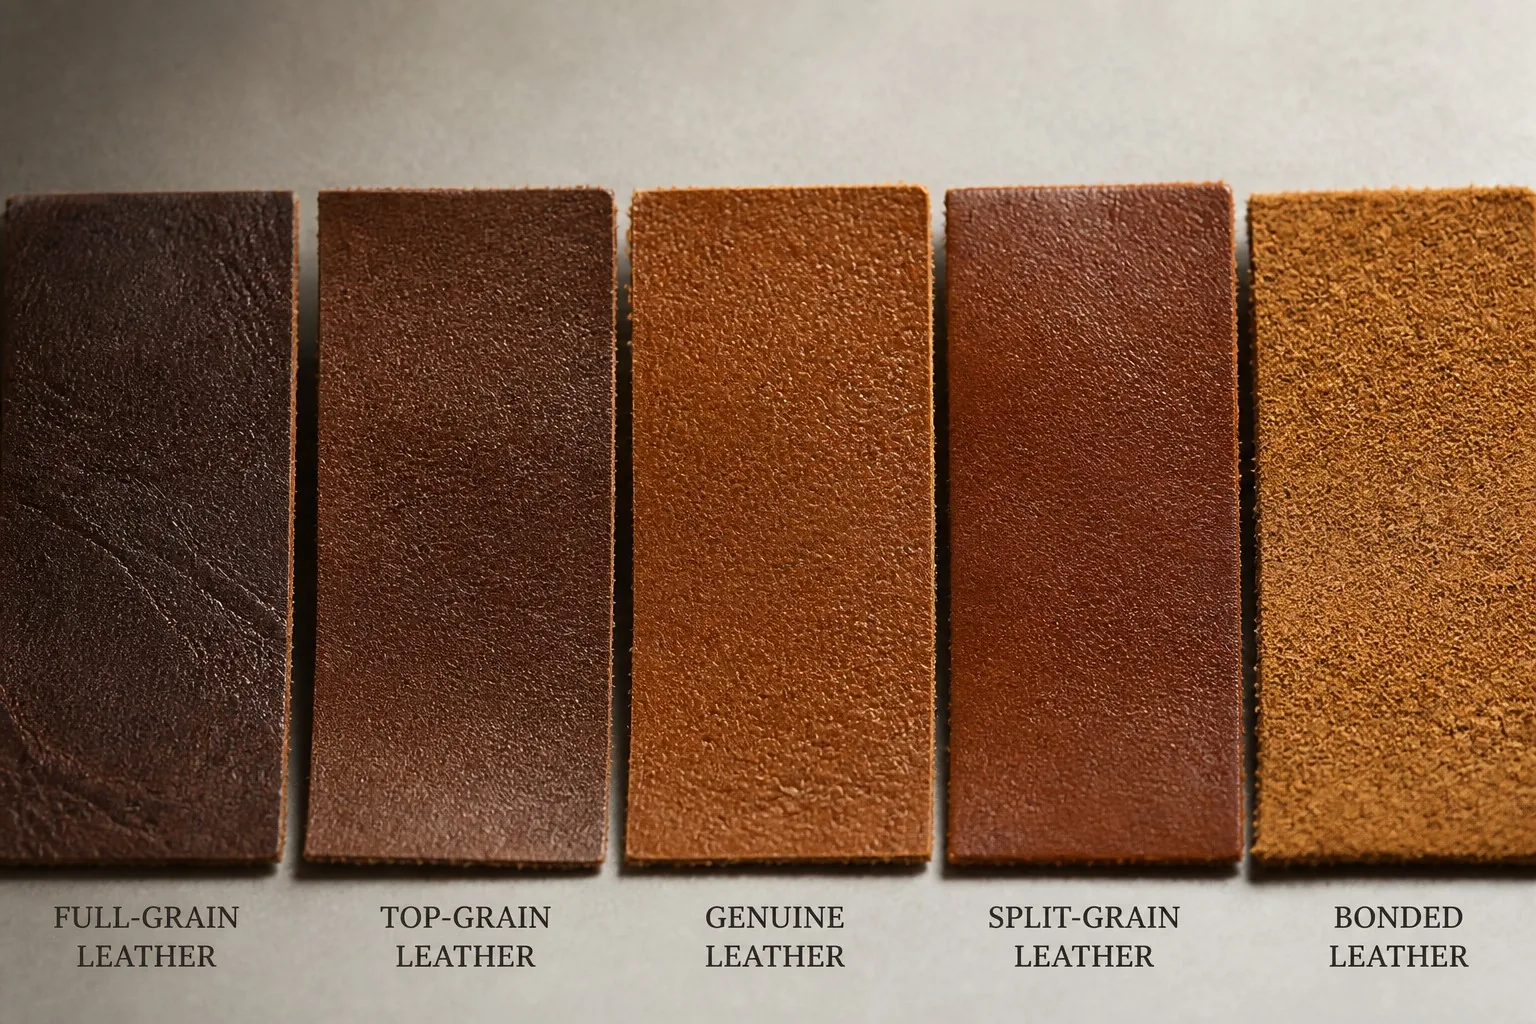
Leather hide samples showing different grades
This guide walks through the leather grades used in bag manufacturing — from full-grain to bonded — with the specs, costs, and selection logic a production team actually needs.
Leather is not one material. It is a family of materials with radically different structures.
The Cost Spread
The same apparent bag can carry a leather cost that differs by a factor of six.
Leather type
Relative material cost
Full-grain
6×
Top-grain
4×
Corrected-grain
2.5×
Split leather
1.5×
Bonded leather
1×
The Durability Spread
Cost tracks structure, and structure tracks how the material ages.
Type
Expected service life
Full-grain
10–30 years
Top-grain
5–15 years
Corrected-grain
3–8 years
Split
2–5 years
Bonded
1–3 years
The Manufacturing Consequences
Each grade behaves differently on the factory floor.
Grade
Cutting
Stitching
Edge work
Full-grain
Careful layout
Walk foot+
Burnish or paint
Top-grain
Standard
Standard
Paint
Corrected
Standard
Standard
Paint
Split
High yield
Light foot
Fold or paint
Bonded
Very high yield
Delicate
Fold only
Factory note: The single most expensive mistake in bag development is approving a sample made from full-grain and then mass-producing from corrected-grain. They look similar on a photo. They do not feel, age, or wear the same.
The Leather Grading System Explained
Grades come from how the hide is split and finished, not from animal quality alone.
The Hide Structure
A cowhide is thick. Tanners split it horizontally into layers.
Layer
Position
Character
Grain
Top surface
Dense fiber, pores
Corium
Middle
Strong but no grain
Flesh
Bottom
Loose, fibrous
Where Each Grade Comes From
Grade
Layer used
Grain surface
Full-grain
Top only
Original, intact
Top-grain
Top, light sanding
Slightly corrected
Corrected-grain
Top, sanded + embossed
Replaced
Split
Corium
None
Bonded
Fiber scraps
Artificial
The Terminology Trap
Marketing language does not match grading language.
Marketing word
Technical reality
“Genuine leather”
Often split or corrected
“Real leather”
Any layer
“Premium leather”
Undefined
“Italian leather”
Origin, not grade
“Full-grain”
Actual grade — verifiable
Full-Grain Leather
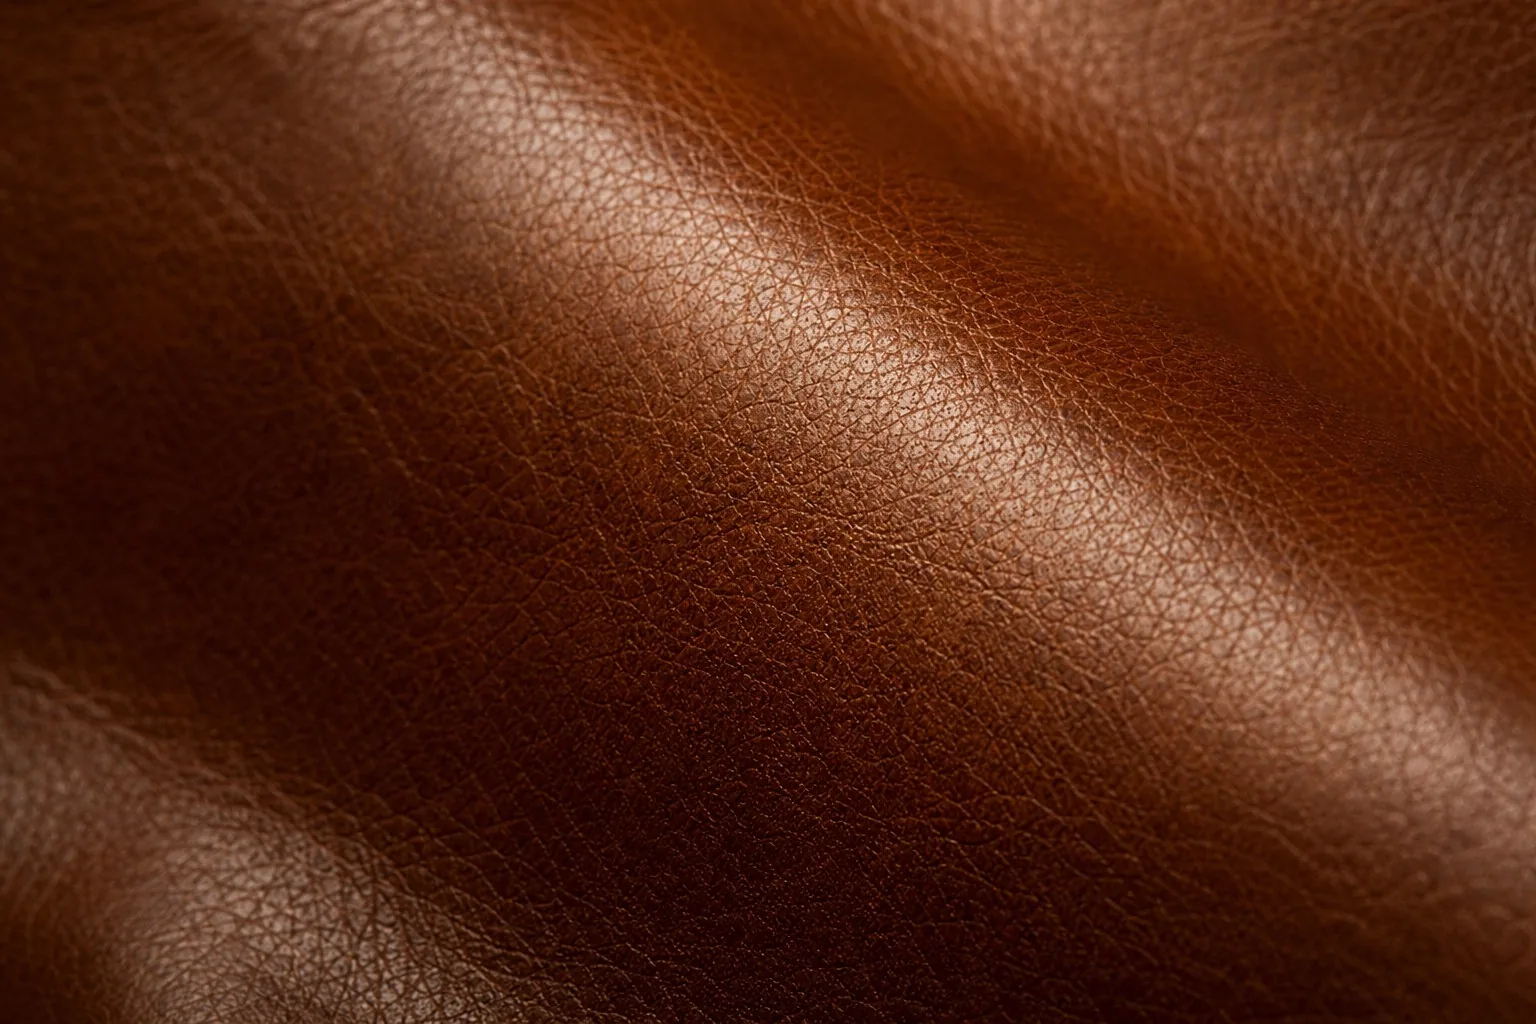
Full-grain is the top layer with its grain surface untouched. It is the reference standard all other leathers are compared against.
Macro detail of full-grain leather surface
What Makes It Full-Grain
The defining characteristic is absence of processing on the grain.
Property
Detail
Grain
Original, intact
Sanding
None
Embossing
None
Fiber density
Highest
Pore visibility
Natural and clear
Why It Ages Well
Full-grain develops a patina rather than degrading. Oils from handling migrate into the fiber and darken the surface, building depth that no finish can imitate.
Aging behavior
Detail
First 6 months
Surface darkens evenly
1–3 years
Color depth builds
Scratches
Buff out with friction
Cracks
Rare, only with neglect
Long-term look
Richer than new
Where It Belongs in a Bag
Application
Suitability
Premium backpack body
Excellent
Flap and trim
Excellent
Straps and handles
Excellent
Lining
Too heavy, wasteful
Internal pockets
Overkill
The Selection Criteria
Criterion
Reason
Hide area above 4.5 m²
Fewer seams
Consistent grain
Matching panels
Tight fiber
Edge burnishing works
Natural markings
Accepted as character
Vegetable tannage option
Better aging
The Full-Grain Trade-offs
Advantage
Disadvantage
Best durability
Highest cost
Best aging
Visible natural marks
Repairable
Thicker, heavier
Premium perception
Less uniform color
Top-Grain Leather
Top-grain is the top layer, lightly sanded to remove surface imperfections, then finished. It keeps the strong fiber structure while gaining uniformity.
The Processing Steps
Step
Purpose
Splitting
Remove lower layers
Light sanding
Remove marks and scars
Buffing
Even surface
Finish coat
Color and protection
Embossing (optional)
Grain pattern
Where It Sits in the Market
Top-grain is the mainstream premium choice: strong enough for daily use, uniform enough for mass production.
Market tier
Typical use
Mid-premium
Main body leather
Premium
Contrast panels
Mass premium
Full bag construction
Corporate gifting
Uniform color batches
The Specs That Matter
Spec
Typical range
Thickness
1.2–1.6 mm
Finish
Pigmented or semi-aniline
Tensile strength
High
Color consistency
Good
Grain pattern
Embossed or natural
When Top-Grain Beats Full-Grain
Scenario
Better choice
Large uniform order
Top-grain
Brand wants no visible scars
Top-grain
Price-sensitive premium
Top-grain
Heritage, patina-focused brand
Full-grain
Corrected-Grain Leather
Corrected-grain is also top layer leather, but heavily sanded and embossed. The grain surface is removed and replaced with an imitation pattern.
The Correction Process
Stage
Action
1
Split the hide
2
Heavy sanding of grain
3
Fill and buff
4
Emboss pattern
5
Pigment coat
6
Top protective layer
The Uniformity Advantage
Because the surface is manufactured, corrected-grain is extremely consistent — the same grain pattern, the same color, batch after batch.
Property
Result
Surface uniformity
Very high
Color consistency
Very high
Wasted hide area
Low
Scrap rate
Low
Cost per panel
Moderate
The Durability Limit
The protective coating wears before the fiber does. Once coating breaches occur, the material degrades quickly.
Failure mode
Cause
Coating peel
Adhesion failure
Cracking
Flex fatigue
Scuffing to base
Abrasion
Color loss
UV and friction
Where Corrected-Grain Works
Application
Verdict
Fashion-forward seasonal bags
Good fit
Cost-controlled premium lines
Good fit
Heavy daily-use backpacks
Acceptable
Heirloom positioning
Wrong material
Factory note: Corrected-grain hides have almost no visible natural defects, so cutting yield is high — often 8–12% better than full-grain on the same pattern. That yield gain is part of why the cost is lower, and part of why the material is thinner in character.
Split Leather
Split leather comes from the lower layers of the hide — the corium and flesh sides — after the grain layer is removed. It has no natural grain surface at all.
The Structure Reality
Property
Detail
Origin layer
Corium or lower
Grain surface
None
Fiber structure
Looser than top layer
Typical thickness
1.0–1.4 mm
Surface
Coated or embossed
Why Factories Use It
Split leather is inexpensive, cuts efficiently, and accepts coatings well.
Advantage
Reason
Low cost
By-product of top-layer splitting
High yield
Few natural defects
Uniform thickness
Machine-split precisely
Coating adhesion
Open fiber structure
The Weak Points
Weakness
Consequence
No grain structure
Lower tear strength
Loose fibers
Stretches under load
Coating dependence
Peeling risk
Fast wear
Visible aging
Common Applications
Application
Fit
Suede and nubuck finishes
Excellent
Internal pocket panels
Good
Bag base reinforcement
Acceptable
Main body of a premium bag
Wrong choice
The Suede Routing
Split leather with a napped surface becomes suede — a legitimate, desirable material with its own spec language.
Suede type
Surface
Full suede
Buffed flesh side
Nubuck
Buffed grain side (top layer)
Split suede
Buffed corium
Bonded suede
Fiber reconstituted
Bonded Leather
Bonded leather is not a hide layer at all. It is reconstituted from leather fiber scraps, mixed with binder, and rolled or pressed into sheets.
How It Is Made
Step
Process
1
Collect leather shavings and scrap
2
Shred into fine fiber
3
Mix with latex or PU binder
4
Spread onto a backing
5
Calender or press flat
6
Emboss grain pattern
7
Apply surface finish
The Composition Question
Component
Typical share
Leather fiber
50–90% (often declared)
Binder
10–40%
Backing textile
Variable
Surface coating
Thin layer
The Performance Reality
Property
Typical performance
Tensile strength
Low
Tear resistance
Low
Aging
Cracks and peels
Moisture response
Poor
Repairability
None
Uniformity
Very high
Where It Appears
Product
Why used
Budget fashion bags
Lowest material cost
Promotional items
Uniform appearance
Book covers and packaging
Flat sheet format
Trim on mixed bags
Cost reduction
Factory note: Bonded leather cannot be burnished, cannot be skived cleanly, and cannot be re-stitched after failure. If a design calls for folded edges and heat-burnished finishes, bonded leather is structurally incapable — the line will produce rejects no matter how skilled the operators are.
The Legal Context
Several jurisdictions regulate the word “leather” in product labeling. A bonded material with 50% fiber content is legally distinguishable from hide leather in the EU and increasingly in North America.
Market
Position
EU
Labeling rules apply
USA
State-level variation
UK
Consumer protection rules
Global e-commerce
Frequently ignored
The “Genuine Leather” Confusion
“Genuine leather” is the most misread phrase in the industry. It is a marketing term, not a grade.
What It Legally Means
Interpretation
Reality
Popular reading
Highest quality
Technical reading
Contains real leather
Industry reading
Usually split or corrected
Buyer assumption
Often wrong
The Grade Ladder as Consumers See It
Consumer belief
Actual grade position
Full-grain
True top grade
Top-grain
Strong second
Genuine leather
Mid-to-low
Bonded leather
Lowest
How to Verify What You Are Buying
Verification
Method
Request grade in writing
Purchase order clause
Ask for tannery name
Traceability
Inspect the reverse
Fiber structure visible
Test edge behavior
Full-grain burnishes
Check thickness
Measured with caliper
Request test reports
Tensile and tear data
The Specification Language That Works
Vague terms produce disputes. Use precise terms in every tech pack.
Avoid
Use instead
“Genuine leather”
“Full-grain, 1.4 mm, veg-tanned”
“Premium leather”
“Top-grain, pigmented finish”
“Real leather”
“Split leather, suede finish”
“Leather trim”
“Corrected-grain, 1.2 mm”
The Full Comparison Matrix
One table, every grade, every decision criterion.
Criterion
Full-grain
Top-grain
Corrected
Split
Bonded
Layer
Top
Top, sanded
Top, embossed
Lower
Scrap
Grain
Natural
Lightly corrected
Artificial
None
Artificial
Durability
Highest
High
Medium
Low
Lowest
Aging
Patina
Gentle
Coating wear
Fast wear
Cracking
Cost
Highest
High
Medium
Low
Lowest
Yield
Lowest
Medium
High
High
Highest
Weight
Heaviest
Heavy
Medium
Light
Light
Repairable
Yes
Partly
No
No
No
Burnish edge
Yes
Limited
No
No
No
Best use
Heritage bags
Premium daily
Fashion lines
Linings, suede
Budget items
The Decision Shortcut
If the priority is…
Choose
Longevity and resale value
Full-grain
Premium at scale
Top-grain
Visual consistency
Corrected-grain
Tactile softness
Split suede
Lowest possible cost
Bonded
Leather Finishes Explained
Grade is the structure; finish is the surface. Two bags can share a grade and behave completely differently because of finishing.
The Three Finish Families
Finish
Surface
Protection
Patina
Aniline
Dyed, no pigment
Low
Strong
Semi-aniline
Light pigment
Medium
Moderate
Pigmented
Full coating
High
Minimal
Aniline Finishing
Property
Detail
Appearance
Natural, translucent
Marks
Visible
Water resistance
Poor
Care needs
High
Best for
Heritage and luxury
Semi-Aniline Finishing
Property
Detail
Appearance
Even color, grain visible
Marks
Mostly hidden
Water resistance
Moderate
Care needs
Moderate
Best for
Premium everyday bags
Pigmented Finishing
Property
Detail
Appearance
Uniform, opaque color
Marks
Hidden
Water resistance
Good
Care needs
Low
Best for
High-volume premium
The Finish Comparison
Factor
Aniline
Semi-aniline
Pigmented
Color uniformity
Low
Medium
High
Grain visibility
Full
Partial
Low
Scuff resistance
Low
Medium
High
Repair ease
Medium
Medium
Low
Cost
High
Medium
Lower
Tannage and Its Effect on Bag Leather
Tannage turns raw hide into stable leather. The method changes how the material behaves for decades.
The Two Main Routes
Route
Chemistry
Time
Vegetable
Plant tannins
Weeks
Chrome
Chromium salts
Hours
The Comparison
Factor
Vegetable
Chrome
Feel
Firm, dry
Soft, supple
Aging
Rich patina
Slower change
Water resistance
Lower
Higher
Heat stability
Medium
High
Environmental profile
Lower impact
Managed waste
Cost
Higher
Lower
The Hybrid Route
Many bag leathers use a combination: chrome for stability, vegetable re-tannage for feel and aging.
Hybrid trait
Benefit
Chrome base
Dimensional stability
Vegetable top
Patina development
Controlled finish
Consistent color
Broad applicability
Suits most bags
Where Bag Leather Comes From
Origin affects hide quality, price, and lead time. Buyers should know the sourcing map.
The Main Origins
Origin
Reputation
Italy
Premium finishing, high price
Spain
Strong vegetable tannage
Germany
Consistency, automotive-grade
Brazil
Volume, good value
India
Wide range, competitive cost
China
Volume, improving quality
Turkey
Mid-market strength
What Origin Actually Determines
Factor
Origin influence
Raw hide quality
Climate and husbandry
Tannery technology
Investment level
Finishing standards
Market served
Price
Labor + regulation
Lead time
Distance and logistics
The Substitution Risk
Origin claims are easy to make and hard to verify. Protect the spec with documentation.
Claim
Verification
“Italian leather”
Tannery invoices
“Vegetable tanned”
Test reports
“Gold-rated tannery”
LWG certificate
“Full-grain”
Caliper and reverse check
Thickness and Grading Specifications
Thickness is measured, declared, and enforced. Small variations change the whole bag.
The Standard Ranges
Application
Thickness
Bag body
1.4–1.8 mm
Flaps
1.2–1.6 mm
Straps
1.8–2.4 mm
Trim and piping
1.0–1.2 mm
Linings
0.6–0.9 mm
Small goods
1.0–1.4 mm
Why Tolerance Matters
Deviation
Consequence
Thicker than spec
Machines struggle, bulky seams
Thinner than spec
Weak structure, sagging
Uneven within hide
Visible panel mismatch
Inconsistent batches
Colour and hand change
The Measurement Protocol
Step
Method
Sample points
5 per hide minimum
Tool
Caliper with 10 mm foot
Method
Skive-free zones only
Record
Per-hide log
Tolerance
±0.1 mm typical
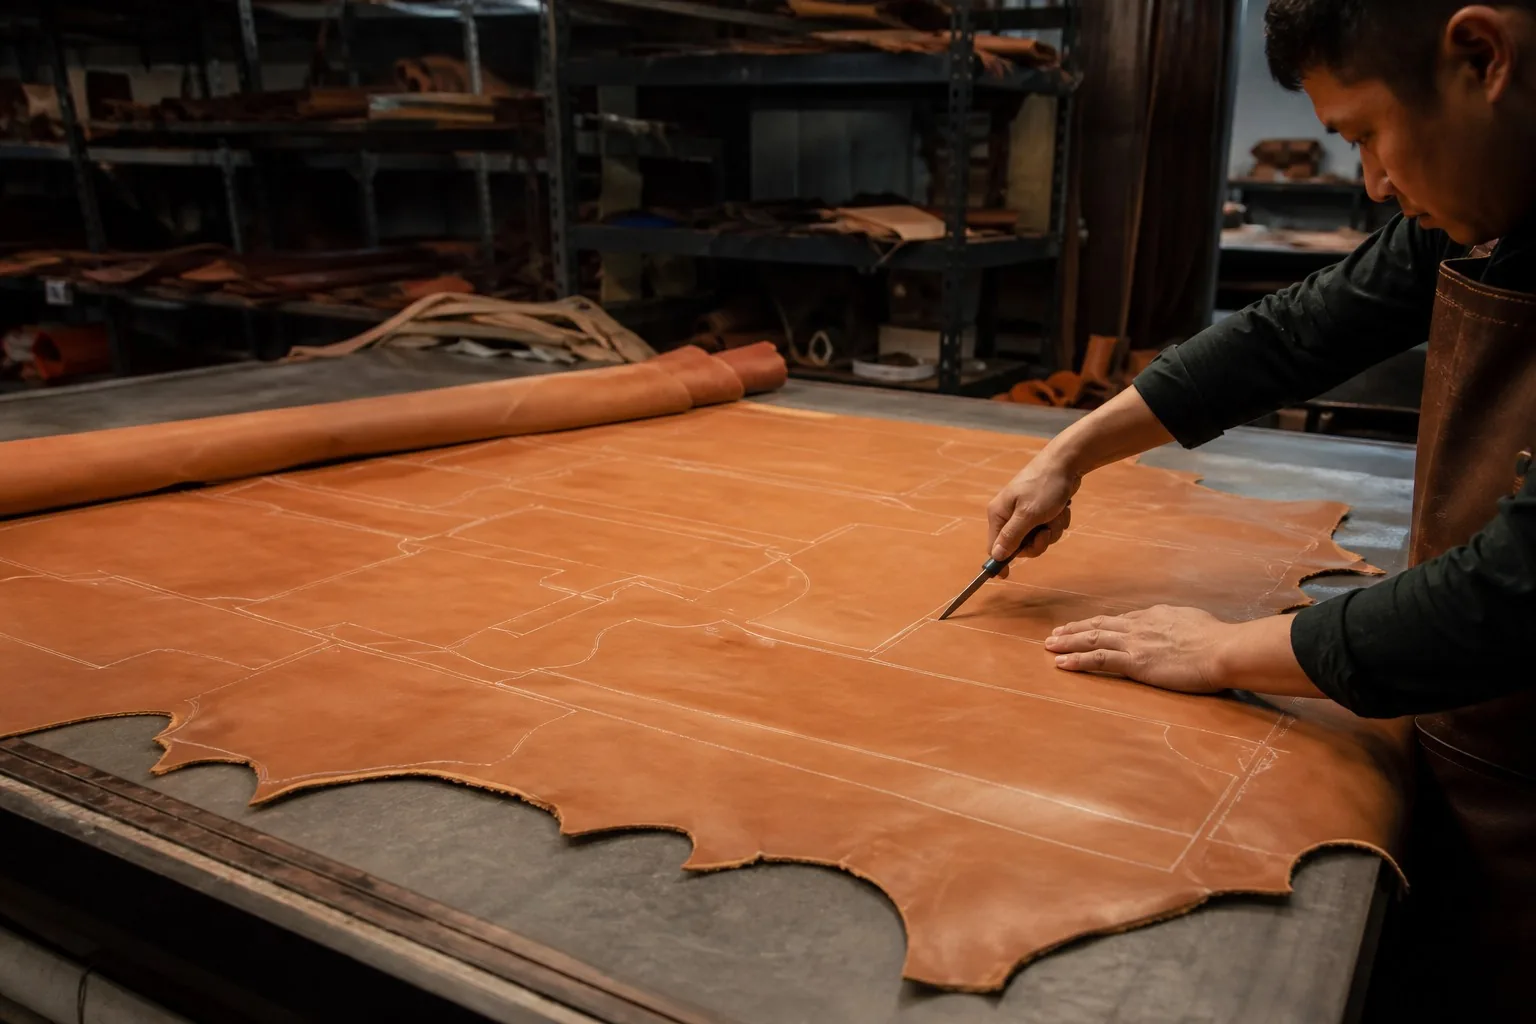
Leather cutting table with pattern pieces
Leather Cutting and Yield in Bag Production
Leather cutting is fundamentally harder than fabric cutting. Hides are irregular and no two are alike.
Why Leather Yield Is Low
Factor
Effect
Irregular hide shape
Edge waste
Natural defects
Excluded zones
Grain direction
Limits rotation
Stretch direction
Structural constraint
Size variation
Per-hide layout needed
The Typical Yield Ranges
Material
Yield range
Full-grain hides
55–70%
Top-grain hides
60–75%
Corrected-grain hides
70–82%
Split leather
75–85%
Bonded sheets
85–95%
The Cutting Rules for Leather
Rule
Reason
Nest by hand for premium
Hide-specific layout
Check stretch direction
Panels must align
Avoid belly for straps
Stretches under load
Use back for main panels
Tightest fiber
Mark defects first
Exclude before nesting
The Yield-Cost Relationship
A 10% yield difference on leather is a direct margin difference.
Scenario
Material cost effect
55% yield full-grain
Highest cost per panel
70% yield full-grain
21% lower per panel
80% yield corrected
Far lower again
Leather Inspection and QC Checklist
Leather must be inspected before cutting. Defects found after cutting are already paid for.
The Defect Catalogue
Defect
Nature
Scars and scratches
Surface damage
Insect bites
Grain disruption
Growth marks
Structural weakness
Veins
Loose fiber zones
Grain breaks
Surface cracking
Colour variation
Dye inconsistency
Thickness variation
Split tolerance
Holes
Unusable zones
The Inspection Procedure
Step
Check
1
Count hides against delivery
2
Measure thickness at points
3
Inspect grain under light
4
Mark defect zones
5
Check colour across batch
6
Grade and record
7
Accept, claim or reject
The Grading Scale
Grade
Usable area
Action
A
Above 85%
Accept
B
70–85%
Accept, note
C
55–70%
Claim, partial use
D
Below 55%
Reject
The QC Points in Production
Stage
Check
Cutting
Defect exclusion verified
Skiving
Thickness consistency
Edge finishing
Burnish or paint quality
Assembly
Colour matching panels
Final
Surface defects after handling
Cost Structure and Quotation
Leather cost is quoted in square feet in most markets, or square meters in others. Convert carefully.
The Unit Conversion
Unit
Equivalent
1 square foot
0.0929 m²
1 m²
10.764 sq ft
Hide average
18–25 sq ft
Large hide
25–32 sq ft
The Cost Components
Component
Share of leather cost
Raw hide
55–70%
Tannage
15–25%
Finishing
10–20%
Transport and duty
5–10%
The Quotation Questions
Question
Purpose
“What grade exactly?”
Structure clarity
“Which tannery?”
Traceability
“What is the thickness range?”
Spec control
“What is the defect allowance?”
Yield planning
“What is the price per sq ft?”
Cost comparison
“What is the minimum order?”
Volume planning
The Hidden Cost Traps
Trap
Consequence
Quoted per hide, not per area
Variable real cost
No thickness tolerance stated
Inconsistent panels
Defect allowance unspecified
Yield surprise
Colour lot not reserved
Batch mismatch
Grade substituted
Quality drop
Matching Leather to Bag Types
The right grade depends on the bag’s job, not only its price point.
The Matching Table
Bag type
Recommended leather
Heritage briefcase
Full-grain, veg-tanned
Premium backpack
Top-grain, semi-aniline
Fashion tote
Corrected-grain
Travel duffel
Top-grain, pigmented
Laptop sleeve
Corrected or split
Promotional bag
Bonded or split
The Weight Consideration
Leather
Effect on bag weight
Full-grain 1.8 mm
Heaviest
Top-grain 1.4 mm
Heavy
Corrected 1.2 mm
Moderate
Split 1.0 mm
Light
Bonded 0.8 mm
Lightest
The Climate Consideration
Climate
Prefer
Humid
Chrome-tanned, pigmented
Dry
Vegetable-tanned, aniline
Cold
Semi-aniline, treated
Mixed
Top-grain, semi-aniline
Care, Warranty and Honest Claims
Leather grade determines what a brand can honestly promise. Overpromising costs more than the material.
The Warranty Logic
Grade
Reasonable warranty
Full-grain
Multi-year structural
Top-grain
2–5 years
Corrected
1–2 years
Split
1 year
Bonded
Limited or none
The Care Instructions by Finish
Finish
Care guidance
Aniline
Condition regularly, avoid water
Semi-aniline
Wipe clean, occasional cream
Pigmented
Damp cloth, mild soap
Suede
Brush, protect spray
The Claims to Avoid
Claim
Risk
“Waterproof leather”
Rarely true
“Scratch-proof”
Impossible
“Will never crack”
Depends on care
“Full-grain” on corrected
Regulatory risk
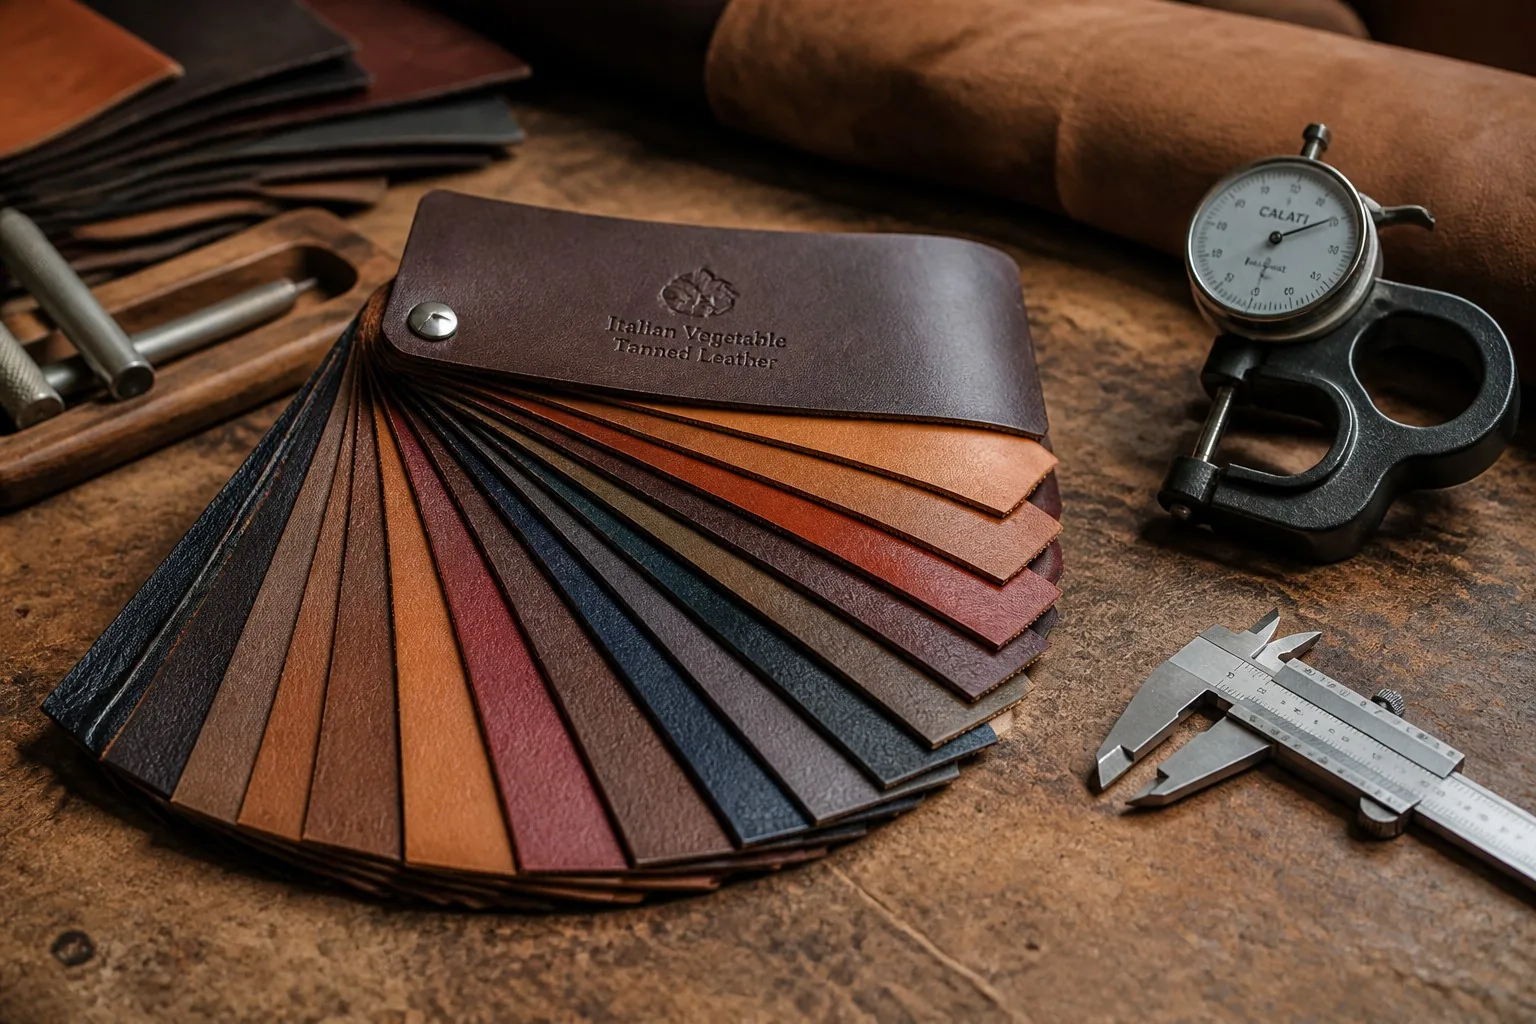
Leather swatch book with thickness gauge
Sustainable Leather and Emerging Options
Environmental requirements now reach the leather supply chain. Bags carry the claims on the label.
The Certification Landscape
Certification
Covers
LWG (Leather Working Group)
Tannery environmental performance
OEKO-TEX
Restricted substances
GOTS
Organic fiber (textiles)
Vegan labels
No animal content
REACH
Chemical compliance
The Tannery Rating System
LWG audits tanneries on a medal scale. The rating travels with the leather.
Rating
Meaning
Gold
Highest audit score
Silver
Strong performance
Bronze
Meeting baseline
The Alternative Materials
Material
Positioning
Mushroom-based
Emerging, premium niche
Pineapple leaf
Lightweight, fashion
Apple waste
Design-forward
Grape waste
Limited volume
Recycled PU
Cost-effective alternative
The Honest Comparison
Factor
Animal leather
Bio-based alternatives
Durability
Very high
Improving
Aging
Patina
Variable
Cost
Wide range
Often high
Scale
Large
Limited
Consumer perception
Polarizing
Improving
Factory note: Requests for bio-based materials usually arrive with a durability expectation built from leather experience. Test any alternative on the actual bag construction — skiving, edge finishing, and adhesion behave very differently from hide leather.
Working with Tanners: Development Timeline
Leather development runs on its own clock. Planning the calendar avoids late-season panic.
The Typical Timeline
Stage
Duration
Brief and grade selection
1 week
Tannery sampling
3–4 weeks
Sample approval
1–2 weeks
Colour matching
2–3 weeks
Bulk tannage
4–6 weeks
Shipping
2–6 weeks
The Colour Approval Process
Step
Output
Pantone reference
Target color
Lab dip
Small sample
Resin and finish trial
Surface match
Batch approval
Production lot
The Risk Points
Risk
Mitigation
Colour drift between lots
Reserve dyed lot
Hide size variation
Order by area, not hides
Late tannery capacity
Book slots in advance
Transport delays
Add buffer weeks
Grade substitution
Written spec and inspection
The Leather Spec Sheet Template
A complete leather spec prevents disputes. Every purchase order should carry these fields.
The Required Fields
Field
Example
Grade
Full-grain
Origin and tannery
Italy, named tannery
Tannage
Vegetable, hybrid
Thickness
1.4 mm ±0.1
Finish
Semi-aniline
Colour reference
Pantone or approved swatch
Defect allowance
Grade B maximum
Hide size
20–25 sq ft average
Testing
Tensile, tear, colourfast
Certification
LWG Silver minimum
The Inspection Clauses
Clause
Purpose
Sampling plan
Defined inspection level
Defect grading
A/B/C/D scale
Claim window
Days after receipt
Replacement terms
Credit or replacement
Retention sample
Dispute reference
The Approval Gate
Gate
Who signs
Sample approval
Design and production
Bulk lot approval
QC and production
Colour approval
Brand and QC
Final inspection
QC before shipment
Common Buyer Mistakes in Leather Sourcing
Most leather problems trace to five recurring mistakes. All are preventable at the spec stage.
The Mistake List
Mistake
Consequence
Specifying “genuine leather”
Unpredictable grade
No thickness tolerance
Inconsistent panels
Approving sample only
Bulk differs
Ignoring yield in costing
Margin erosion
No retention sample
Unwinnable disputes
The Prevention Table
Mistake
Fix
Vague grade wording
Technical grade in writing
Missing tolerance
±0.1 mm stated
Sample-bulk gap
Same lot, same grade
Unrealistic yield
Plan 55–70% for full-grain
No reference sample
Signed and stored
The Leather Grade Decision List
Question
If yes
Is the bag a long-term premium product?
Full-grain
Does the brand need batch consistency?
Top-grain
Is visual uniformity the priority?
Corrected-grain
Is softness more important than strength?
Split or suede
Is cost the only constraint?
Bonded with clear labeling
Run this list before sampling, not after. Changing grade after tooling and sample approval restarts the whole development cycle.
FAQ
What is the difference between full-grain and top-grain leather?
Full-grain keeps the original grain surface untouched, so the natural pores and markings stay visible and the material ages into a patina. Top-grain is the same top layer but lightly sanded and finished to remove imperfections, giving more uniform color at slightly lower durability. Full-grain ages better; top-grain produces more consistent batches.
Is genuine leather the same as full-grain leather?
No. “Genuine leather” is a marketing term that legally means the material contains real leather — it usually refers to split or corrected-grain leather, not the top grade. Full-grain is a specific technical grade and can be verified by grain visibility, thickness, and edge behavior.
Is bonded leather real leather?
Bonded leather is reconstituted from leather fiber scraps mixed with a binder and applied to a backing. It contains leather fiber but is not a hide layer, so it cannot be burnished, skived cleanly, or repaired. It is the lowest grade and behaves more like a coated material than leather.
How can I verify the leather grade my factory is using?
Put the grade in writing on the purchase order with thickness tolerance and tannery name. Inspect the reverse side to confirm the fiber structure, measure thickness with a caliper at multiple points, test edge burnishing, and request test reports for tensile and tear strength. Sample and bulk must come from the same approved lot.
What thickness leather should I specify for a backpack?
Most backpack bodies run 1.4–1.8 mm, flaps 1.2–1.6 mm, and straps 1.8–2.4 mm for load-bearing strength. Trim and piping use 1.0–1.2 mm. Always state a tolerance — usually ±0.1 mm — and measure at several points per hide during inspection.
Why is leather cutting yield so much lower than fabric yield?
Hides are irregular in shape and carry natural defects, so nesting cannot fill edges the way fabric markers do, and grain and stretch directions limit how pieces can be rotated. Typical yields run 55–70% for full-grain and 70–82% for corrected-grain, versus 80%+ for fabric.
Does leather type affect the warranty a brand can offer?
Yes. Full-grain can support multi-year structural warranties because the fiber structure resists wear and repairs well. Corrected-grain and split leather typically support one to two years, and bonded leather rarely supports a structural warranty at all. Match the promise to the grade, not to the price point.
Is vegetable-tanned leather better than chrome-tanned for bags?
Neither is universally better. Vegetable tanning gives a firmer hand, richer patina, and an easier environmental story, but lower water resistance and higher cost. Chrome tanning gives softer, more water-resistant, more dimensionally stable leather at lower cost. Many bag leathers combine both routes.
Conclusion
Leather grade is the single decision that shapes a bag’s durability, appearance, cost, and the claims a brand can honestly make. Full-grain keeps its grain and earns its reputation; top-grain trades a little character for consistency; corrected-grain delivers uniformity at the cost of aging; split leather is a legitimate soft-finish material with real limits; bonded leather is a fiber composite that should never be sold as hide leather.
For production teams, the practical rules are simple. Name the grade in writing. State the thickness and tolerance. Appoint the tannery. Inspect every delivery and grade what you accept. Plan yield realistically, because leather cutting wastes far more than fabric cutting. Then match the finish to the climate and the usage — and match the warranty to the grade.
Do that, and the leather you approve in sampling is the leather your customers will still be carrying a decade later.