Container Loading Plans: How Do You Stop Cartons Shifting in Transit?
Container Loading Plans: How Do You Stop Cartons Shifting in Transit?
Cargo damage in a container is rarely caused by rough handling. It is caused by the load being stable at the moment the doors close and unstable twenty minutes into the voyage, when the ship begins to move.
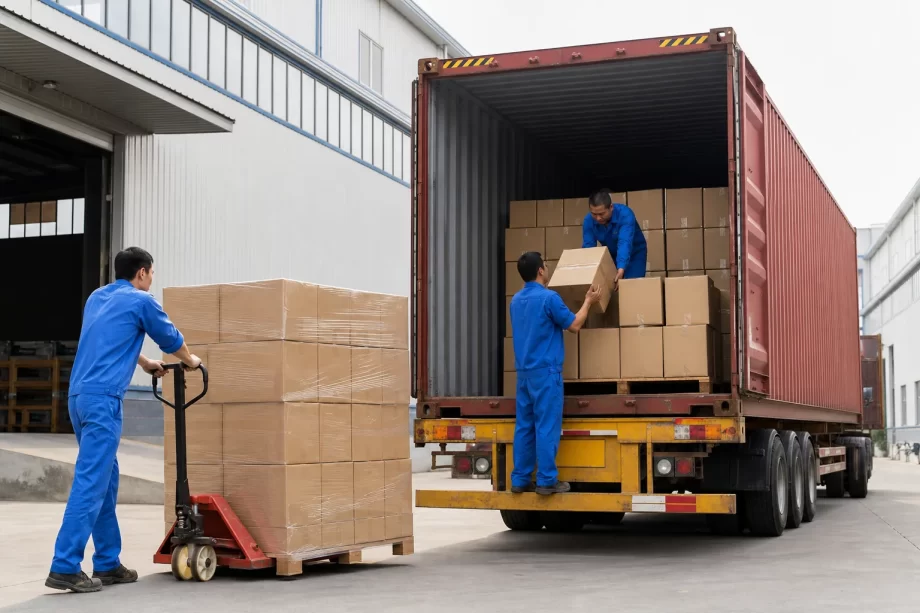
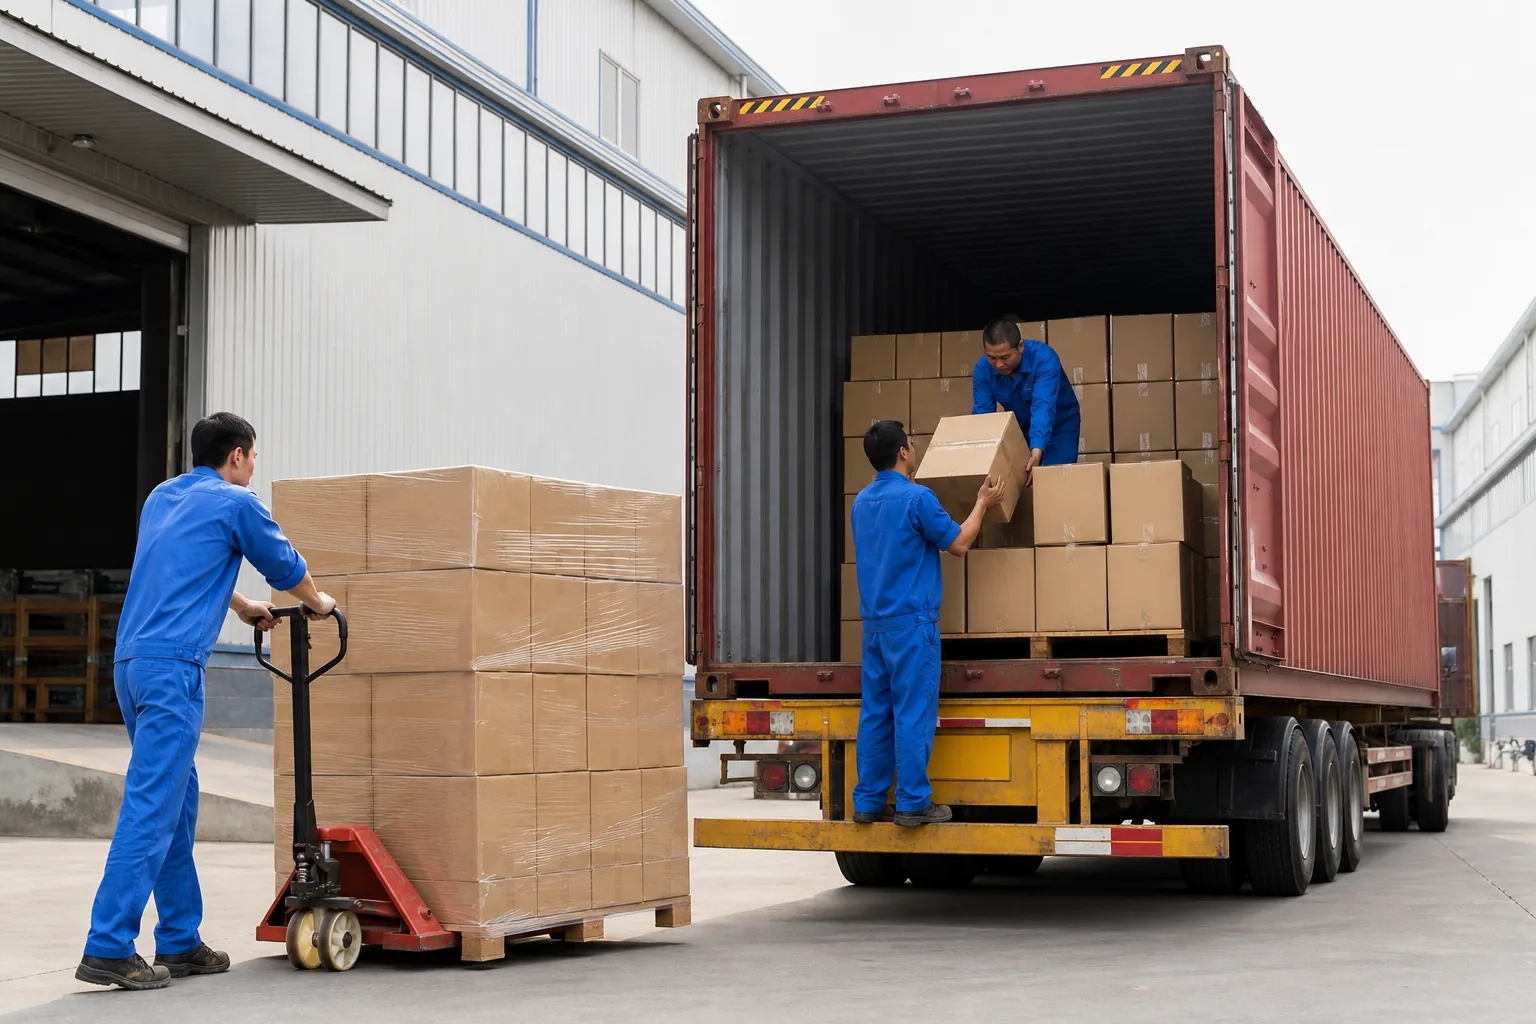
Cartons being loaded into an open shipping container at a factory dock
A backpack carton is light for its volume, which makes it easy to stack and easy to displace. A container full of these cartons can look perfectly arranged at the loading dock and arrive at the destination with the whole stack leaned against one door, cartons crushed at the bottom and hardware puncturing fabric from inside.
The fix is a plan rather than an effort. A loading plan defines what goes where, how it interlocks, what fills the gaps and how it is verified before sealing. This guide covers how that plan is built for bag cartons specifically: stack strength, interlocking patterns, weight distribution, dunnage choice, bracing methods, moisture effects and the records that decide a claim.
Understanding the motion is what makes the countermeasure obvious, and the motion is more varied than most loading crews assume.
The Motion Table
Motion
Cause
Vertical bouncing
Road and sea state
Fore-aft surge
Braking and pitching
Lateral sway
Rolling
Vibration
Engine and hull
Racking
Container flex
Settling
Compaction over time
The Force Table
Force
Effect on bags
Compression
Crushed cartons
Shear
Stack collapse
Impact
Punctures
Vibration
Abrasion damage
Moisture
Softened board
Heat
Weakened adhesive
The Transit Motion Failure Table
Failure mode
Visible result
Stack lean
Doors blocked
Bottom crush
Deformed cartons
Gap migration
Mixed cartons
Load shift
Door burst
Void collapse
Top layer drop
Moisture sag
Soft corners
The Transit Motion Cost Table
Cost
Bearer
Rejected cartons
Seller
Replacement air freight
Seller
Claim administration
Both
Repacking at destination
Buyer
Retail chargeback
Seller
Reputation
Seller
The Illusion Table
Assumption
Reality
Tight fill is enough
Voids remain
Light cargo cannot shift
Weight is not stability
Straps hold everything
Straps need anchor points
Cartons are rigid
Board softens
Drivers load carefully
Speed governs
Sealing ends risk
Risk starts after sealing
Treat the load as a structure that must remain stable under repeated acceleration in three directions, because a container is not a shelf and nothing in it stays where it was put by gravity alone.
Building the Load Plan
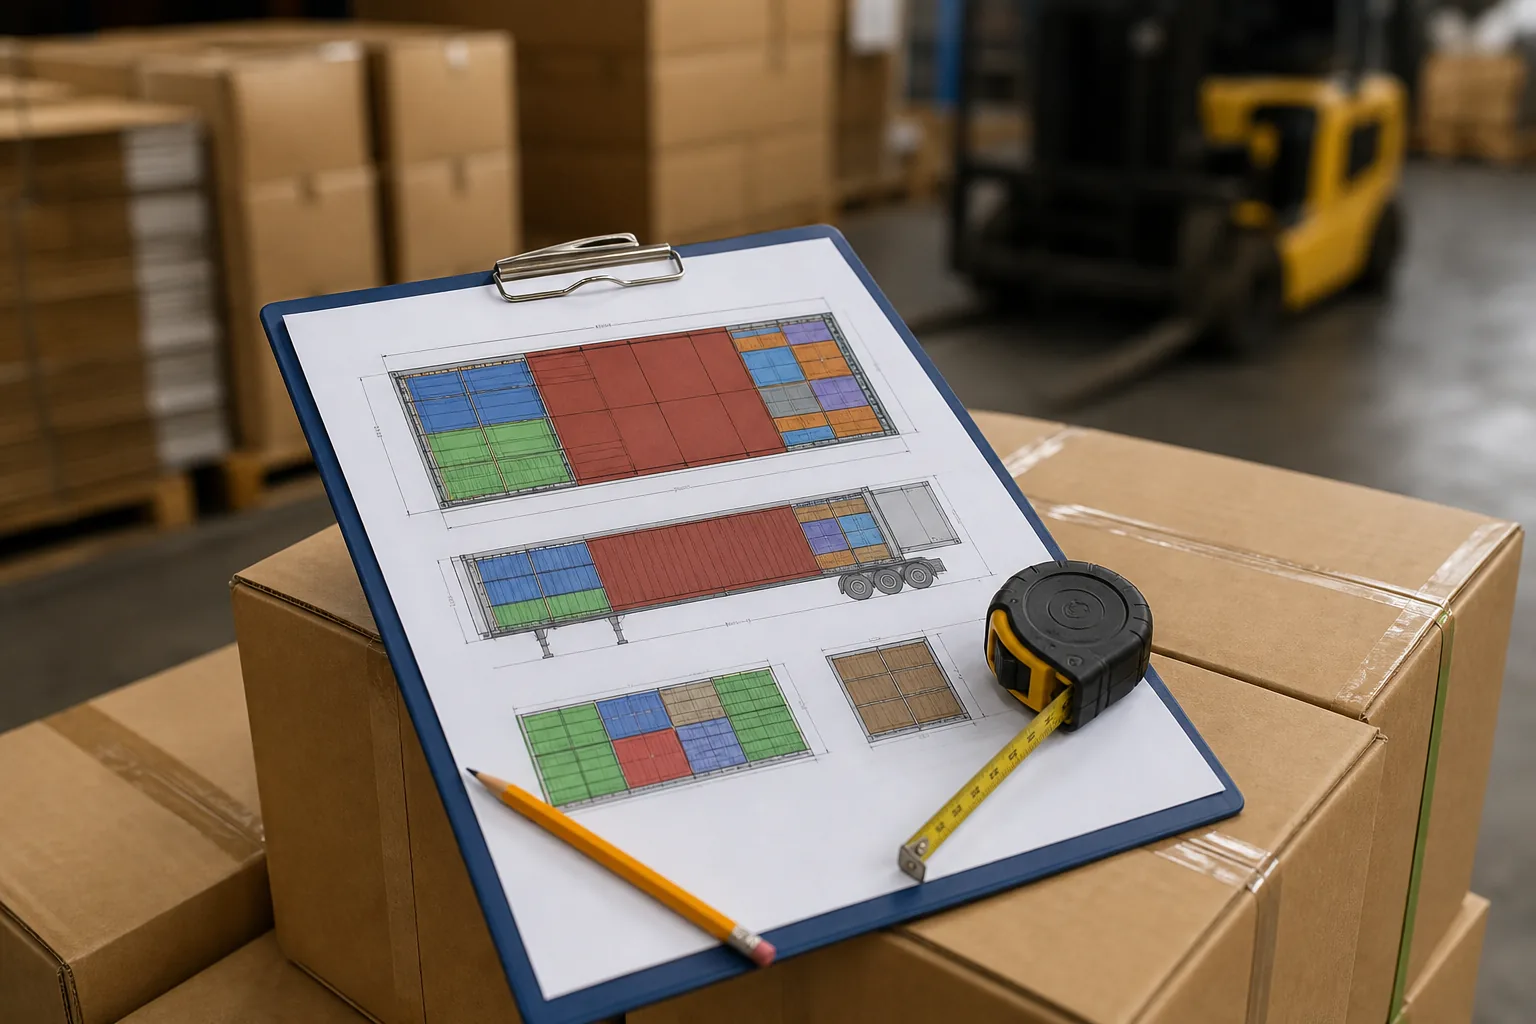
A load plan is a drawing with numbers, and it is produced before the first carton moves rather than reconstructed at the dock.
A container loading plan drawing on a clipboard resting on stacked cartons
The Input Table
Input
Source
Carton dimensions
Specification
Carton weight
Packing list
Carton strength
Board test
Container internal size
Operator data
Cargo mix
Order detail
Route conditions
Forwarder advice
The Drawing Table
Element
Shows
Plan view
Footprint layout
Elevation
Stack heights
Section
Interlock pattern
Weight map
Distribution
Dunnage points
Fill locations
Door zone
Final bracing
The Calculation Table
Step
Purpose
Volume fill
Utilisation check
Weight check
Payload limit
Stack count
Height limit
Layer count
Compression limit
Void estimate
Dunnage quantity
Balance check
Axle distribution
The Revision Table
Trigger
Action
Carton size change
Redraw
Mix change
Recalculate
Container swap
Recheck internal
Route change
Review bracing
Season change
Review moisture
Feedback from claim
Update standard
The Approval Table
Role
Confirms
Logistics
Plan feasible
Production
Carton supply
Quality
Strength adequate
Forwarder
Container type
Supervisor
Load sequence
Management
Cost accepted
Produce the plan from measured carton data rather than from habit, because a plan copied from a previous order with different carton dimensions produces a load that looks right and behaves badly.
Carton Strength and Stacking Limits
Stack height is decided by board strength and time, not by the height of the container, and the difference between the two is where crushed cartons come from.
The Test Table
Measure
Meaning
Burst strength
Puncture resistance
Edge crush
Vertical strength
Compression
Stack capacity
Board grade
Material class
Flute type
Structure
Moisture content
Strength modifier
The Derating Table
Factor
Effect on capacity
Long storage
Reduced
High humidity
Reduced
Vibration
Reduced
Poor stacking
Reduced
Oversize carton
Reduced
Vent holes
Reduced
The Height Table
Carton type
Practical stack
Small hardware cartons
Tall
Finished bag cartons
Moderate
Mixed size
Limited
Heavy cartons
Short
Soft-sided packaging
Very short
Master cartons
Per test
The Safety Table
Practice
Reason
Test a sample stack
Real capacity
Allow margin
Unknown route
Avoid mixed columns
Uneven loading
Keep within limit
Compression
Rotate stock
Age control
Inspect board
Damage
The Specification Table
Field
Requirement
Board grade
Stated
Compression value
Tested
Carton size
Toleranced
Weight limit
Declared
Print and varnish
Strength neutral
Handling marks
Applied
Reduce the calculated stack height by a working margin before loading, because laboratory compression values are measured in dry conditions and a container crossing a tropical route is not a dry condition.
Interlocking and Column Stacking
Two stacking philosophies compete in every container, and the right choice depends on whether the aim is stability or strength.
The Pattern Table
Pattern
Character
Column stack
Maximum strength
Interlocked
Maximum stability
Brick pattern
Balanced
Pinwheel
Fits odd space
Mixed
Risk of both failing
Single layer
No interlock
The Trade-off Table
Aspect
Column
Interlock
Compression
Best
Reduced
Resistance to lean
Weak
Strong
Loading speed
Fast
Slower
Void creation
Low
Higher
Damage risk
Crush
Shear
Suits
Strong board
Weak board
The Layer Table
Layer
Function
Floor layer
Foundation
Middle layers
Load transfer
Top layer
Closure
Edge column
Wall support
Door zone
Braced
Corner posts
Protected
The Alignment Table
Rule
Purpose
Corners aligned
Vertical transfer
Edges flush
No protruding
No overhang
Wall damage
Consistent gaps
Predictable
Level layers
No point loads
Square to walls
Stability
The Pattern Error Table
Error
Consequence
Mixed patterns
Uneven support
Random rotation
Weak columns
Overhang
Wall puncture
Loose layer
Collapse
Skipped layer
Height loss
Ignored corner
Corner crush
Decide the pattern once and apply it for the whole load, because a container that is half column-stacked and half interlocked has the weaknesses of both methods and the strengths of neither.
Weight Distribution and Axle Loads
Weight placement is a road safety issue before it is a cargo issue, and container weights that look acceptable in total can still be illegal at the axle.
The Distribution Table
Zone
Preference
Centre
Main mass
Front third
Heavy items
Rear third
Lighter items
Door area
Light only
Floor edges
Supported
Over wheelbase
Balanced
The Weight Limit Table
Limit
Basis
Container payload
Operator rating
Road axle limit
Local law
Floor point load
Floor rating
Stack height
Board strength
Volume
Internal size
Chassis limit
Haulier capability
The Imbalance Table
Imbalance
Consequence
Rear heavy
Axle overload
Front heavy
Steering issues
Side heavy
Roll risk
Top heavy
Lean in turns
Uneven layers
Point loading
Door heavy
Burst risk
The Measure Table
Method
Accuracy
Carton count and weight
Good
Weight bridge
Best
Load cell per axle
Good
Estimated from invoice
Weak
Visual assessment
Poor
No check
None
The Documentation Table
Document
Purpose
Packing list
Weight evidence
Verified gross mass
Legal requirement
Weighbridge ticket
Proof
Load plan
Position record
Photos
Condition record
Seal number
Integrity
Weigh the loaded container rather than trusting the sum of the cartons, because verified mass is a legal declaration and an arithmetic error in a packing list becomes a compliance problem at the terminal gate.
Void Filling Materials
Voids are the mechanism by which a stable load becomes a moving one, and the material chosen to fill them determines how well the load survives.
The Void Fill Material Table
Material
Character
Airbag
Large void fill
Paper void fill
Small gaps
Honeycomb board
Panel separation
Foam block
Localised support
Corrugated pad
Surface protection
Timber batten
Structural bracing
The Selection Table
Void type
Suitable fill
Long gap to wall
Airbag
Vertical gap
Honeycomb
Corner gap
Foam
Layer gap
Pad
Irregular space
Paper fill
Door end
Bracing
The Airbag Table
Aspect
Requirement
Size
Matches gap
Inflation
Per instruction
Pressure
Not overfilled
Surface
Smooth contact
Position
Between flat faces
Quantity
Enough to lock
The Void Fill Cost Table
Material
Relative cost
Paper fill
Low
Corrugated pad
Low
Honeycomb
Moderate
Foam block
Moderate
Airbag
Moderate
Timber bracing
High
The Void Fill Error Table
Error
Result
Underfilled airbag
No restraint
Overfilled airbag
Carton distortion
Paper only in large void
Collapse
Fill above load height
Useless
Fill behind doors only
Rear movement
Recycled loose fill
Shifting
Fill the void at the point where the load can move, not at the point that is easiest to reach, because dunnage placed for appearance rather than contact does nothing once the ship starts rolling.
Bracing and Blocking
Bracing resists movement by structure, and it works only when the brace transfers force into the container frame rather than into the cartons.
The Method Table
Method
Function
Timber batten
Horizontal restraint
Vertical post
Anti-lean
Plywood panel
Load spread
Nail plate
Joint fixing
Wedge
Gap closure
Strapping to rail
Anchoring
The Anchor Table
Anchor point
Suitability
Floor lashing ring
Strong
Side wall rail
Moderate
Corner post
Strong
Door header
Weak
Floor seam
Not suitable
Carton itself
Never
The Design Table
Requirement
Purpose
Load spread
Avoid point force
Contact area
Friction
Redundant fixing
Failure tolerance
Access for unloading
Practicality
No sharp edges
Damage control
Documented layout
Repeatability
The Bracing Material Table
Material
Use
Softwood batten
General bracing
Plywood
Panel bracing
Steel strap
Tension
Plastic strap
Light duty
Corner protector
Edge protection
Anti-slip mat
Friction
The Bracing Inspection Table
Check
Standard
Fixings tight
No movement
Contact firm
No gap
No protrusion
Wall safe
Load covered
Full height
Door clear
Opens freely
Photo taken
Evidence
Anchor bracing to the container structure and never to the cartons, because a brace fixed to the load simply becomes part of the load when the load moves.
Strapping and Lashing
Strapping adds tension where bracing adds structure, and the two are complementary rather than alternative.
The Strap Table
Type
Strength
Steel band
Highest
Heavy plastic
High
Corded strap
Moderate
Ratchet strap
High, reusable
Adhesive tape
Not structural
Shrink film
Unitising only
The Application Table
Target
Method
Palletised load
Vertical and cross
Loose cartons
Horizontal banding
Top layer
Over-band
Door stack
Diagonal brace
Mixed heights
Step bracing
Heavy items
Direct lashing
The Tension Table
Factor
Effect
Over-tension
Carton crush
Under-tension
Slack
Edge contact
Cutting
Corner protection
Load spread
Temperature
Stretch change
Humidity
Strap relaxation
The Strap Failure Table
Failure
Cause
Strap cut through carton
No corner protector
Slack strap
Wrong tension
Band snapped
Over-tension
Load still moved
Anchor too weak
Tape used as strap
Wrong material
Straps hidden
Cannot inspect
The Standard Table
Item
Requirement
Strap type
Specified
Tension method
Tool based
Corner protection
Mandatory
Spacing
Defined
Inspection
Before sealing
Record
Photographed
Specify corner protection wherever strapping crosses a carton edge, because a strap under tension will cut through board and the cut edge is where the load begins to separate.
Airbags and Inflatable Dunnage
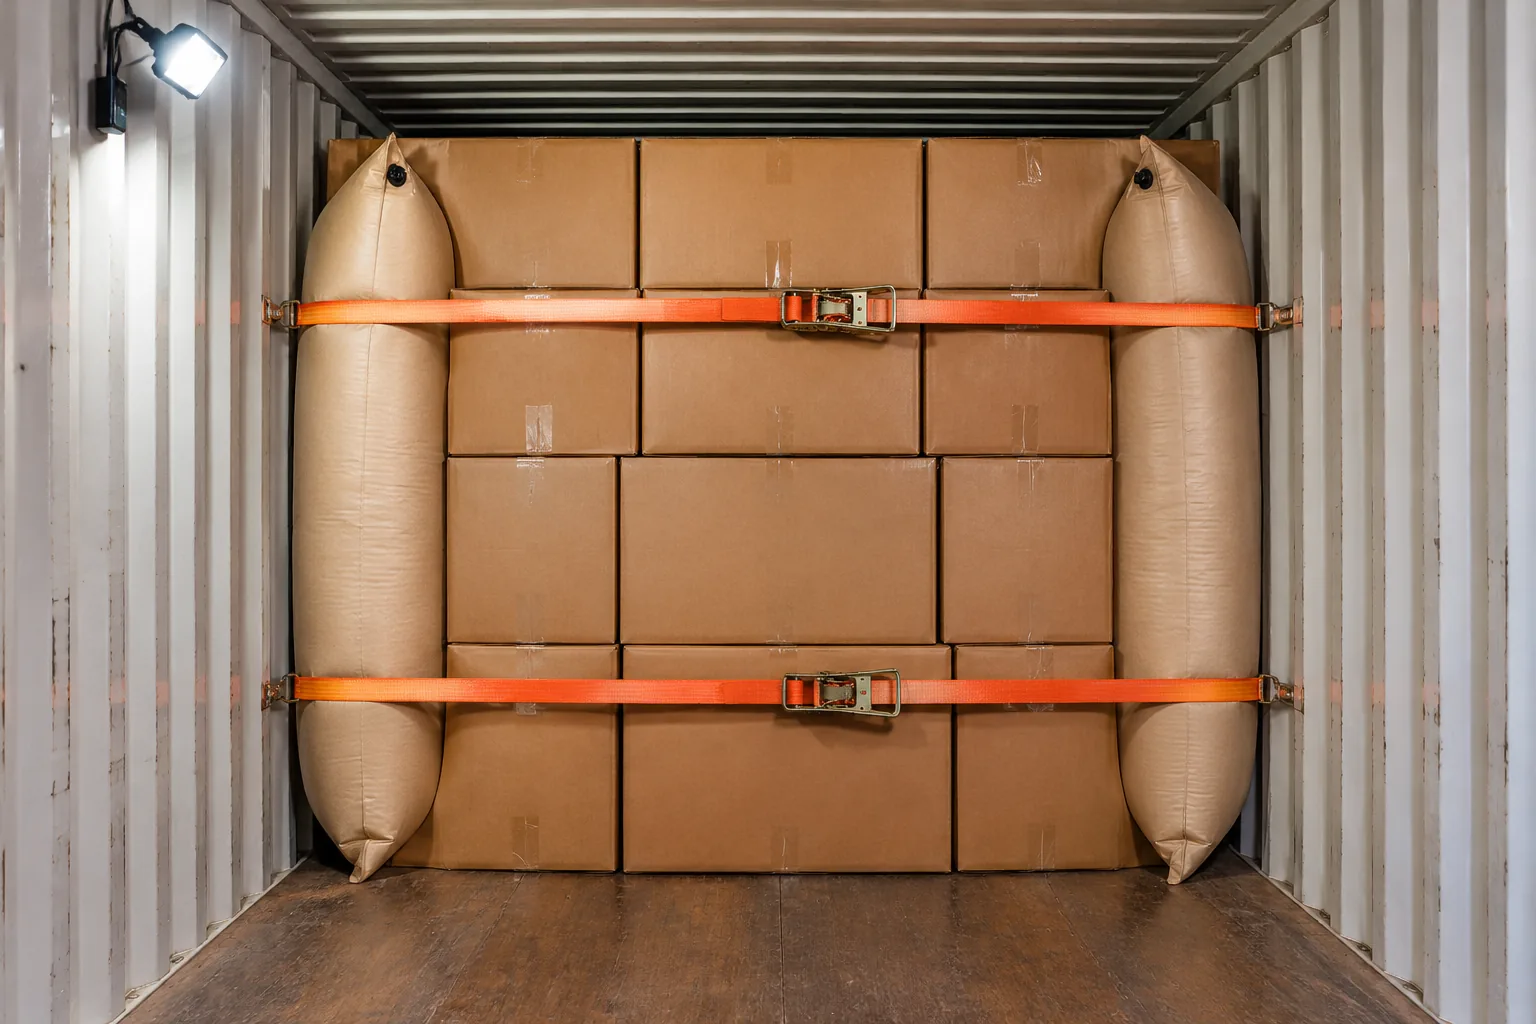
Airbags are the most cost-effective restraint for bag cartons, and the most frequently misused because they look self-explanatory.
Interior of a loaded container with cartons braced by inflatable airbags and strapping
The Size Table
Gap width
Bag choice
Narrow
Small bag
Moderate
Standard bag
Wide
Large or layered
Irregular
Multiple small
Vertical gap
Horizontal bag
Corner
Wedge plus bag
The Airbag Placement Table
Position
Purpose
Load to side wall
Lateral restraint
Load to rear doors
Rear restraint
Between blocks
Separation
Top of stack
Anti-lean
Under overhang
Support
Door end
Final lock
The Pressure Table
Stage
Action
Before inflation
Correct position
Inflation
To marked pressure
Check
Firm contact
Re-check
After ten minutes
Venting risk
Temperature drop
Record
Photo and count
The Airbag Limit Table
Limit
Reason
Gap width
Bag reach
Gap height
Bag coverage
Load weight
Force capacity
Surface
Puncture risk
Sharp edges
Protection needed
Temperature
Pressure change
The Airbag Error Table
Error
Consequence
Bag too small
No contact
Bag overinflated
Carton distortion
Bag against sharp edge
Puncture
Bag only at top
Lower load free
No re-check
Slow leak unnoticed
Mixed sizes randomly
Uneven restraint
Photograph every inflated bag after the pressure check, because an airbag claim is decided by evidence of correct placement rather than by the presence of bags in the container.
Verification Before Sealing
The last ten minutes before the doors close decide whether the previous two hours were worth doing, and verification has to be a checklist rather than a glance.
The Check Table
Check
Standard
Load square
No lean
Voids filled
Contact firm
Bracing fixed
No movement
Straps tensioned
Correct
Door zone clear
Opens
Floor clean
No debris
The Photo Table
Shot
Purpose
Empty container
Baseline
Half loaded
Pattern evidence
Fully loaded
Condition
Door end
Bracing proof
Seal close-up
Integrity
Container number
Identity
The Sign-off Table
Role
Confirms
Loader
Sequence followed
Supervisor
Checks complete
Quality
No carton damage
Logistics
Documents ready
Driver
Seal applied
Office
Photos filed
The Seal Table
Element
Requirement
Seal type
High security
Number
Recorded
Application
On camera
Photo
Clear digits
Document
On bill of lading
Discrepancy
Reported immediately
The Handover Table
Stage
Record
Dock exit
Time and seal
Terminal gate
Receipt
Vessel loading
Confirmation
Transhipment
Condition note
Arrival
Survey
Delivery
Consignee signature
Photograph the seal and the container number in one frame, because a claim that depends on proving the container was never opened needs the seal number and the container identity in the same image.
Floor Loading and Point Loads
Container floors are strong in distributed load and weak in concentration, and a bag carton sitting on a small pallet foot is a concentrated load.
The Floor Table
Element
Character
Timber floor
Distributed strength
Cross members
Span support
Fork pockets
Local weakness
Door threshold
Raised edge
Corner castings
Structural
Lashing rings
Rated points
The Load Table
Load type
Risk
Distributed cartons
Low
Pallet feet
Moderate
Steel frames
High
Machine parts
Very high
Mixed
Unpredictable
Loose hardware
Local damage
The Spread Table
Method
Effect
Plywood sheet
Load spreading
Timber bearer
Point transfer
Pallet base
Standard spread
Direct stacking
Maximum spread
Frame on floor
Concentrated
Padding
Minor help
The Floor Inspection Table
Check
Reason
Floor condition
Pre-existing damage
Protrusions
Puncture risk
Moisture
Rot and slipping
Debris
Point load
Odour
Contamination
Photo
Evidence
The Prohibition Table
Practice
Problem
Nailing into floor
Structural damage
Welding inside
Fire and damage
Heavy point load
Floor deformation
Blocking doors
Safety
Overloading corner
Frame stress
Ignoring damage
Claim denied
Spread concentrated loads with a plywood sheet or timber bearer before loading, because a floor that deforms under a point load does not recover and the deformation becomes visible evidence in a damage survey.
Heat, Humidity and Carton Softening
Board strength falls as moisture rises, and a container is a steel box that heats and cools daily, condensing water on the inside of the roof.
The Climate Table
Condition
Effect
Day heating
Vapour release
Night cooling
Condensation
High humidity
Board softening
Tropical route
Maximum risk
Cold route
Brittle board
Long transit
Cumulative
The Moisture Table
Source
Contribution
Carton board
Significant
Wood pallets
Significant
Packaging paper
Moderate
Product moisture
Low
Container floor
Moderate
Ambient air
Variable
The Control Table
Control
Method
Desiccant
Absorbs vapour
Ventilation
Limited effect
Liner
Barrier
Dry pallets
Pre-conditioned
Carton specification
Moisture resistant
Loading weather
Avoid rain
The Desiccant Table
Aspect
Guidance
Quantity
Per volume
Placement
Distributed
Type
Container grade
Monitoring
Indicator
Disposal
At destination
Record
Photo
The Consequence Table
Outcome
Effect
Soft board
Stack collapse
Wet cartons
Rejection
Mould
Total loss
Label damage
Identification loss
Metal corrosion
Hardware claims
Mixed damage
Claim dispute
Specify moisture-resistant board and a desiccant quantity for long or tropical routes, because a stack that is stable in a dry warehouse loses a third of its compression strength in a humid container.
Mixed Loads and Heavy-Light Placement
Mixed shipments are where plans are abandoned, and they are also where the damage is worst because the heavy goods damage the light ones.
The Mix Table
Combination
Risk
Bags and hardware
Puncture
Cartons and rolls
Roll movement
Finished and samples
Crush
Bag and packaging
Volume waste
Heavy and light
Compression
Fragile and bulk
Impact
The Mixed Load Placement Table
Cargo
Position
Heavy cartons
Floor, forward
Light cartons
Upper, rear
Rolls
Horizontal, chocked
Samples
Protected, top
Packaging
Fills voids
Fragile
No load above
The Separation Table
Method
Purpose
Plywood divider
Load separation
Foam sheet
Surface protection
Airbag
Position lock
Strapping
Unit cohesion
Labelling
Identification
Photo
Evidence
The Roll Table
Issue
Control
Rolling along floor
Chocks
Rolling across width
Horizontal stack
Weight concentration
Spread
Surface damage
Padding
Unloading hazard
Secured ends
Moisture
Liner
The Rule Table
Rule
Reason
Heavy below light
Compression
Dense forward
Axle load
No mixed columns
Stability
Separate by type
Damage control
Label by block
Unloading
Plan for unloading
Safety
Place heavy cargo on the floor and forward of centre, because a heavy carton placed high in the load compresses everything below it and then falls when the stack gives way.
Container Types and Their Constraints
The container is a variable in the plan rather than a constant, and each type imposes its own geometry.
The Type Table
Type
Character
Standard dry
General cargo
High cube
Extra height
Pallet wide
Euro pallet fit
Open top
Top loading
Flat rack
Over-dimension
Ventilated
Airflow
The Constraint Table
Type
Limitation
Standard
Height
High cube
Height on some routes
Pallet wide
Availability
Open top
Weather exposure
Flat rack
No side support
Ventilated
Reduced protection
The Internal Table
Dimension
Planning use
Length
Block count
Width
Row count
Height
Stack count
Door opening
Access limit
Floor area
Footprint
Tare weight
Payload
The Route Table
Route factor
Constraint
Rail leg
Height limit
Road leg
Weight limit
Ferry
Dimension limit
Inland barge
Length limit
Transhipment
Handling risk
Terminal
Equipment fit
The Booking Table
Item
Confirm
Type requested
Written
Internal size
From operator
Payload
Stated
Condition
Photo on receipt
Age and grade
Inspected
Damage
Noted on interchange
Inspect the container and photograph any damage before loading starts, because pre-existing floor or wall damage noted at interchange is the difference between a defensible claim and an argument.
Loading Sequence and Labour
Sequence determines whether the plan is physically achievable, and labour determines whether sequence is followed when the container is waiting.
The Sequence Table
Step
Purpose
Inspect
Condition baseline
Sweep
Clean floor
Mark
Position guide
Load front
Build from depth
Interlock
Pattern applied
Progress check
Maintain alignment
The Crew Table
Role
Task
Supervisor
Plan adherence
Loader
Stacking
Helper
Carton supply
Checker
Count and match
Photographer
Records
Driver
Seal and departure
The Productivity Table
Factor
Effect
Carton size
Handling ease
Stack height
Pass count
Distance
Supply time
Pattern complexity
Speed
Supervision
Consistency
Weather
Pace
The Discipline Table
Rule
Reason
Plan posted
Reference
One pattern
Consistency
No shortcuts
Stability
Count per layer
Accuracy
Stop for damage
Quality
Photo per stage
Evidence
The Problem Table
Problem
Response
Container late
Do not rush pattern
Carton short
Redraw, fill
Damage found
Segregate
Space left
Fill properly
Manpower short
Reduce scope
Weather
Protect cargo
Post the load plan inside the container and count each layer as it goes in, because a crew working from memory will finish with the wrong pattern and a container that looks full.
Photographic Records
Photographs are the only evidence that survives the voyage, and the set has to be planned in advance rather than assembled after a claim.
The Set Table
Shot
Timing
Container number
Before loading
Empty interior
Before loading
Floor condition
Before loading
Pattern detail
During loading
Full load
Before closing
Bracing detail
Before closing
The Quality Table
Requirement
Purpose
Clear focus
Identification
Even light
Detail
Wide plus close
Context
Scale reference
Size
Time stamp
Sequence
No editing
Credibility
The Archive Table
Record
Retention
Photos
Claim period
Load plan
Contract period
Weigh ticket
Regulatory
Seal record
Claim period
Damage notes
Claim period
Correspondence
Contract period
The Claim Table
Claim type
Evidence needed
Crushed cartons
Load pattern photos
Shifted load
Bracing photos
Water damage
Desiccant and liner
Puncture
Interior condition
Shortage
Count sheets
Seal breach
Seal images
The Photo Failure Table
Failure
Consequence
No photos
Claim disputed
Blurred images
Useless
Late assembly
Inconsistent
Missing seal shot
Identity gap
No date
Sequence doubtful
Photos lost
No defence
Shoot the container number, the empty floor and the finished load every time, because a claim is decided on the condition before loading and the arrangement after it, and neither can be reconstructed later.
Claims and Evidence
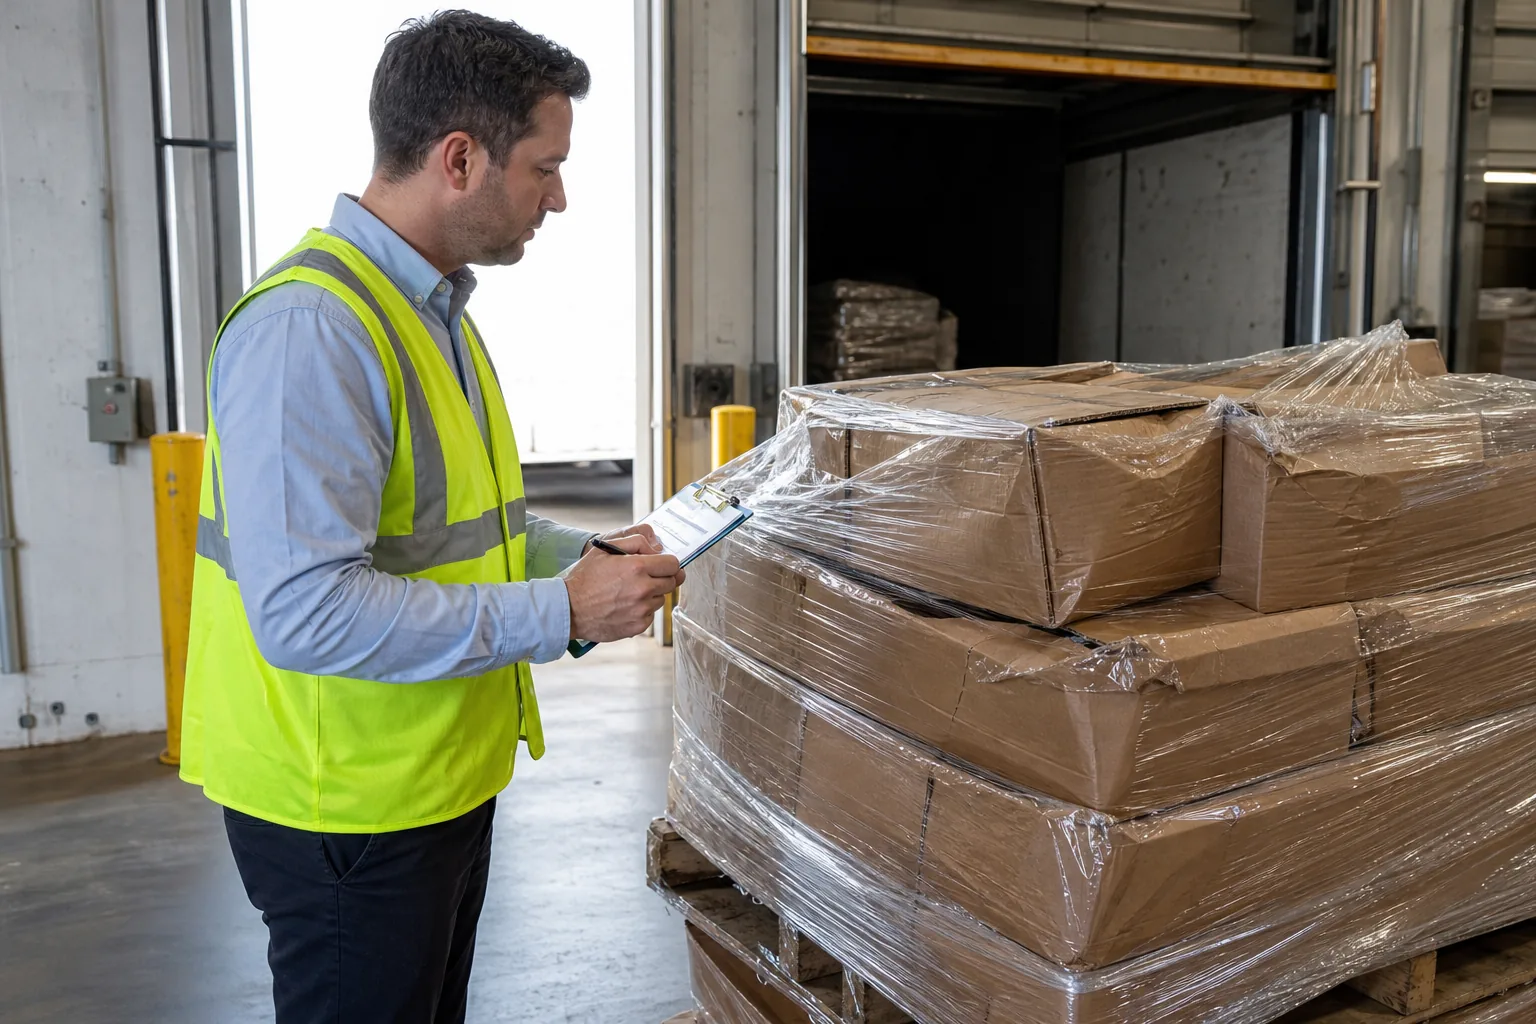
A damage claim is an evidence contest rather than a factual one, and the party with structured records recovers while the party with recollection does not.
Warehouse inspector examining dented cartons on a pallet at a receiving dock
The Stage Table
Stage
Action
On arrival
Inspect before unloading
At delivery
Note reservations
Within days
Notify carrier
Survey
Joint inspection
Documentation
Submit set
Follow-up
Track response
The Evidence Table
Document
Supports
Photos at loading
Condition
Load plan
Arrangement
Seal record
Integrity
Survey report
Damage cause
Delivery receipt
Reservations
Repair estimate
Quantum
The Cause Table
Cause argued
Evidence needed
Poor packing
Packing specification
Poor stowage
Load plan and photos
Carrier handling
Survey and tally
Inherent vice
Product data
Moisture
Desiccant record
Concealed damage
Inspection timing
The Timeline Table
Window
Requirement
At delivery
Reserve rights
Short period
Written notice
Survey window
Joint attendance
Claim filing
Within limit
Response
Carrier review
Settlement
Negotiated
The Prevention Table
Measure
Effect
Standard pack spec
Reduces disputes
Photo protocol
Proof
Seal discipline
Integrity
Survey at arrival
Early evidence
Claim register
Pattern detection
Feedback loop
Design change
Reserve rights in writing at the moment of delivery even when the damage looks minor, because a clean signature on a delivery receipt is treated as evidence that the cargo arrived in good condition.
Common Shifting Failures
The same failures recur across container loads, and each has a specific cause that a plan can address.
The Shifting Failure Table
Failure
Cause
Load leaned to one side
Pattern not interlocked
Rear stack collapsed
Door zone unbraced
Cartons crushed low
Stack over limit
Mixed cartons scattered
Voids unfilled
Rolls moved
No chocks
Top layer displaced
No over-band
The Detection Table
Signal
Meaning
Door hard to open
Load moved
Cartons out of square
Shear force
Corner deformation
Point load
Water staining
Condensation
Strap marks
Over-tension
Mixed stacking order
Disturbance
The Root Cause Table
Root cause
Prevention
No plan
Written drawing
Plan not followed
Supervision
Wrong dunnage
Specification
Carton too weak
Board upgrade
Loading rushed
Scheduling
No verification
Checklist
The Remedy Table
Finding
Action
Pattern failure
Retrain crew
Board failure
Re-specify carton
Dunnage shortage
Stock control
Bracing missing
Kit per load
Moisture
Desiccant increase
Repeated claims
Review plan
The Learning Table
Practice
Benefit
Log every claim
Pattern visibility
Photograph standard
Comparability
Review quarterly
Early correction
Share with forwarder
Joint fix
Update plan template
Institutional memory
Train new crews
Consistency
Log every damage event with its cause, because single claims look like bad luck and a register of ten similar claims looks like a loading plan that needs rewriting.
Programme Ownership and Cost
A loading standard without an owner decays into habit, and the cost of the programme is small compared with one rejected container.
The Owner Table
Role
Duty
Logistics manager
Plan owner
Supervisor
Execution
Quality
Pack specification
Purchasing
Dunnage supply
Finance
Claim tracking
Management
Standard approval
The Programme Cost Table
Element
Relative cost
Dunnage materials
Low
Strapping and corners
Low
Desiccant
Low to moderate
Labour time
Moderate
Training
One-off
Damage avoided
Very high
The Budget Table
Item
Basis
Airbags per container
By void estimate
Strapping per load
By pattern
Desiccant per container
By volume
Photo time
Minutes
Inspection
Per container
Claim reserve
Historical
The Indicator Table
Metric
Target direction
Damage rate
Down
Claim value
Down
Carton rejection
Down
Loading time
Stable
Plan adherence
Up
Photo completeness
Up
The Review Table
Frequency
Action
Per shipment
Check and record
Monthly
Damage summary
Quarterly
Plan review
Annually
Specification review
On claim
Root cause
On route change
Re-plan
Fund the dunnage as a fixed cost per container rather than a variable to be trimmed, because the money saved on airbags is recovered by the buyer as a damage claim with interest.
The Loading Plan Checklist
Before Loading
Item
Done
Container inspected
☐
Container number recorded
☐
Floor photographed
☐
Plan posted
☐
Dunnage staged
☐
Carton count confirmed
☐
During Loading
Item
Done
Pattern followed
☐
Layers counted
☐
Weight placement checked
☐
Voids filled
☐
Bracing fixed
☐
Progress photographed
☐
Before Sealing
Item
Done
Load square
☐
Door zone clear
☐
Straps tensioned
☐
Airbags checked
☐
Seal applied and photographed
☐
Documents matched
☐
FAQ
What causes most carton shifting in container shipments?
Unfilled voids and a pattern that does not interlock. A load can look tight at the door and still contain gaps between blocks that open up once the container starts to pitch and roll. Movement then concentrates at the weakest point, usually the bottom layer or the door end, and the visible result is a leaned stack or crushed corner cartons. Filling voids at the point of possible movement and locking the pattern resolves most of it.
Should bag cartons be column stacked or interlocked?
Column stacking carries the most vertical load and suits strong board on short routes. Interlocking resists lean and suits weaker board or long sea voyages, at the cost of some compression strength because load paths no longer run straight down. The decision follows the board grade and the route, and it should be made once for the whole load rather than mixed block by block.
How many airbags does a container need?
Enough to fill every gap where the load can move, which is an outcome rather than a fixed number. The count comes from the plan: gap width, gap height and the number of blocks determine bag size and quantity. The practical test is firm contact across the full height of the gap after inflation, with a re-check a few minutes later to catch a slow leak or a temperature-driven pressure drop.
Can we strap the cartons to each other instead of bracing to the container?
Unitising cartons together helps them behave as one block, but it does not anchor that block to the container. Without a connection to the floor rings, side rails or a structural brace, the unitised block slides as a single mass, which concentrates force and can burst the doors. Use strapping for cohesion and bracing for restraint.
Why do cartons crush even when the stack is within the tested limit?
Because tested compression values assume dry board and a short duration. In a container, humidity softens the board, vibration cycles the load, and the stack may sit for weeks. Each of those reduces real capacity. Loading below the calculated limit, specifying moisture-resistant board and controlling carton moisture at packing are the practical responses.
Does a desiccant really matter for bag cartons?
It matters on long or tropical routes, where daily heating and cooling drives condensation onto the container roof and then onto the top layer. Board, pallets and paper packaging all release vapour inside a closed container. Desiccant absorbs that vapour and keeps the board drier, which protects both the cartons and the metal hardware inside them.
What photographs should we take before the doors close?
A consistent set: the container number, the empty interior and floor before loading, the pattern during loading, the completed load, the bracing and airbag detail, and the seal with the number legible. The set should be repeatable across shipments so that a claim can be compared against a normal load rather than argued from memory.
Who pays when cargo arrives damaged?
It depends on the cause and the evidence. If the load plan, packing and bracing were sound and the survey shows external impact or handling damage, the carrier or its insurer bears it. If the survey finds an unstable pattern, weak board or unfilled voids, the shipper carries it. That is why loading photographs and a documented standard matter more than the argument made after arrival.
Conclusion
Cartons shift because a container is a moving structure, not because a crew was careless. The countermeasures are ordinary engineering: a plan built from measured carton data, a pattern chosen for the board grade, weight placed low and forward, voids filled where movement is possible, bracing anchored to the container rather than the cargo, and a verification routine before the doors close.
None of it is expensive. Airbags, strapping, corner protectors and a modest quantity of desiccant cost a small fraction of a rejected container, and the photographic record costs a few minutes of a supervisor’s time.
The difference between a factory that ships without damage and one that argues about it every quarter is rarely equipment. It is whether the loading plan exists as a document that a crew follows and a supervisor checks, or as an understanding that changes with whoever is standing at the dock that morning.