Most bag programs are limited not by design ambition but by supplier capability. A brand can specify a construction, a material, and a tolerance, and still receive goods that miss all three because the factory has never built that product type before and has no system for learning how.
Supplier development is the discipline of closing that gap deliberately. Instead of switching suppliers whenever a program proves too difficult, the buyer invests in raising the supplier’s capability until the difficulty disappears, and in doing so converts a transactional relationship into a capacity that competitors cannot easily copy.
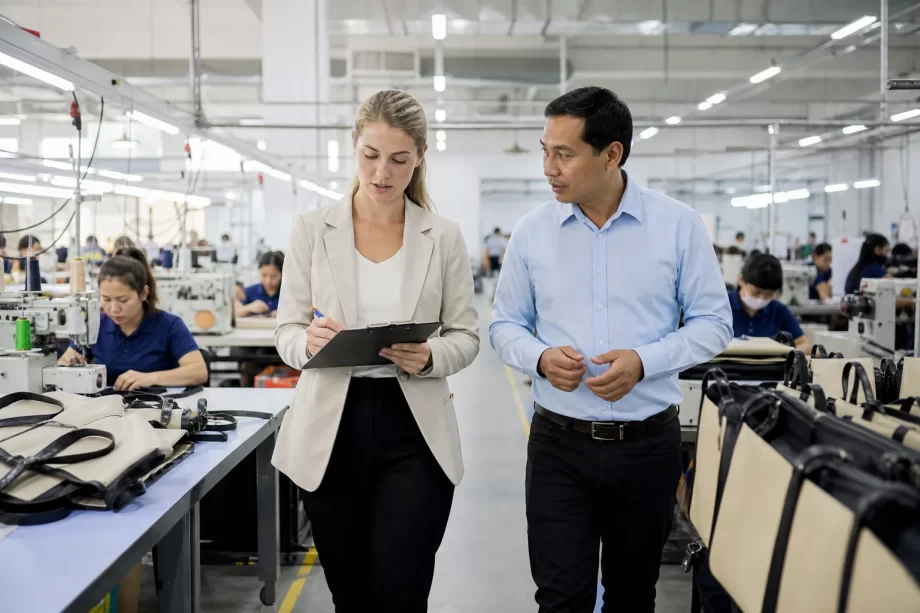
Auditor assessing a bag factory production floor with a checklist
This guide covers the manufacturer’s and buyer’s view of supplier development: how capability is assessed, how gaps are analysed and prioritised, how a development plan is built and resourced, how technical support and quality systems are transferred, how capacity and delivery reliability are developed, how progress is measured, and how the process is handled when a supplier does not respond.
Switching suppliers carries hidden costs that are rarely counted when a program runs into difficulty. Development usually costs less than replacement, and it retains the knowledge that has already been built.
The Cost Comparison Table
Route
Character
Develop the existing supplier
Investment in capability
Replace the supplier
Search, sampling, and risk
Split the order
Risk sharing, higher administration
Bring production in house
Capital and management burden
Re-specify the product
Redesign cost and lost features
The Switching Cost Table
Cost element
Character
Supplier search
Management time
Auditing and qualification
Travel and assessment
Sampling rounds
Materials and labour
Learning curve
Early quality loss
Volume ramp
Slower first orders
Relationship reset
Trust rebuild
The Development Benefit Table
Benefit
Effect
Retained knowledge
The factory already knows the product
Faster improvement
Focused intervention
Better pricing over time
Efficiency shared
Capacity priority
Preferred customer status
Lower risk
Proven partner
Competitive barrier
Capability others lack
The Development Trigger Table
Trigger
Signal
Repeated defects
Quality system gap
Late deliveries
Planning or capacity gap
Failing a new product type
Technical gap
Rising cost
Efficiency gap
Audit non-conformity
System gap
Buyer program escalation
Capability mismatch
The Decision Table
Situation
Preferred route
Capable supplier, one weakness
Develop
Systemic management failure
Replace or restructure
New product, capable plant
Develop with technical support
Chronic integrity problem
Replace
Strategic long-term volume
Develop
Buyer note: The cheapest moment to develop a supplier is before the program is placed, not after a shipment fails. Capability work done during sampling costs a fraction of the same work done under delivery pressure, and it changes the factory’s default behaviour rather than applying a temporary correction.
Assessing Supplier Capability
Development begins with an honest measurement. An assessment that flatters the supplier produces a plan that addresses the wrong problems.
The Assessment Dimensions Table
Dimension
What is measured
Technical
Product types built, tooling, machine set
Quality system
Control, inspection, traceability
Capacity
Output, peak capability, lead time
Delivery
On-time performance, planning
Materials
Sourcing, stock control, traceability
Workforce
Skills, training, retention
Management
Organisation, communication, planning
Compliance
Legal, social, environmental
The Evidence Table
Dimension
Evidence to collect
Technical
Sample history, equipment list
Quality system
Records, inspection reports
Capacity
Production records, line counts
Delivery
Shipment history
Materials
Purchase records, lot control
Workforce
Training records, headcount
Management
Organisation chart, meeting records
Compliance
Certificates, audit reports
The Rating Scale Table
Level
Description
1
Does not meet requirement
2
Partially meets, informal
3
Meets, documented
4
Meets with measurement
5
Meets, measured, continuously improved
The Assessment Method Table
Method
Use
Document review
System existence
Site walkthrough
Actual practice
Interview
Understanding
Product inspection
Output reality
Record sampling
Consistency
Trial order
Performance proof
The Assessment Pitfall Table
Pitfall
Effect
Auditing the showroom, not the line
False capability picture
Accepting documents at face value
Systems that do not operate
Assessing only quality
Missing capacity and delivery
Assessing once
Snapshot rather than trend
Scoring generously
Wrong priorities
Capability Gap Analysis
An assessment produces a list. Gap analysis turns that list into a priority order by weighing each gap against its effect on the program.
The Gap Table
Gap
Consequence
No measurement system
Dimensional drift
No incoming inspection
Material defects reaching the line
Untrained operators
Rework and variation
No production plan
Late delivery
Weak traceability
Unable to contain a problem
No corrective action process
Repeating failures
The Priority Table
Criterion
Weight
Effect on the customer
Highest
Safety or compliance
Highest
Frequency of occurrence
High
Cost of the failure
High
Ease of correction
Moderate
Cost of the correction
Moderate
The Quick Win Table
Gap
Quick intervention
No reference sample at the line
Mount one
Unclear specification
Reissue with clarity
No incoming check
Introduce a simple record
No operator briefing
Daily five-minute review
Untidy materials storage
Segregate by lot
The Structural Gap Table
Gap
Longer intervention
No quality organisation
Appointment and training
No planning function
Planning role and tools
No testing capability
Equipment and method
No traceability system
Records and coding
No improvement process
Structured review cycle
The Root Cause Table
Visible problem
Underlying gap
Late shipments
No capacity planning
Colour variation
No material approval process
Loose hardware
No tooling control
Inconsistent stitching
No work instruction
High rework
No in-line inspection
The Prioritisation Table
Order
Focus
1
Anything affecting safety or compliance
2
Anything causing customer rejection
3
Anything causing delivery failure
4
Anything causing cost escalation
5
Anything improving long-term capability
Building the Development Plan
A development plan is a project, not a wish list. It needs an owner, milestones, evidence of completion, and a review rhythm.
The Plan Element Table
Element
Content
Objective
The capability to be built
Gap addressed
The measured deficiency
Actions
Specific steps
Owner
Factory and buyer
Resources
People, time, equipment
Milestone
Completion evidence
Review date
Scheduled check
The Milestone Table
Milestone
Evidence
Procedure written
Document issued
Staff trained
Training record
Equipment installed
Commissioning record
First output checked
Inspection report
Performance stable
Three consecutive lots
Capability confirmed
Assessment score
The Resourcing Table
Resource
Source
Technical specialist
Buyer or third party
Training time
Factory, within working hours
Equipment
Factory investment
Documentation
Buyer templates
Travel
Buyer budget
Follow-up
Regular visits
The Responsibility Table
Task
Typically owned by
Defining the standard
Buyer
Adopting the standard
Factory
Providing training
Buyer or specialist
Building the system
Factory
Monitoring progress
Both
Verifying capability
Buyer
The Review Rhythm Table
Cadence
Content
Weekly during active work
Actions and blockers
Monthly
Progress against milestones
Quarterly
Capability reassessment
Annual
Relationship and strategy
The Documentation Table
Document
Purpose
Assessment report
Baseline
Gap analysis
Priorities
Development plan
Actions and owners
Progress log
Evidence of work
Reassessment report
Measured change
Technical Support and Training
Technical transfer is the most concrete form of development. It changes what the factory can physically produce, and it stays in the plant after the project ends.
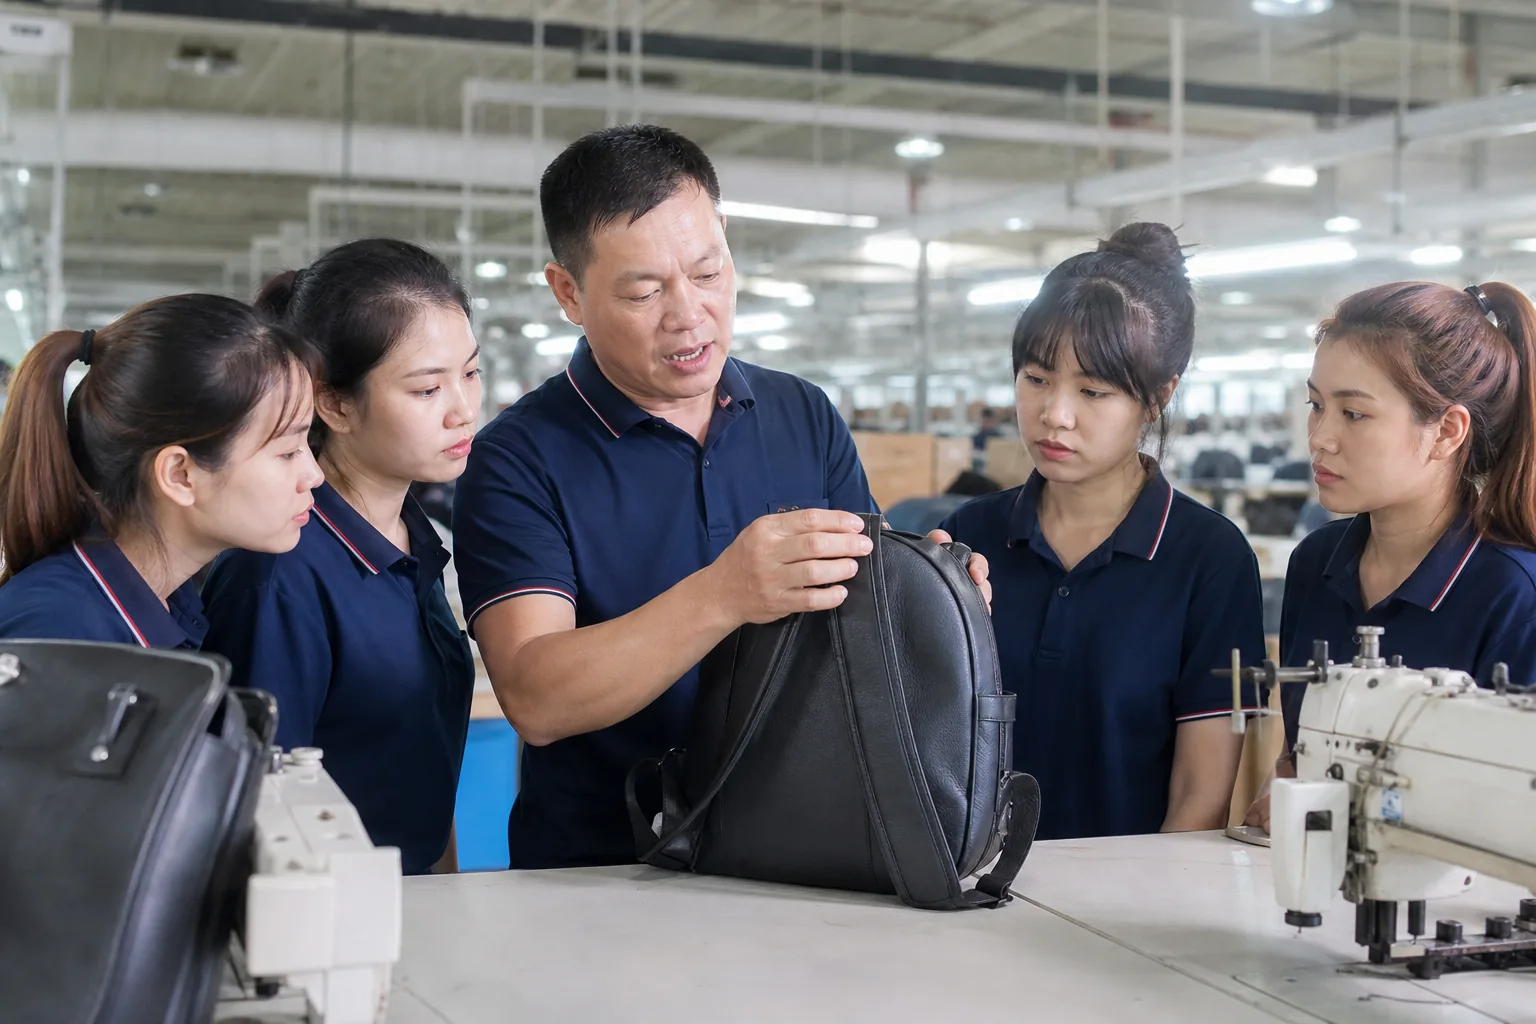
Training session demonstrating stitching technique to operators
The Technical Transfer Table
Area
Support provided
Construction methods
Demonstration and instruction
Machine settings
Parameters and trials
Tooling
Die and mould design guidance
Pattern interpretation
Reading and using the pattern
Material handling
Cutting and preparation practice
Assembly sequence
Documented work instruction
The Training Format Table
Format
Strength
On-the-job demonstration
Fast, practical
Classroom session
Theory and background
Sample workshop
Hands-on with real product
Video reference
Repeatable
Written instruction
Permanent
The Training Content Table
Topic
Audience
Construction detail
Operators
Inspection method
Inspectors
Measurement technique
Quality staff
Machine parameter control
Technicians
Material identification
Cutting and store staff
Corrective action
Supervisors
The Skills Matrix Table
Role
Core skills
Operator
Operation, self-check
Senior operator
Multi-operation, training
Inspector
Measurement, judgement
Supervisor
Escalation, planning
Technician
Setting, maintenance
Quality engineer
Method, analysis
The Training Record Table
Field
Purpose
Trainee
Identification
Topic
Content covered
Date
Chronology
Trainer
Source of instruction
Assessment
Competence confirmed
Follow-up
Reinforcement scheduled
The Transfer Barrier Table
Barrier
Response
High staff turnover
Written standards, not verbal
Resistance to change
Demonstrate the benefit
Language gap
Visual instruction and samples
No dedicated trainer
Train the trainer
No time allocated
Schedule within production
Factory note: A written work instruction combined with a mounted reference sample survives staff turnover; a verbal explanation does not. Where turnover is high, the documentation is the only part of the training that keeps working.
Quality System Development
Quality development installs the controls that let a factory find its own problems. The objective is independence: a supplier that can detect and correct deviations without the buyer’s intervention.
The System Component Table
Component
Function
Incoming inspection
Material verification
In-process check
Early deviation detection
Final inspection
Release decision
Measuring equipment
Objective judgement
Records
Traceability
Corrective action
Problem removal
The Inspection Point Table
Point
Check
Goods in
Material, colour, quantity
Cutting
Panel accuracy, direction
Preparation
Components complete
Assembly
Construction sequence
Finishing
Hardware, labels
Packing
Presentation and count
The Measuring Equipment Table
Equipment
Use
Measuring tape and rule
Dimensions
Callipers
Hardware and foam
Light box
Colour assessment
Tensile tester
Joint strength
Timer
Cycle testing
Scales
Weight check
The Record Table
Record
Content
Inspection report
Result and disposition
Defect log
Type and frequency
Rework record
Quantity and cause
Corrective action
Cause and fix
Traceability record
Lot and unit identity
Calibration record
Equipment validity
The Corrective Action Table
Step
Action
Contain
Stop the affected goods
Describe
Define the problem precisely
Analyse
Identify the cause
Correct
Remove the cause
Verify
Confirm the fix works
Standardise
Update the procedure
The Independence Table
Stage
Character
Early
Buyer detects and instructs
Developing
Factory detects, buyer verifies
Developing further
Factory detects and corrects
Independent
Factory detects, corrects, and prevents
Advanced
Factory improves proactively
Capacity and Delivery Development
Delivery failure is usually a planning failure. A factory that cannot forecast its own load will promise dates it cannot meet, and no amount of inspection will fix a schedule that was never achievable.
Supervisor and workers reviewing workstation layout on an assembly line
The Planning Component Table
Component
Function
Order register
Visibility of commitments
Capacity model
Available hours by process
Load calculation
Demand against capacity
Material plan
Availability before start
Bottleneck view
Constraint identification
Progress tracking
Early warning
The Capacity Table
Factor
Measurement
Machine hours
Available by process
Labour hours
Available by skill
Efficiency rate
Actual against theoretical
Rework allowance
Historical percentage
Absence allowance
Historical percentage
Peak limit
Maximum sustainable
The Delivery Metric Table
Metric
Meaning
On-time delivery
Against the confirmed date
Lead time actual
Against the quoted lead time
Order completion
Quantity and completeness
Schedule adherence
Progress against plan
Recovery speed
Time to recover from disruption
The Planning Improvement Table
Weakness
Development action
No order register
Introduce a simple schedule
No capacity view
Build a process capacity table
Unrealistic promises
Quote from capacity
Material surprises
Confirm availability before start
No early warning
Daily progress review
The Capacity Growth Table
Route
Requirement
Additional shifts
Workforce and supervision
Additional lines
Equipment and space
Outsourcing
Control of subcontractors
Efficiency improvement
Method and training
Layout improvement
Flow and handling
The Reliability Table
Stage
Character
Unreliable
Dates missed without warning
Becoming reliable
Dates missed with notice
Reliable
Dates met, exceptions rare
Highly reliable
Dates met with buffer
Commercial and Relationship Development
Capability development only holds if the commercial relationship supports it. A supplier that has improved but is squeezed on price will eventually revert to the behaviours that were cheap.
The Commercial Element Table
Element
Content
Price
Transparent cost structure
Payment terms
Predictable and fair
Volume commitment
Stated and honoured
Lead time
Realistic and stable
Forecast sharing
Visible demand
Investment sharing
Shared cost of improvement
The Incentive Table
Incentive
Effect
Volume commitment
Encourages investment
Longer agreement
Enables planning
Priority status
Rewards performance
Investment support
Shares risk
Public recognition
Motivates management
The Relationship Stage Table
Stage
Character
Transactional
Order by order
Preferred
Regular allocation
Partner
Joint planning
Strategic
Joint development
The Communication Table
Mechanism
Frequency
Operational contact
Daily during production
Review meeting
Monthly
Business review
Quarterly
Development review
Per plan milestone
The Escalation Table
Level
Trigger
Operational
Routine issue
Management
Repeated issue
Senior management
Program risk
Commercial
Contractual consequence
The Relationship Risk Table
Risk
Mitigation
Improvement not rewarded
Link volume to performance
Price pressure after development
Cost transparency
Key contact leaves
Multiple interfaces
Competitor approached by supplier
Agreement and trust
Measuring Progress
Progress is measured against the baseline, and the baseline must be recorded before the work begins. Without it, improvement is a matter of opinion.
The Metric Table
Metric
Baseline need
Defect rate
Historical records
Rework rate
Historical records
On-time delivery
Shipment history
First-pass yield
Inspection data
Customer complaints
Claim records
Assessment score
Initial assessment
The Evidence Table
Claim
Evidence required
Defects reduced
Inspection records before and after
Delivery improved
Shipment records
Capability raised
Reassessment result
Training completed
Training records
System installed
Documented procedure
The Review Table
Interval
Question
Monthly
Are the actions happening?
Quarterly
Is the metric moving?
Annually
Is capability genuinely higher?
The Stagnation Table
Symptom
Likely cause
Plan not progressing
No owner or no time allocated
Metrics flat
Wrong root cause addressed
Improvement then relapse
No standardisation
Data unavailable
No records kept
Training repeated
No written standard
The Verification Table
Method
Strength
Record review
Objective and cheap
Site visit
Confirms practice
Trial order
Performance proof
Reassessment
Full picture
Audit
System confirmation
The Recognition Table
Achievement
Response
Milestone met
Formal acknowledgement
Metric improved
Increased allocation
Capability level raised
Preferred status
Sustained excellence
Long-term agreement
Continued support
Joint development
Managing Difficult Suppliers
Not every supplier responds to development. Recognising the difference between a supplier that cannot improve and one that will not is a commercial judgement, and it should be made early rather than after several failed shipments.
Supplier performance review meeting with records on the table
The Response Pattern Table
Pattern
Signal
Approach
Willing and capable
Actions completed
Support and expand
Willing, not capable
Actions attempted, weak
Technical support
Capable, not willing
Capability present, no action
Commercial pressure
Neither
No capability, no engagement
Replace
The Non-Response Table
Behaviour
Read as
Actions promised, not done
Priority or capacity problem
Records not produced
System absence or evasion
Blame shifted to materials
Willingness to investigate lacking
Same defect repeated
Corrective action not real
Access restricted
Something concealed
Price used as the only answer
Commercial-only relationship
The Intervention Table
Level
Action
1
Reminder and revised deadline
2
Management meeting with a plan
3
Conditional order status
4
Escalation to senior management
5
New business suspended
6
Exit
The Conditional Status Table
Condition
Requirement
New orders
Subject to verification
Inspection
Increased level
Shipment
Pre-shipment inspection mandatory
Payment
Revised terms
Duration
Until metrics recover
The Exit Criteria Table
Criterion
Threshold
Repeated non-conformity
Three consecutive lots
Delivery failure
Two consecutive orders
Integrity breach
Immediate
Compliance failure
Immediate
Refusal to engage
After formal escalation
The Exit Table
Step
Action
1
Confirm the record is complete
2
Notify formally
3
Secure tooling and samples
4
Recover outstanding materials
5
Close open orders
6
Transfer to the new source
The Replacement Risk Table
Risk
Mitigation
New supplier repeats the problem
Assess capability first
Tooling lost or withheld
Contractual clarity
Knowledge lost
Document before exit
Lead time gap
Overlap production
Cost and Resourcing
Supplier development has a budget and a payback. Treated as an unbudgeted favour, it does not happen; treated as a project with resources, it produces measurable returns.
The Cost Element Table
Element
Character
Assessment time
Management and travel
Technical support
Specialist days
Training
Factory hours and materials
Documentation
Template and translation
Equipment
Factory investment
Follow-up visits
Travel and time
The Buyer Cost Table
Activity
Typical burden
Initial assessment
Days per supplier
Development planning
Days per plan
Technical visits
Days per visit
Verification
Days per milestone
Records and reporting
Ongoing
The Factory Cost Table
Activity
Typical burden
Management time
Ongoing
Training hours
Production time
Equipment
Capital
Records
Administration
Sampling for verification
Materials and labour
The Payback Table
Improvement
Return
Defect reduction
Less rework and fewer claims
Delivery improvement
Lower expediting cost
Efficiency gain
Price stability
Independence
Less buyer supervision
Capability gain
Access to new product types
The Investment Decision Table
Situation
Decision
High volume, capable supplier
Invest
Low volume, capable supplier
Light support
High volume, weak supplier
Develop or replace
Low volume, weak supplier
Replace
Strategic product
Invest regardless of volume
The Resourcing Table
Resource
Source
Technical specialist
Internal or external
Trainer
Internal or contracted
Templates
Buyer standard documents
Budget
Program cost
Time
Scheduled, not spare
The Cost of Inaction Table
Inaction
Consequence
No development
Repeated defects
No records
Unresolvable disputes
No planning
Chronic lateness
No standardisation
Turnover-driven variation
No exit decision
Permanent underperformance
Development Priorities by Supplier Type
The right development focus depends on what the supplier contributes. A fabric mill, a hardware supplier, and an assembly factory fail in different ways, and the intervention should match the failure mode.
The Supplier Type Table
Supplier type
Common weakness
Fabric mill
Shade consistency, lot variation
Coating and lamination
Adhesion, hand feel
Hardware and injection
Tolerance, finish
Zipper supplier
Slider function, tape shade
Webbing supplier
Width and stretch consistency
Assembly factory
Construction, systems
The Priority Table
Supplier type
Development focus
Fabric mill
Colour control and lot records
Coating and lamination
Process parameters and testing
Hardware and injection
Mould control and inspection
Zipper supplier
Functional testing and grade control
Webbing supplier
Specification and measurement
Assembly factory
Systems, planning, and training
The Evidence Table
Supplier type
Key evidence
Fabric mill
Colour approval and lot traceability
Coating and lamination
Test reports and parameter logs
Hardware and injection
Dimensional reports and load tests
Zipper supplier
Cycle test and tensile results
Webbing supplier
Measured width and elongation
Assembly factory
Inspection records and delivery history
The Integration Table
Interface
Development need
Mill to cutting
Shade and lot consistency
Component to assembly
Tolerance and completeness
Assembly to packing
Presentation and count
Supplier to supplier
Shared standards
The Multi-Tier Table
Tier
Who manages development
Tier 1
Buyer or assembly factory
Tier 2
Tier 1 supplier, verified by buyer
Tier 3
Tier 1 supplier, documented
Shared
Joint where the standard is buyer-specified
The Verification Table
Claim
How to verify
Consistency improved
Lot comparison records
Testing introduced
Test reports over time
Parameters controlled
Parameter logs
Standards applied
Inspection against specification
The Supplier Development Checklist
Assessment
Item
Done
Assessment dimensions defined
☐
Evidence collected for each dimension
☐
Rating scale applied consistently
☐
Site walkthrough conducted on the line
☐
Records sampled rather than accepted
☐
Baseline documented and dated
☐
Gap Analysis
Item
Done
Gaps listed with consequences
☐
Safety and compliance gaps placed first
☐
Customer-affecting gaps identified
☐
Quick wins distinguished from structural work
☐
Root causes traced rather than symptoms listed
☐
Priorities agreed with the supplier
☐
Development Plan
Item
Done
Objectives stated with evidence of completion
☐
Actions assigned to named owners
☐
Resources identified and committed
☐
Milestones scheduled
☐
Review rhythm agreed
☐
Plan documented and shared
☐
Technical and Quality Transfer
Item
Done
Work instructions written for key operations
☐
Reference samples mounted at stations
☐
Operators trained and records kept
☐
Inspectors trained on measurement
☐
Measuring equipment available and checked
☐
Incoming and in-process checks operating
☐
Corrective action process in use
☐
Capacity and Delivery
Item
Done
Order register in place
☐
Capacity model built by process
☐
Quotations based on capacity
☐
Material availability confirmed before start
☐
Progress reviewed daily
☐
Bottleneck identified and managed
☐
Commercial and Verification
Item
Done
Volume commitment stated
☐
Payment terms predictable
☐
Performance linked to allocation
☐
Metrics compared against baseline
☐
Improvement verified with evidence
☐
Recognition given for milestones met
☐
The Eight Rules
Rule
Reason
Record the baseline before starting
Progress otherwise unmeasurable
Work on the line, not in the meeting room
Systems on paper do not produce goods
Write the standard down
Verbal knowledge leaves with staff
Prioritise by customer effect
Resources are always limited
Give the plan an owner at both ends
Unassigned actions do not happen
Link improvement to commercial reward
Otherwise improvement reverses
Verify with records, not assurances
Evidence makes the claim checkable
Decide early on replacement
Delay perpetuates the cost
FAQ
What is the difference between a supplier audit and supplier development?
An audit measures and reports; development changes what the supplier can do. An audit produces a score and a list of findings, and if that is where the relationship ends, the findings become a recurring set of observations rather than a fix. Development takes the audit result as a baseline, prioritises the gaps by their effect on the program, assigns owners and resources, and works until the capability is measurably different. The audit is the diagnostic step; development is the treatment.
How do we know whether a supplier can actually improve?
Look at what happened after the last set of findings. A supplier that engaged, changed something, and produced records is capable of improving even if the first attempt was imperfect. A supplier that agreed to everything and changed nothing is a different problem, which is commercial rather than technical. The most reliable indicator is the response to a small, well-defined request: a supplier that completes a modest action on time will usually complete a larger one, and one that does not will not.
How long does supplier development take?
Quick wins can appear within weeks: a mounted reference sample, a reissued specification, or a simple incoming inspection record often removes an entire class of defect immediately. Structural changes take longer, typically three to six months for a functioning planning or quality system, and a full capability change measured by reassessment usually takes a year of sustained work. The variable that matters most is not the size of the gap but whether someone inside the factory owns the work.
Who should pay for the improvements?
It depends on what is being improved and who benefits. Equipment that the factory will use for every customer is normally a factory investment, sometimes supported by a volume commitment. Training and documentation provided by the buyer are usually a buyer cost, because they represent transferred knowledge. Where a specific capability is required for the buyer’s product alone, sharing the cost is reasonable. What should be avoided is a buyer funding general capability that the factory then uses to serve competitors at a lower price.
What if the supplier improves and then reverts?
Reversion usually means the improvement was a behaviour rather than a system. If a corrective action was applied without updating the procedure, it disappears as soon as attention moves elsewhere. The remedy is to standardise: write the change into the work instruction, update the inspection record, and make the new practice part of the routine review. Reversion is also a signal that the commercial side is misaligned, since a supplier under continuous price pressure will return to whatever was cheapest.
Should development effort go to a weak supplier or a good one?
Both, for different reasons. A capable supplier can be developed into a strategic partner, and the effort there produces access to new product types and better responsiveness. A weaker supplier with high value to the program may be worth developing because the alternative is an expensive replacement with its own learning curve. What should be avoided is spending the same effort on a weak supplier with low volume and no willingness to engage, where the arithmetic does not work.
How many suppliers should be developed at once?
Fewer than most buyers attempt. Development consumes management time on both sides, and a plan without attention is a document rather than a project. Two or three active plans with clear milestones are usually more productive than ten with vague objectives, particularly where the same person on the buyer’s side is responsible for all of them. Once a plan reaches the verification stage it needs less attention, which frees capacity for the next supplier.
What records should we keep?
The baseline assessment, the gap analysis, the plan with owners and dates, the progress log, and the evidence for each milestone. Photographs of the workstation before and after, copies of the written procedures, and training records are particularly useful because they show change over time rather than asserting it. The records serve two purposes: they make progress verifiable, and they survive the departure of the individual who managed the project.
When should we stop developing a supplier?
When the record shows the same finding recurring across several cycles with no engagement, when delivery failures repeat without warning, when integrity is in question, or when compliance obligations are not met. Any of those justifies a formal escalation, and the absence of a response to that escalation is the exit criterion. Continuing to develop a supplier who will not engage is not patience; it is a decision to keep paying the cost of the failure.
Conclusion
Supplier development is the deliberate practice of turning a supplier’s capability into a competitive asset. It is cheaper than replacement, it retains knowledge that has already been built, and it produces improvements that persist because they live in the factory’s systems rather than in the buyer’s supervision.
The method is consistent from beginning to end. Assess against defined dimensions and collect evidence on the line rather than in the meeting room. Turn the assessment into a prioritised gap list weighted by effect on the customer, and separate quick wins from structural work.
Give the plan owners at both ends, resources, milestones, and a review rhythm, and write the standards down so they survive staff turnover.
Build the quality system until the factory can find its own problems, build the planning system until its promises are achievable, and align the commercial terms so improvement is rewarded rather than squeezed away. Measure against the recorded baseline, verify with records rather than assurances, and decide early when a supplier will not engage.
For factories, development is how a plant moves up the value chain: a factory that absorbs new methods, documents them, and can prove the improvement wins programs that go beyond its current capability.
For buyers, the practical starting point is the baseline. Record what the supplier can do today, choose the two or three gaps that affect the customer most, and resource the work as a project with a named owner rather than as an expectation. The capability that results belongs to the factory, but the advantage of having it belongs to whoever built it first.