How Does Supplier Quality Engineering Work in Backpack Programs?
How Does Supplier Quality Engineering Work in Backpack Programs?
A backpack manufacturer controls its own sewing floor, but it does not control where the zipper tape, the webbing, the coated fabric, or the buckle come from. Roughly the majority of the defect causes that reach a finished bag originate outside the factory gate, in a material lot or a moulded part that arrived with a certificate but not with the performance the certificate implied.
Supplier quality engineering is the function that closes that gap. It is not purchasing, and it is not incoming inspection. It is the discipline of defining what a supplier must be able to do, verifying that they can do it, controlling what arrives, and forcing correction when something goes wrong. In a bag program it is the difference between a factory that reacts to material problems and one that prevents them.
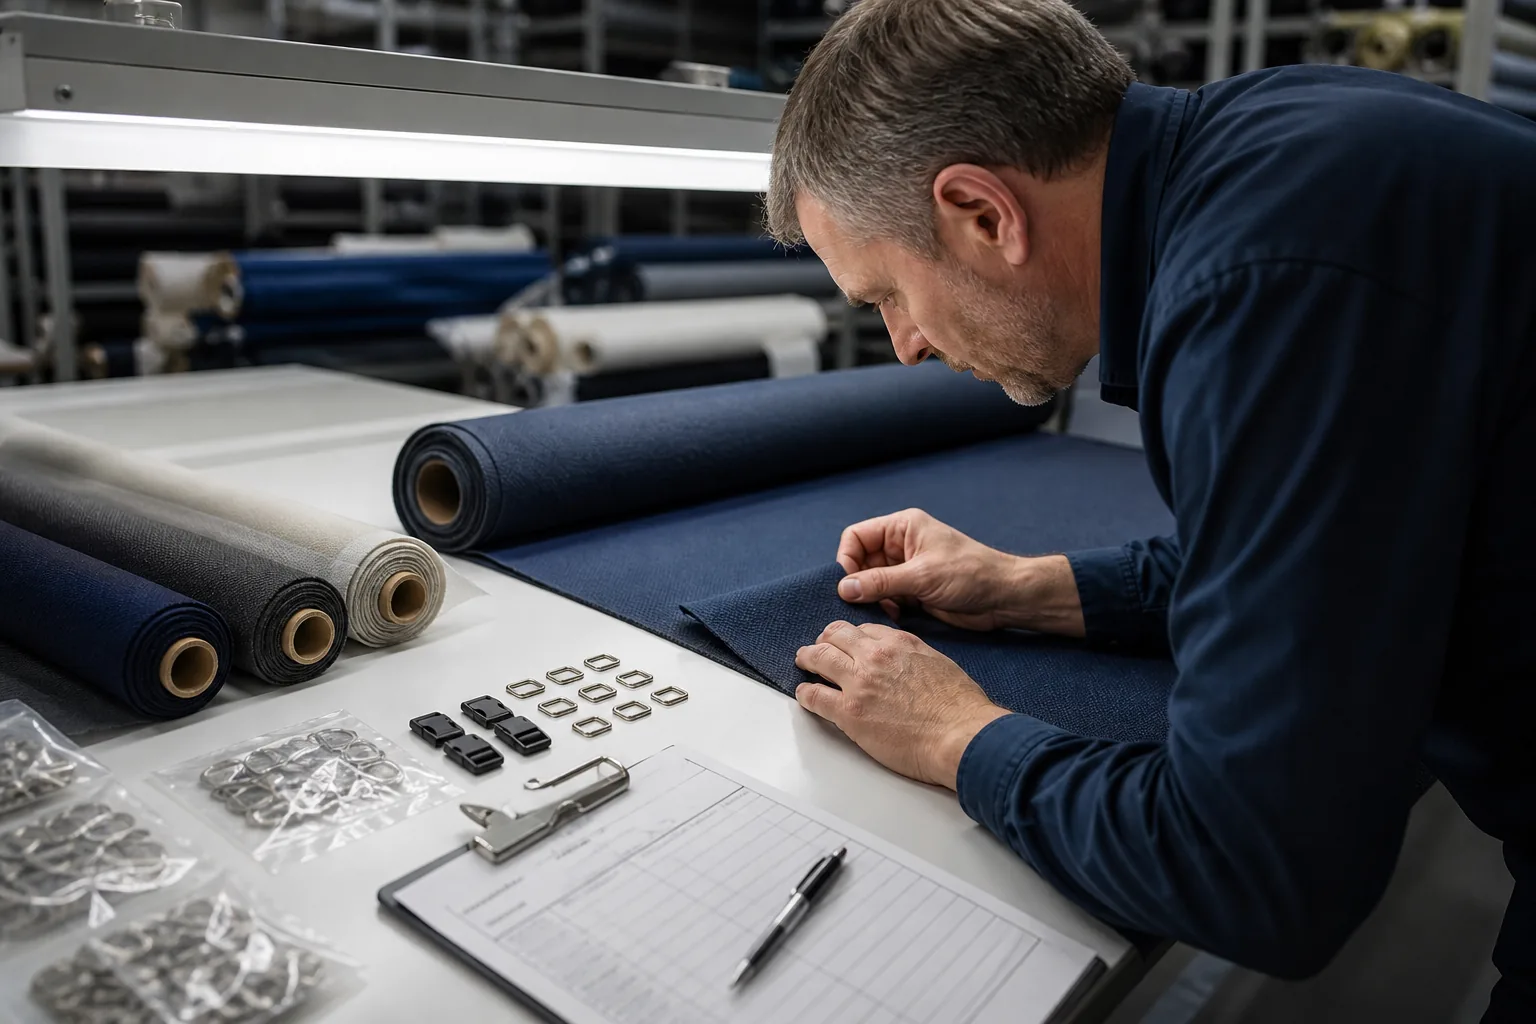
Quality engineer reviewing incoming components with a supplier representative
This guide covers supplier quality engineering for backpack and bag manufacturing programs: what the function owns, how suppliers are evaluated and approved before the first order, and how incoming quality control is structured.
It then covers what a submission package should contain, how nonconformances are handled and how an 8D report is judged, how supplier performance is measured and scored, how weaker suppliers are developed, and how risk and escalation are managed across a supplier base.
Supplier quality engineering sits between the purchasing decision and the production line. Its scope is narrow enough to be measurable and broad enough to cover everything that arrives at the factory door.
The Responsibility Table
Area
Ownership
Supplier evaluation
Assess capability before approval
Specification clarity
Ensure requirements are written and understood
Incoming control
Define inspection and sampling
Submission review
Approve samples and documentation
Nonconformance
Raise and track supplier defects
Corrective action
Review 8D and verify effectiveness
Performance measurement
Score and report supplier quality
Development
Raise capability of weaker suppliers
Risk
Map dependency and plan mitigation
The Boundary Table
Activity
Owner
Price and terms
Purchasing
Delivery scheduling
Planning
Technical specification
Design and engineering
Incoming inspection execution
Quality control team
Supplier process capability
Supplier quality engineering
Corrective action approval
Supplier quality engineering
The Failure Origin Table
Origin
Typical defect
Fabric mill
Shade variation, width, coating adhesion
Webbing supplier
Strength, elongation, colour
Zipper maker
Slider function, chain tolerance
Hardware moulder
Tolerance, flash, gate strength
Foam and padding
Density, thickness, resilience
Thread supplier
Strength, colour, lubricity
Trim and label
Adhesion, legibility, placement
The Cost of Arrival Defects Table
Cost
Character
Sorting labour
Direct and unplanned
Rework
Consumes line capacity
Scrap
Material and labour lost
Line stoppage
Delivery risk
Expedited replacement
Premium freight
Customer claim
Commercial exposure
Manufacturer note: The first question in supplier quality is not whether the material is good. It is whether the requirement was written down in a way the supplier could meet. A significant share of incoming defects are specification failures rather than manufacturing failures: a colour described as “dark grey” instead of given as a measured reference, a coating adhesion never quantified, a webbing strength stated as a nominal figure with no tolerance.
Supplier Evaluation and Approval
A supplier is approved on evidence, not on a sample. The evaluation establishes whether the supplier has a system capable of producing the requirement repeatedly, which is a different question from whether one sample looked correct.
Supplier audit in progress on a bag factory production floor
The Evaluation Dimension Table
Dimension
What is assessed
Process capability
Equipment and control
Quality system
Documented and followed
Material control
Incoming, storage, traceability
Measurement
Instruments and calibration
Competence
Skills and training
Capacity
Volume and lead time
Sub-tier control
Their own suppliers
Corrective action
Response to past problems
The Evaluation Method Table
Method
Use
Questionnaire
Initial screening
Document review
System evidence
Site audit
Verify what happens on the floor
Sample submission
Prove capability on the part
Trial order
Prove capability at volume
Reference check
Verify past performance
The Audit Scope Table
Area
Evidence sought
Receiving
Records and material identification
Storage
Condition and segregation
Production
Control plan performed
In-process checks
Records at the station
Final inspection
Sampling and criteria
Calibration
Certificate and schedule
Nonconformance
Segregation and disposition
Training
Records for the operators
The Rating Table
Rating
Meaning
Approved
Capable for the intended part
Conditionally approved
Approved with restrictions
Development required
Needs work before volume
Not approved
Not suitable
The Approval Condition Table
Condition
Example
Enhanced inspection
Higher sampling level
Additional documentation
Certificate per batch
Restriction
Limited to certain parts
Review period
Reassessment after a set time
Capacity cap
Volume limited
The Requirement Package Table
Document
Purpose
Specification
Performance requirements
Drawing
Dimensions and tolerances
Colour reference
Physical standard
Test method
How to verify
Packaging requirement
Protection and identification
Label requirement
Traceability
Change notification
Supplier obligation
Nonconformance procedure
Reporting route
The Sample Approval Table
Step
Evidence
Sample submitted
Identified and dated
Test performed
Recorded result
Comparison with standard
Visual and measured
Approval decision
Signed and dated
Retained sample
Kept for reference
Production reference
Golden sample issued
The Change Control Table
Change
Supplier must
Material
Notify and resubmit
Process
Notify before implementation
Sub-tier supplier
Notify and requalify
Site or line
Notify and re-audit
Tooling
Notify and requalify
Incoming Quality Control and Submission Requirements
Incoming control is where the supplier’s promises meet the factory’s requirements. It has to be strong enough to prevent a bad lot from entering production, and efficient enough not to become a bottleneck.
Incoming quality control bench with fabric and hardware being measured
The Inspection Level Table
Level
Applied to
Skip lot
Proven stable supplier
Reduced
Consistent history
Normal
Standard sampling
Tightened
Recent problems
Full inspection
Critical or unproven
The Sampling Table
Factor
Consideration
Lot size
Determines sample size
Criticality
Safety and functional parts
Supplier history
Drives the level
Cost of escape
Justifies higher levels
Measurement cost
Balanced against risk
The Test Type Table
Test
Application
Visual
Colour, finish, defects
Dimensional
Width, thickness, length
Physical
Strength, elongation, adhesion
Functional
Fit with the mating part
Chemical
Restricted substances documentation
Packaging
Protection and identification
The Certificate Table
Document
Content
Material certificate
Grade and batch
Test report
Measured values
Compliance statement
Restricted substances
Packing list
Quantity and lot
Traceability label
Lot and date
The Submission Package Table
Element
Purpose
Sample parts
Prove the part itself
Dimensional report
Prove measurement
Material certificate
Prove the input
Process description
Prove the method
Control plan
Prove ongoing control
Test results
Prove performance
Approval signature
Formal acceptance
The Receiving Decision Table
Outcome
Action
Accepted
Release to store
Accepted with note
Release, record the deviation
Rejected
Segregate and notify
Held
Await test result
Sorting required
Contain and screen
The Segregation Table
Status
Handling
Accepted
Identified and located
Quarantine
Physically separated
Rejected
Marked and controlled
Return pending
Documented and protected
Nonconformance and Corrective Action
How a factory handles a supplier defect determines whether the problem repeats. The objective is not to punish the supplier but to remove the cause so that the next lot is correct.
The Nonconformance Step Table
Step
Action
1
Contain the affected material
2
Document the defect with evidence
3
Notify the supplier formally
4
Require a corrective action response
5
Review and challenge the analysis
6
Verify the effectiveness
7
Close and record
Corrective action meeting with defective samples and documents on the table
The Containment Table
Action
Detail
Stop the line
If the material is in production
Sort the lot
Separate conforming from not
Recall the material
From stores and work in progress
Check the previous lots
Same supplier and batch
Protect the customer
Screen finished goods
The Notification Table
Element
Content
Reference
Supplier and lot
Defect description
What is wrong
Evidence
Photographs and measurements
Quantity affected
Units or metres
Requirement breached
Which specification
Response required
Format and deadline
The 8D Structure Table
Discipline
Content
D1
Team formed
D2
Problem described
D3
Interim containment
D4
Root cause identified
D5
Corrective action chosen
D6
Action implemented and validated
D7
Systemic prevention
D8
Closure and recognition
The Root Cause Table
Level
Question
Occurrence
Why did it happen?
Escape
Why did it reach us?
Systemic
Why did the system allow it?
The Review Test Table
Test
Purpose
Is the cause specific?
Rules out restatement
Is the evidence consistent?
Rules out guesswork
Does the fix address the cause?
Rules out a cosmetic action
Is the date committed?
Enables tracking
Is it verifiable?
Enables closure
The Verification Table
Method
Applied when
Next lot inspection
Routine
Increased sampling
Moderate risk
Full inspection for a period
Higher risk
Process audit
Systemic concern
Test of the corrected part
Design or material change
The Escalation Table
Occurrence
Action
First
Standard nonconformance
Repeated
Formal warning and tighter inspection
Chronic
Development plan or capacity restriction
Unresolved
Sourcing review
The Cost Recovery Table
Cost
Basis
Sorting labour
Hours spent
Rework
Hours and material
Scrap
Material value
Freight
Expedited shipment
Line disruption
Agreed rate
Manufacturer note: A corrective action is only closed when the next delivery proves it. A supplier that submits a well-written report and then ships the same defect is worse than one that submits a poor report and fixes the process, because the paperwork creates the impression of control where none exists. The verification step is what distinguishes a real corrective action programme from a filing exercise.
Supplier Scorecards and Performance Review
Measurement changes behaviour, but only if the supplier can see the measurement and understands how it is calculated. A scorecard that is published, explained, and used in sourcing decisions is a control; one that stays in a folder is not.
The Scorecard Metric Table
Metric
Definition
Incoming lot acceptance
Accepted lots as a share of lots received
Defect rate
Defective units per thousand
On-time delivery
Deliveries within the agreed window
Corrective action closure
Responses closed on time
Documentation accuracy
Certificates correct on first submission
Claim rate
Field claims attributed to the component
The Weighting Table
Metric
Weight
Quality
Highest
Delivery
Significant
Documentation
Moderate
Responsiveness
Moderate
Cost
Commercial, tracked separately
The Grading Table
Grade
Meaning
Consequence
A
Strong performer
Preferred, reduced inspection
B
Acceptable
Standard control
C
Marginal
Development plan
D
Below requirement
Sourcing review
The Review Rhythm Table
Frequency
Activity
Monthly
Data collected and shared
Quarterly
Formal review meeting
Annually
Full reassessment
On event
After a significant defect
The Data Source Table
Data
Source
Lot acceptance
Incoming inspection records
Defect quantity
Nonconformance records
Delivery
Goods received notes
Corrective actions
Response register
Field claims
Warranty records
The Communication Table
Element
Practice
Published score
Shared with the supplier
Basis explained
Method transparent
Trend shown
Compared with previous periods
Actions agreed
Written and dated
Consequences stated
Linked to sourcing
Developing Weaker Suppliers
Not every supplier that scores poorly should be replaced. Where the part is critical, the tooling is specific, or the alternative is worse, development is the better commercial decision.
The Development Trigger Table
Signal
Response
Repeated lot rejections
Process review at the supplier
Documentation failures
Training on submission
Slow corrective action
Escalation and support
Capability gap on a new part
Joint development
Capacity shortfall
Planning support
The Support Type Table
Type
Application
On-site coaching
Process and inspection method
Training session
Documentation and standards
Shared inspection fixtures
Measurement consistency
Supplier to supplier learning
Benchmarking
Joint improvement project
Structural capability
The Development Plan Table
Element
Content
Gap
Measured deficiency
Action
Specific step
Owner
Supplier and factory
Evidence
What proves completion
Milestone
Date
Review
Frequency
The Capability Milestone Table
Stage
Evidence
Documented procedure
Written and issued
Operator trained
Record present
Measurement in place
Calibrated instruments
Control applied
Records at the process
Capability shown
Consistent results over lots
The Exit Decision Table
Situation
Decision
Improving on plan
Continue
Improving too slowly
Reassess scope
Unwilling to change
Reduce or exit
Unable and critical
Dual source
Part easily resourced
Replace
Risk, Dependency and Multi-Sourcing
Supplier quality risk is a function of two things: how likely a supplier is to fail, and how much damage that failure would cause. Both have to be managed together.
The Risk Matrix Table
Likelihood
Impact
Priority
High
High
Immediate action
High
Low
Contain and monitor
Low
High
Dual source
Low
Low
Routine control
The Dependency Table
Factor
Raises risk
Single source
Yes
Custom tooling
Yes
Long lead time
Yes
Specialised process
Yes
Small supplier base
Yes
Geographic concentration
Yes
The Single Source Table
Reason
Mitigation
Proprietary part
Hold safety stock
Tooling investment
Retain tooling rights
Capability unique
Develop an alternative
Commercial agreement
Negotiate a second source clause
The Dual Source Table
Element
Requirement
Specification identical
Same requirements
Approval both
Both qualified
Split allocation
Defined proportion
Common standard
Same reference sample
Regular comparison
Ongoing checks
The Continuity Table
Risk
Plan
Supplier fails suddenly
Safety stock
Quality collapse
Alternative approved source
Delivery failure
Backup logistics
Compliance withdrawal
Alternative material
The Business Continuity Table
Element
Practice
Critical part list
Identified and maintained
Buffer level
Set against lead time
Alternative approval
Maintained, not lapsed
Contact list
Updated
Trigger points
Defined in advance
The Escalation Path Table
Level
Action
1
Quality engineer contacts the supplier
2
Formal notice with a deadline
3
Management meeting and a plan
4
Commercial consequence
5
Exit or replacement
Setting Up a Supplier Quality Programme
A supplier quality programme can start with one engineer and a defined scope. What matters is that the scope is written down, the responsibilities are assigned, and the same standard is applied to every supplier that matters.
The Programme Element Table
Element
Content
Scope
Which suppliers and which parts
Critical part list
Parts that affect the customer
Approval process
How a supplier is approved
Incoming plan
Levels and sampling
Nonconformance route
How a defect is raised
Response requirement
Format and deadline
Scorecard
Metrics and weighting
Review rhythm
Meeting frequency
Development process
How a weak supplier is helped
Escalation path
How a chronic problem is handled
The Critical Part Table
Category
Example
Customer-facing appearance
Shell fabric and colour
Load-bearing
Webbing, thread, hardware
Functional
Zippers and closures
Protective
Lining and padding
Compliance-related
Restricted substance content
Identification
Labels and branding
The Role Table
Role
Responsibility
Supplier quality engineer
Approval, control, corrective action
Incoming inspector
Execute inspection and record
Purchasing
Terms, escalation, sourcing
Design engineer
Specification clarity
Production
Feedback on line defects
Management
Review and resource decisions
The Document Set Table
Document
Owner
Supplier specification
Design
Approval record
Supplier quality
Incoming inspection plan
Supplier quality
Nonconformance register
Supplier quality
Corrective action register
Supplier quality
Scorecard
Supplier quality
Audit report
Supplier quality
The Programme Start Table
Step
Activity
1
List all suppliers and classify by importance
2
Write the requirement for the critical ones
3
Approve against evidence
4
Define incoming control by risk
5
Set the nonconformance route
6
Start the scorecard
7
Hold the first review
The Data System Table
Record
Purpose
Supplier master
Contact and status
Part and supplier link
Which supplier supplies which part
Lot record
What arrived and when
Inspection result
What was found
Defect record
What went wrong
Corrective register
What was promised
The Documentation Discipline Table
Practice
Reason
One reference per defect
Enables tracing
Photographs attached
Removes ambiguity
Measurement recorded
Removes argument
Deadlines stated
Enables follow-up
Closure evidence required
Prevents paper closure
Cost, Benefit and Programme Metrics
Supplier quality engineering carries a cost, and the return appears as avoided cost elsewhere. Making that visible is what keeps the function resourced.
The Programme Cost Table
Element
Character
Engineer time
Salaried, recurring
Inspection labour
Recurring
Test and measurement
Equipment and consumables
Audits and travel
Periodic
Sorting and rework
Charged or absorbed
Held stock
Working capital
The Avoided Cost Table
Avoided cost
Mechanism
Line stoppage
Material arrives conforming
Rework hours
Fewer defects to correct
Scrap
Less material discarded
Customer claim
Fewer field failures
Expedited freight
Fewer emergency replacements
Sorting labour
Fewer hold-and-screen events
The Programme Metric Table
Metric
Meaning
Supplier defect rate
Trend over time
Cost of poor supplier quality
Financial impact
Corrective action closure time
Responsiveness
Approved supplier share
Base health
Repeat defect share
Whether causes are removed
The Baseline Table
Step
Activity
1
Count current incoming rejections
2
Estimate sorting and rework hours
3
Estimate line stoppage time
4
Record the current claim data
5
Convert to a cost figure
6
Re-measure after the programme matures
The Maturity Table
Level
Character
1
Inspection only
2
Documented incoming control
3
Approval and scorecards
4
Structured corrective action
5
Supplier development and prevention
The Review Agenda Table
Item
Purpose
Data pack
Shared in advance
Performance summary
Trend and grade
Open corrective actions
Status and blockers
Repeat issues
Escalation
Improvement actions
Agreed next steps
Risk items
Dependency and continuity
The Communication Rule Table
Principle
Practice
Same data to both parties
No hidden scoring
Written outcomes
Actions recorded
Deadlines explicit
Dates not intentions
Consequences stated
Linked to sourcing
Recognition given
Good performance acknowledged
Manufacturer note: The most common reason a supplier quality programme loses momentum is that the data never reaches a decision. If the scorecard does not influence how much inspection a supplier receives, how much business they are offered, or how much support they get, the supplier learns that the score is administrative and behaves accordingly. The programme works when the number changes something.
Common Weak Points in Bag Supply Chains
Certain failures recur across bag programs regardless of the factory, because they come from the structure of the industry rather than from any one supplier.
The Recurring Issue Table
Issue
Underlying cause
Shade variation between lots
Dye lot spread and no physical standard
Coating adhesion failures
Unspecified adhesion requirement
Webbing breaking below expectation
Nominal strength quoted without tolerance
Hardware tolerance drift
Mould wear not monitored
Zipper function complaints
Slider tolerance and chain misalignment
Label adhesion failures
Substrate not specified to the label supplier
Foam losing loft
Density specified, resilience not
Thread colour mismatch
No agreed reference under a standard light
The Structural Cause Table
Structure
Consequence
Many small suppliers
Limited control over each
Trading intermediaries
Factory not visible to the buyer
Seasonal demand peaks
Capacity stretched, control loosened
Price pressure
Specification quietly reduced
Short development cycles
Requirements written late
The Preventative Table
Measure
Effect
Physical standard for colour
Removes interpretation
Measured requirement plus tolerance
Removes nominal ambiguity
Reference sample retained
Enables comparison over time
Defined test method
Enables consistent verification
Sub-tier visibility
Reveals where the material is made
The Seasonal Table
Condition
Risk
Peak season
Rushed production and inspection
New operators
Skill variation
Substitute materials
Unapproved change
Overtime shifts
Reduced attention
Multiple styles at once
Mix-ups between parts
The Supplier Quality Checklist
Supplier Management
Item
Done
Suppliers classified by importance
☐
Critical part list maintained
☐
Specification issued to each supplier
☐
Approval based on evidence
☐
Approval conditions recorded
☐
Change notification requirement stated
☐
Supplier contact and status current
☐
Incoming Control
Item
Done
Inspection level defined per supplier
☐
Sampling plan documented
☐
Test methods specified
☐
Certificates checked on arrival
☐
Inspection records retained
☐
Quarantine area controlled
☐
Decision recorded per lot
☐
Nonconformance
Item
Done
Defect documented with evidence
☐
Material contained and sorted
☐
Supplier notified formally
☐
Response required in a stated format
☐
Deadline set
☐
Root cause challenged
☐
Effectiveness verified
☐
Cost recovered where agreed
☐
Performance and Risk
Item
Done
Scorecard calculated monthly
☐
Score shared with the supplier
☐
Review meeting held
☐
Development plans active
☐
Dependency mapped
☐
Single sources identified
☐
Continuity plan documented
☐
The Eight Rules
Rule
Reason
Write the requirement before judging the part
Prevents specification disputes
Approve on systemic evidence
A sample proves nothing about repetition
Match inspection level to risk
Controls cost and attention
Contain before investigating
Protects the line
Demand a specific root cause
Restatement is not analysis
Verify on the next delivery
Paperwork is not correction
Publish the scorecard
Measurement changes behaviour
Link the score to a decision
Otherwise the data is ignored
FAQ
How is supplier quality engineering different from incoming inspection?
Incoming inspection is the act of checking what arrives. Supplier quality engineering is the system that decides what should be checked, at what level, for which supplier, against which requirement, and what happens when the check fails. Inspection is one instrument inside the function. A factory with inspection but no supplier quality engineering tends to inspect everything at the same level, which wastes effort on stable suppliers and under-controls the risky ones, and treats each rejection as an isolated event rather than a signal about the supplier’s process.
Do we need to audit every supplier?
No, and attempting it usually means auditing none of them properly. Suppliers should be classified by the importance of what they provide, and the depth of evaluation should follow that classification. A supplier of a critical, load-bearing component, or of a fabric whose shade consistency affects the visible product, deserves a site audit and a full approval package. A supplier of a simple trim item with a stable history and a simple specification can be approved on documentation and a sample. The objective is to spend evaluation effort where a failure would hurt the most.
What should an incoming inspection plan contain?
It should state, for each part and supplier, the characteristics to be checked, the method and instrument, the sampling level, the acceptance criteria, and the action to take on a result outside the criteria. It should also state the level of certificate checking required on arrival, because a certificate that is never compared with the shipment provides no control. Without these elements written down, inspection becomes a matter of whichever inspector happens to receive the lot, and consistency between shifts and between sites disappears.
What makes an 8D report acceptable?
A specific root cause supported by evidence, and a corrective action that addresses that cause rather than the symptom. The common failure is a report whose root cause section restates the defect, such as “operator carelessness” without identifying what in the process allowed the error to occur and to escape. Beyond the analysis, an acceptable report commits to a dated action, names a responsible person, and states how the effect will be verified. The verification is what the factory should hold the supplier to, because it is the only part of the report that can be tested.
How do we handle a supplier who ships a defect after promising a fix?
Escalate, and tighten the control at the same time. The immediate response is to raise the inspection level for that supplier, contain any material already in the plant, and notify them formally with the evidence that the correction did not work. The commercial response is to place the supplier on a development plan with defined milestones, or to restrict the share of business they are offered. Where the part is critical and the supplier does not improve, the correct decision is usually to qualify an alternative rather than to keep absorbing the cost.
Should a scorecard weight quality above delivery and cost?
Quality should carry the highest weight where the part affects the customer or the load path, because a delivery that arrives early with a defect is worth less than a delivery that arrives on time and correct. Delivery still matters, and a supplier who consistently ships late creates its own cost, so it should not be ignored. Cost is best tracked separately, because a supplier who wins on price while generating sorting and claim costs is not cheaper in total. The weighting should reflect the commercial reality of the specific part rather than being fixed across every supplier.
How many samples should be required for approval?
Enough to show repeatability rather than a single good result. One sample demonstrates that the part can be made; several samples taken from a production run demonstrate that it can be made consistently, which is the question that matters. The number should be proportionate to the risk, with more samples for a critical or complex part and fewer for a simple trim. Samples should be taken from normal production rather than prepared specially for submission, and at least one should be retained as the reference for future comparison.
Where does a factory start if it has no supplier quality programme at all?
With a list of suppliers and the parts they supply, sorted by how much damage a failure would cause. From that list, write the performance requirement for the most critical group, because most incoming disputes are caused by a requirement that was never written down in measurable terms. Then define incoming control at a level matched to each supplier’s risk, set up a simple register for defects and corrective actions, and start recording the data. The programme can begin without consultants or software, and it improves as the recorded data begins to show which suppliers and which parts deserve attention.
How does supplier quality engineering connect to traceability?
Directly. When a defect reaches the field and a finished unit can be traced back to the material lot that caused it, the supplier quality function needs to know which supplier, which lot, and which other orders received the same material. That forward trace is what defines the scope of the containment, and its speed depends on whether the lot was recorded at receiving and linked to the work order. A traceability system that stops at the factory gate cannot answer a supplier-origin question, which is why the two functions should be designed together.
Conclusion
Supplier quality engineering exists because a backpack manufacturer cannot inspect quality into materials it did not make. The function writes the requirement, verifies that the supplier is capable of meeting it, controls what arrives, forces correction when something goes wrong, and measures whether the supplier is getting better or worse over time.
The mechanics are consistent from start to finish. Classify suppliers by the damage a failure would cause, and spend evaluation effort accordingly. Approve on systemic evidence rather than a single sample, with the sample taken from normal production.
Define incoming control per supplier and per part, at a level matched to risk, with methods and acceptance criteria written down. Contain any defect before investigating it. Require a specific root cause and a dated action, and verify on the next delivery rather than on the report. Publish the scorecard, and make the score change something the supplier can feel.
For factories, the return appears as line time that is not lost to sorting, rework that is not performed, and claims that are not received. A plant that knows which suppliers are stable, which are marginal, and which parts depend on a single source is in a position to plan rather than to react.
For buyers, the practical test is to ask the supplier how it evaluates its own suppliers, what its incoming inspection level is, and what happened the last time a material failed in production. A factory that answers with records is managing its supply base; one that answers with reassurance is hoping.