Skills Matrices in Bag Factories: How Do You Build a Trained Line?
Skills Matrices in Bag Factories: How Do You Build a Trained Line?
Every bag factory claims its operators are skilled. Very few can show which operator is qualified on which operation, at what level, assessed by whom, on what date, and who else could cover the job if that person were absent tomorrow. The difference between the claim and the evidence is a skills matrix.
This guide covers workforce training and skills matrices from a bag manufacturer’s perspective: why training is a production control rather than a human resources activity, how a skills matrix is structured and used, how operations and skill levels are defined, how training is delivered on the floor, how competence is assessed, how multi-skilling creates line flexibility, how records are maintained, and how the investment is costed and measured.
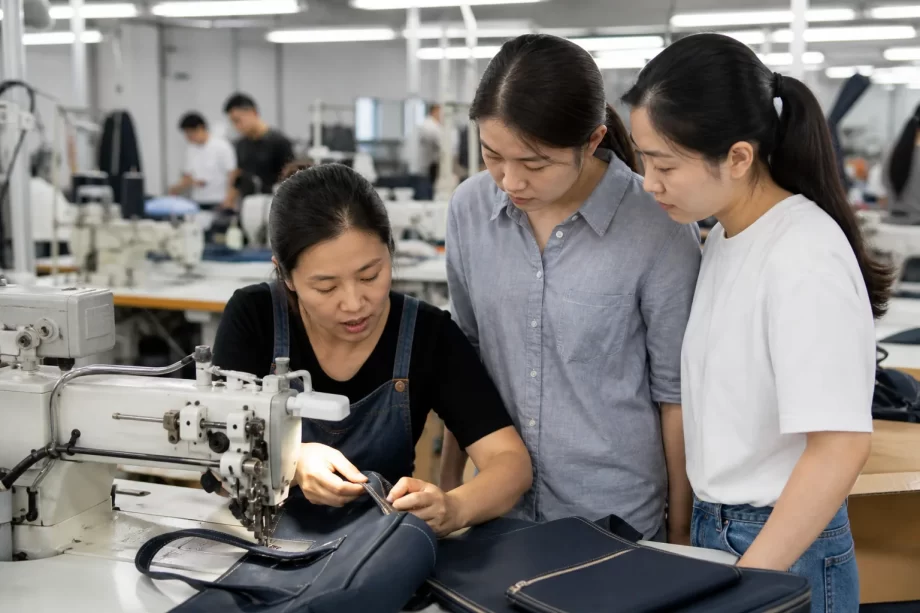
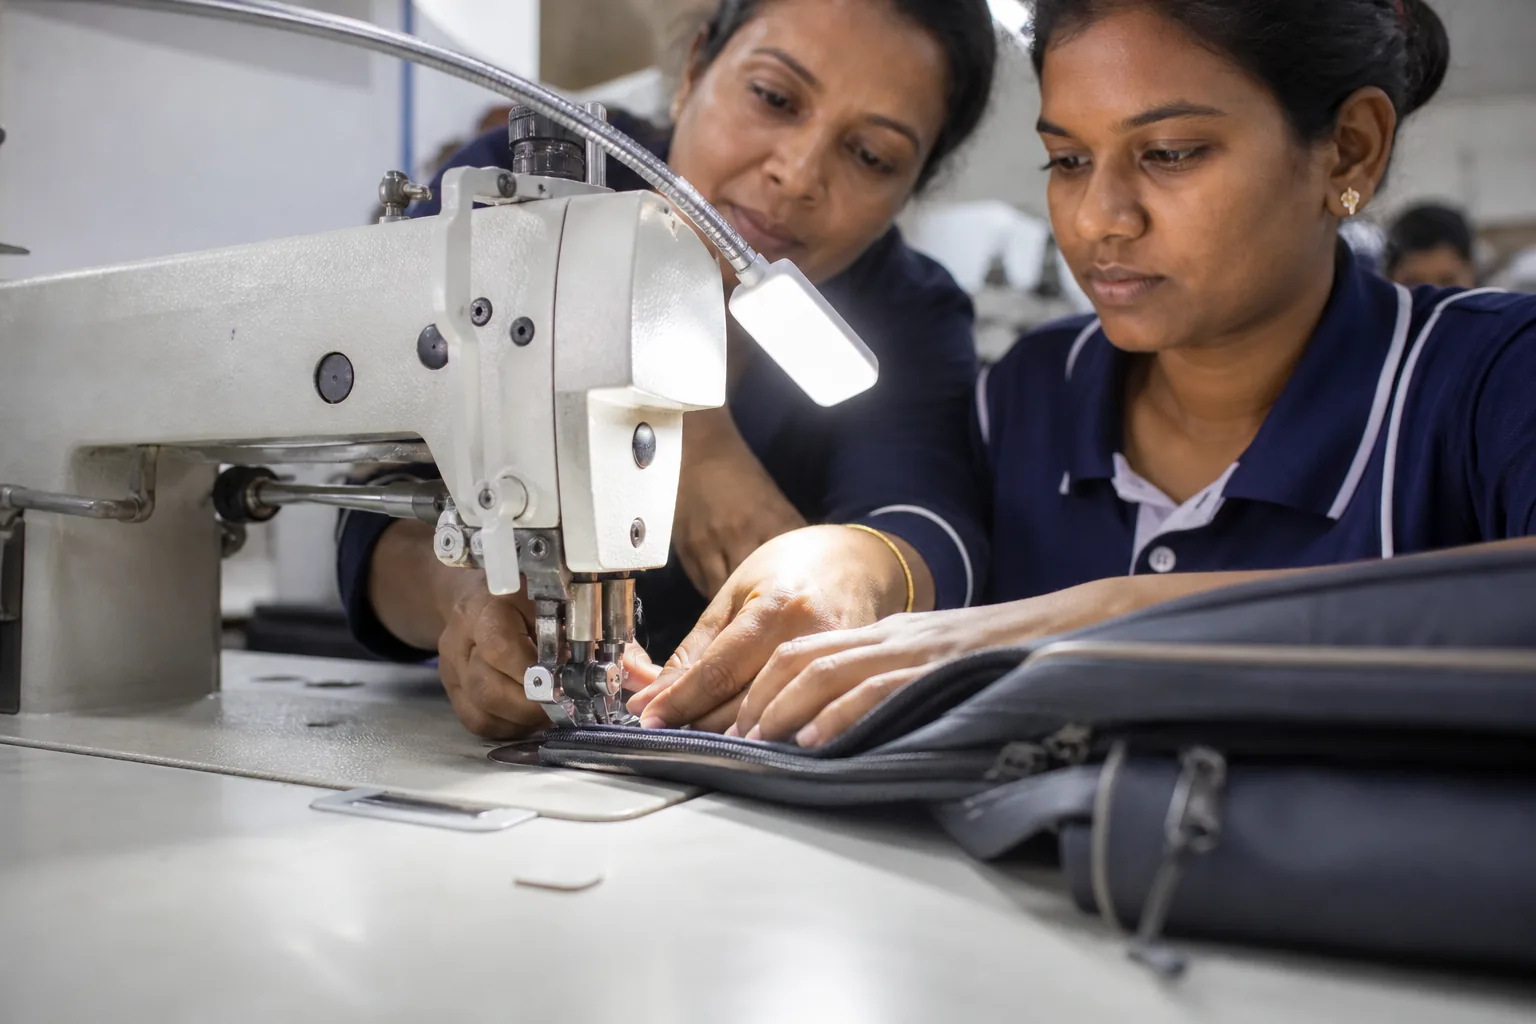
A skilled operator demonstrating a seam technique at an industrial machine to two trainees on a factory floor
Training in a bag factory is usually treated as an onboarding event and then forgotten. A new operator is shown the operation once, produces a few pieces, and is absorbed into the line, where the quality of the work becomes a matter of individual habit.
The factory then discovers the true state of its capability when a key operator leaves, when an order requires an unfamiliar construction, or when a defect trace points back to a single workstation whose occupant was never formally assessed.
A skills matrix sits at the intersection of quality, capacity, and continuity, and it is the only document that makes all three visible at once. Without it, a supervisor knows who is on the line but not what the line can actually do.
The Function Table
Function
Question answered
Quality
Who is qualified on this operation?
Capacity
How many operators can run this operation?
Continuity
Who covers if this person is absent?
Planning
Who can be moved to a new order?
Development
Who is ready for the next level?
Audit
What evidence exists for this claim?
The Cost of No Matrix Table
Consequence
Mechanism
Defects traced to one operator
No assessment record
Line stops on absence
No identified backup
New order delayed
No verified capability
Rework not explained
Skill gap invisible
Training repeated
No record of prior training
Pay disputes
No defined skill levels
The Stakeholder Table
Stakeholder
Use
Line supervisor
Daily allocation
Production planner
Capacity and flexibility
Quality manager
Defect investigation
HR
Development and grading
Buyer or auditor
Capability evidence
Trainer
Gap identification
The Absence Impact Table
Absence type
Effect without a matrix
Planned leave
Cover found by seniority, not skill
Unplanned absence
Line stops at the unstaffed step
Resignation
Capability lost silently
Promotion
Operation left without an owner
Shift change
Coverage assumed, not verified
Peak season
Gaps appear under load
An absence is the moment when an undocumented capability becomes visible. The line that continues at full output through a resignation is a line that knew, in advance, which operations had a second and third qualified operator, and had already planned the move.
The Control Point Table
Control
Purpose
Operation list
Defines the scope
Skill level
Defines the standard
Assessment
Proves the level
Record
Preserves the proof
Review cycle
Keeps it current
Backup count
Protects continuity
Manufacturer note: The most expensive training failure in a bag factory is not a poorly trained operator. It is a well-trained operator whose competence was never recorded, so that when the person moves to another line, resigns, or is promoted, the factory has no way to prove the capability existed and no way to know that it has been lost. A matrix that is filled in once and never updated produces the same outcome, because it describes a factory that no longer exists.
The Skills Matrix: Structure and Use
A skills matrix is a grid with operations on one axis and people on the other, and each cell carries a level. The structure is simple; the discipline is in what the cells mean.
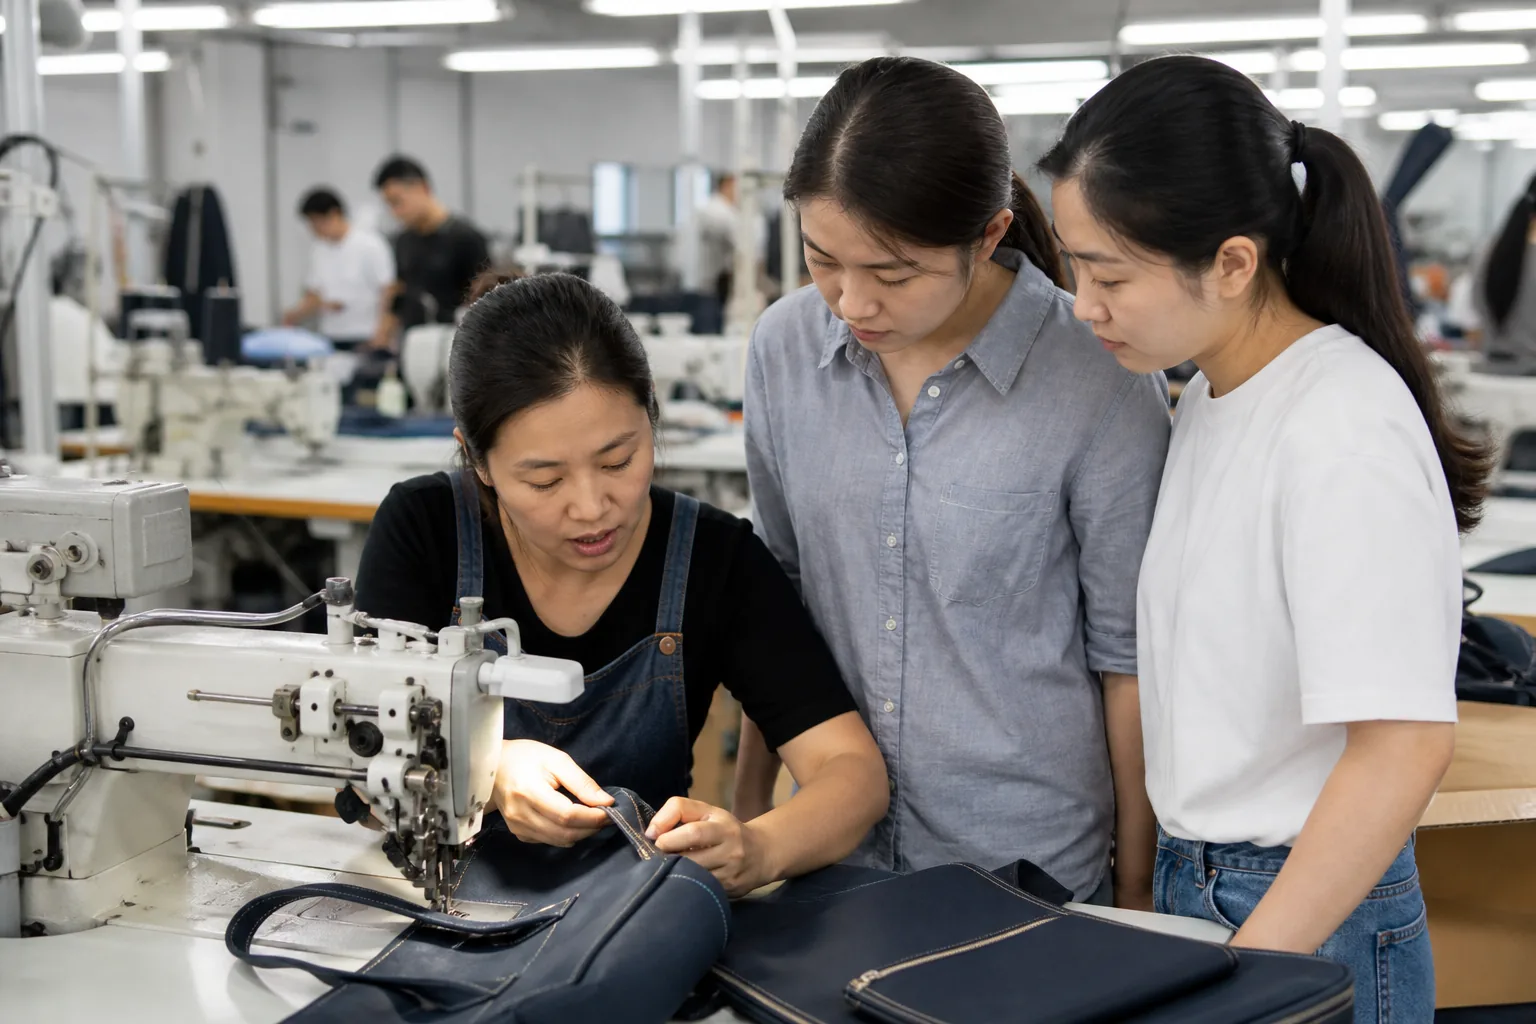
A supervisor reviewing a wall-mounted colour-coded skills grid with a clipboard
The Axis Table
Axis
Content
Rows
People, by team or line
Columns
Operations, in process order
Cell
Skill level and date
Groups
Operation families
Header
Line, shift, section
Footer
Backup count per operation
The Level Table
Level
Meaning
Zero
No training
One
Trained, supervised
Two
Qualified, independent
Three
Qualified, trainer
Four
Expert, trouble-shooter
The Cell Content Table
Element
Purpose
Level
Current capability
Date
When assessed
Assessor
Who confirmed it
Expiry
When to reassess
Note
Restriction or condition
Signature
Accountability
The Visual Coding Table
Colour
Convention
Empty
Not trained
Light
In training
Solid
Qualified
Dark
Trainer level
Hatched
Expiring soon
Marked
Restriction applies
The Reading Table
Pattern in the matrix
Interpretation
Full column, one name
Single point of failure
Full row
Versatile operator
Empty column
No capability at all
Many light cells
Training in progress
Many expiring
Assessment backlog
Even distribution
Balanced team
The Update Table
Trigger
Action
New operator
Add row, begin level one
Assessment passed
Update level and date
Operator leaves
Archive row, review backups
New operation
Add column, assess all
Process change
Reset affected cells
Annual review
Verify all cells
Manufacturer note: The backup count at the foot of each column is the most useful number on the matrix and the one most often omitted. A column with eleven qualified operators and a column with one look identical in a staff count and behave completely differently when someone is absent. Reading the matrix by column minimum rather than by row average is what turns it from a personnel display into a capacity tool.
Defining Operations and Skill Levels
The matrix is only as good as its columns. An operation defined too broadly hides the difference between an operator who can run a straight seam and one who can set a curved seam on coated fabric; an operation defined too narrowly produces hundreds of columns that nobody maintains.
The Operation Breakdown Table
Level of detail
Example
Process stage
Cutting, sewing, finishing
Machine group
Lockstitch, walking foot, bartack
Operation
Join main body side seam
Operation element
Align, sew, backstitch, trim
Critical attribute
Seam allowance, stitch density
Difficulty class
Simple, standard, complex
The Operation Register Table
Field
Content
Operation code
Unique identifier
Description
What is done
Machine
Required equipment
Work content
Standard minutes
Critical quality point
What must not go wrong
Difficulty class
Training time band
Prerequisite
Prior operation required
The Difficulty Table
Class
Character
Simple
Short training, low variation
Standard
Moderate training, defined technique
Complex
Long training, judgement required
Critical
Long training, high consequence
Rare
Infrequent, needs refresher
New
No established standard yet
The Skill Level Definition Table
Level
Evidence required
One
Completed instruction, supervised output
Two
Independent output within tolerance
Three
Consistent output, can instruct others
Four
Solves deviations, sets the standard
The Level Criteria Table
Criterion
Level two threshold
Output rate
Meets standard minutes
Quality
Within the defect limit
Independence
No assistance required
Consistency
Holds across a shift
Documentation
Correctly completed
Safety
No unsafe practice observed
The Training Time Table
Operation class
Typical training band
Simple
Days
Standard
One to two weeks
Complex
Several weeks
Critical
Several weeks plus audit period
Rare
Refresher before each run
New
Undefined until standardised
The Prerequisite Table
Operation
Prerequisite
Curved seam on coated fabric
Straight seam competence
Zipper insertion
Panel alignment
Bartack at stress point
Machine control
Binding a curve
Binding a straight edge
Setting hardware
Reinforcement placement
Final inspection
Full process knowledge
The Standard Work Table
Element
Purpose
Operation sequence
Consistent method
Machine setting
Consistent result
Work content time
Capacity basis
Quality checkpoint
Early detection
Handling method
Prevents damage
Safety requirement
Prevents injury
Manufacturer note: The operation list is where most matrices fail. A factory that defines columns as “sewing” and “finishing” has produced a document that cannot answer any useful question, because both are process stages rather than operations. The practical test is whether a column can be assessed by watching one person perform one task and comparing the result against a written standard. If the column cannot be assessed that way, it is too broad to carry a skill level.
Training Delivery on the Floor
Training in a bag factory happens at the machine, not in a classroom, and the constraint is that production continues while it happens. The method therefore has to be structured enough to be repeatable and small enough to fit around output.
A trainer guiding a trainee’s hands on fabric through a heavy-duty walking foot machine
The Delivery Method Table
Method
Character
Demonstration
Trainer shows the operation
Guided practice
Trainee performs with support
Supervised production
Trainee works on live order
Buddy system
Paired with a qualified operator
Rotation
Moves through operations
Refresher
Returns to a lapsed skill
The Sequence Table
Step
Activity
One
Explain the operation and its quality point
Two
Demonstrate at normal pace
Three
Demonstrate slowly with commentary
Four
Trainee performs with guidance
Five
Trainee performs unaided
Six
Assess against the standard
The Trainer Requirement Table
Requirement
Reason
Level three or above
Can instruct competently
Assessed on the operation
Knows the standard
Trained in instruction
Can transfer the skill
Available time allocated
Training is not incidental
Consistency with standard
Prevents method drift
Feedback loop to quality
Captures recurring errors
The Training Cell Table
Element
Content
Dedicated machine
No disruption to the line
Standard samples
Reference for acceptance
Written standard
Consistent expectation
Material allowance
Practice without cost concern
Time allowance
Scheduled, not borrowed
Record sheet
Evidence of completion
The Timing Table
Approach
Suitability
Before the shift
Short demonstrations
During low load
Guided practice
During peak
Not suitable
Overtime session
Complex operations
Between orders
Rotation and refreshers
Dedicated training week
New line start-up
The Method Drift Table
Cause
Control
Trainer preference
Written standard work
Speed pressure
Standard time enforced
Machine setting change
Setting sheet
Material change
Re-brief on handling
No refresher
Scheduled revisit
No assessment
Periodic re-check
The Common Error Table
Error
Training response
Uneven seam allowance
Guide and slow practice
Puckering
Tension and feed instruction
Missed backstitch
Sequence emphasis
Wrong part orientation
Visual aid at the station
Damaged coating
Handling technique
Skipped checkpoint
Station instruction card
Manufacturer note: Training that borrows time from production is training that gets cancelled when the line is busy, which is precisely when the new operator is needed. Scheduling the training cell as a capacity item, with its own machine, material allowance, and hours in the plan, is what separates factories that develop capability from factories that hope for it. The cost is visible and small; the cost of an unassessed operator on a critical operation is invisible until a shipment is rejected.
Assessment and Certification
Assessment is the step that converts training into a recorded capability. It has to be practical, because the skill is manual, and it has to be criterion-based, because a judgement of “looks good” cannot be defended when a defect appears six weeks later.
An assessor inspecting a sewn backpack panel against a gauge template with graded samples on the table
The Assessment Method Table
Method
What it proves
Observation
Method followed
Output inspection
Result within tolerance
Timed production
Rate achieved
Sample review
Consistency across units
Questioning
Understanding of the quality point
Re-assessment
Retention over time
The Assessment Criteria Table
Criterion
Threshold
Seam allowance
Within the stated tolerance
Stitch density
Matches the specification
Alignment
Within the stated offset
Appearance
No puckering or damage
Rate
Within the standard time band
Safety
No unsafe act observed
The Assessor Table
Requirement
Reason
Level four on the operation
Authority to judge
Independent of the trainee
Avoids bias
Trained in assessment
Consistent criteria
Uses the written standard
Defensible decision
Records the evidence
Traceable outcome
Reviews periodically
Maintains calibration
The Outcome Table
Outcome
Action
Qualified
Level two recorded
Qualified with restriction
Level two plus a note
Not yet competent
Return to guided practice
Competent on one variant
Restricted scope
Competent, trainer potential
Progress toward level three
Lapsed
Refresher and re-assessment
The Certification Table
Element
Content
Certificate
Operation, level, date
Assessor name
Accountability
Validity period
Re-assessment interval
Scope
Variants covered
Restrictions
Conditions of use
Record location
Where evidence sits
The Re-assessment Table
Operation class
Interval
Critical
Short, driven by audit
Complex
Annual
Standard
Annual to biennial
Simple
Biennial
Rare
Before each run
After absence
On return
Multi-Skilling and Line Flexibility
A line staffed by specialists is efficient until someone is absent, an order changes, or a style requires a different balance of work. Multi-skilling is the deliberate development of overlap so that the line can absorb variation without losing output.
The Flexibility Table
Model
Character
Specialist line
High efficiency, low flexibility
Multi-skilled line
Moderate efficiency, high flexibility
Hybrid
Core specialists, flexible support
Cell
Whole-garment teams
Modular
Small teams with overlap
Buffer
Extra operators on critical steps
The Overlap Table
Operation criticality
Minimum qualified
Critical
Three
Complex
Two
Standard
Two
Simple
One plus a trainer
Rare
One plus documented procedure
New
Not yet defined
The Rotation Table
Pattern
Effect
Daily rotation
Broad exposure, slower output
Weekly rotation
Balanced development
Absence cover only
Minimal disruption
Planned cross-training
Steady capability growth
No rotation
Deep specialism, fragile line
Forced rotation
Resentment without purpose
The Development Path Table
Stage
Expectation
Entry
One simple operation
Developing
Two to three operations
Qualified
Core operations at level two
Versatile
Multiple families
Trainer
Level three on key operations
Expert
Level four, sets standard
The Capacity Table
Situation
Matrix response
Absence
Move a qualified backup
Demand spike
Add a second shift from the bench
Style change
Reallocate by operation
New order
Identify gaps before acceptance
Machine breakdown
Redeploy to other operations
Peak season
Plan training before, not during
The Resistance Table
Concern
Response
Pay for extra skills
Define skill-based grading
Fear of redundancy
Explain flexibility as stability
Preference for one task
Recognise and rotate fairly
Trainer time cost
Budget it as capacity
Quality risk in rotation
Assess before deploying
Union agreement
Negotiate the framework
Manufacturer note: Multi-skilling fails when it is presented as a benefit to the factory and a burden to the operator. The factories that make it work tie it to a visible progression: a defined skill level, a recorded assessment, and a pay grade that moves with it. When an operator can see that learning a second operation changes their grade, the matrix stops being an administrative document and becomes the map of their own advancement.
Manufacturer note: The matrix also has a planning use that is easy to overlook. Before quoting a new style, the planner can compare the required operations against the matrix and see immediately whether the line has the capability or whether a training lead time must be built into the delivery date. A quote issued without that check is a promise made on capability the factory has not verified.
Training Records and Traceability
A skill that is not recorded is a skill the factory cannot rely on. Records serve three different audiences: the supervisor who allocates work, the auditor who asks for evidence, and the quality engineer who traces a defect back to its origin.
The Record Table
Record
Content
Skills matrix
Current levels by person
Training log
What was delivered and when
Assessment form
Criteria and outcome
Certificate
Level, scope, validity
Refresher record
Revisit and outcome
Departure record
Capability lost
The Audience Table
Audience
Question
Supervisor
Who can run this today?
Planner
Can we accept this order?
Quality
Who made this unit?
Auditor
Where is the evidence?
HR
What is the grade?
Buyer
How is capability assured?
The Traceability Table
Trace element
Link
Work order
Line and date
Operation
Which step
Operator
Who performed it
Skill level
Was it within scope
Assessment date
Was it current
Inspector
Who checked it
The Retention Table
Record
Retention
Assessment form
Life of employment plus a period
Certificate
Life of employment
Training log
Several years
Matrix snapshot
Per review cycle
Defect trace
Per order
Departure record
Per policy
The Audit Table
Audit question
Evidence
Are operators qualified?
Matrix and certificates
Is training documented?
Training log
Is assessment independent?
Assessor records
Is it current?
Dates against intervals
Are critical operations covered?
Backup count
Are gaps addressed?
Action plan
The System Table
Approach
Character
Paper board
Visible, hard to query
Spreadsheet
Flexible, version risk
HR system
Structured, slow to update
MES link
Traceable to orders
Hybrid
Board plus system
Manual plus audit
Simple, labour-heavy
The medium matters less than the discipline. A paper board updated monthly by the supervisor is more useful than a system nobody maintains, provided the board is the one used for allocation and the one shown in an audit.
The Data Quality Table
Problem
Consequence
Stale cells
Capability overstated
Missing dates
Cannot prove currency
No assessor name
Decision unattributable
Levels not defined
Comparisons meaningless
Duplicate entries
Confusion in allocation
Paper-only storage
Loss and inaccessibility
Costing Training and Measuring Return
Training has a cost and it is usually paid in a budget line that is easy to cut. Making the return visible is what protects the investment when the quarter is tight.
The Cost Table
Cost
Basis
Trainer time
Hours plus opportunity
Trainee time
Hours not producing
Machine time
Occupied equipment
Material
Practice consumption
Assessment
Assessor hours
Administration
Records and review
The Return Table
Return
Mechanism
Lower rework
Fewer defects at source
Higher output
Rate reached sooner
Less absentee impact
Backup coverage
Faster changeover
Multi-skilled allocation
Lower turnover
Visible progression
Fewer claims
Consistent quality
The Payback Table
Investment
Where the return appears
Cross-training a critical step
Absence no longer stops the line
Training a complex operation
Fewer defects at the source
Trainer development
Faster qualification of new staff
Assessment discipline
Defects traceable to a cause
Refresher programme
Fewer lapsed-skill errors
Progression grading
Lower turnover in key roles
The payback is rarely visible in a single line of the accounts, which is why the case has to be argued with operational evidence. A cross-trained critical step shows its value on the day someone is absent, and a trained complex operation shows its value in the rework trend over a quarter.
The Metric Table
Metric
Definition
Qualification rate
Qualified against required
Backup coverage
Operations with two or more
Time to qualify
Days from start to level two
Reassessment compliance
Current against due
Rework by operation
Defects per thousand
Training hours per operator
Annual investment
The Benchmark Table
Indicator
Healthy signal
Critical operations backed up
All
Reassessment overdue
None
Qualification on core
Most of the team
Time to qualify
Within the stated band
Rework trend
Falling
Training hours
Scheduled, not ad hoc
The Business Case Table
Argument
Evidence
Quality
Rework and claim trend
Capacity
Output per operator
Continuity
Absence impact
Flexibility
Changeover time
Retention
Turnover and tenure
Compliance
Audit findings
The Investment Decision Table
Situation
Action
New operation
Train before the order
Single-point failure
Cross-train immediately
High rework
Diagnose the skill gap
New line
Full training plan
Peak approaching
Refreshers in advance
Budget pressure
Protect critical operations
The Training Programme Checklist
Structure
Item
Done
Operation register written
☐
Difficulty classes assigned
☐
Skill levels defined
☐
Assessment criteria written
☐
Matrix built
☐
Backup minimums set
☐
Delivery
Item
Done
Trainers identified
☐
Trainer level confirmed
☐
Training cell equipped
☐
Standard samples available
☐
Hours scheduled in the plan
☐
Standard work documented
☐
Assessment
Item
Done
Assessors appointed
☐
Criteria applied consistently
☐
Output inspected
☐
Rate verified
☐
Outcome recorded
☐
Restrictions noted
☐
Records
Item
Done
Matrix current
☐
Certificates issued
☐
Training log maintained
☐
Reassessment dates set
☐
Traceability link defined
☐
Audit pack available
☐
Development
Item
Done
Progression path published
☐
Skill-based grading agreed
☐
Rotation planned
☐
Cross-training budgeted
☐
Refresher schedule set
☐
Turnover risk reviewed
☐
The Eight Rules
Rule
Reason
Define operations, not departments
Only operations can be assessed
Read the matrix by column minimum
Coverage beats average skill
Record the assessor and the date
Evidence must be attributable
Schedule training as capacity
Unscheduled training gets cancelled
Assess against a written standard
Judgement needs a reference
Cross-train the single-point operations first
Continuity is the largest risk
Tie skill level to a pay grade
Motivation follows recognition
Check the matrix before quoting
Capability constrains delivery
Manufacturer note: A skills matrix is a living document and dies quietly. The failure is rarely a decision to stop maintaining it; it is a month when the line is too busy to update the cells, followed by another, until the document describes a factory that has since changed. The countermeasure is a fixed review rhythm tied to something that already happens, such as the monthly quality review, so the update is a standing agenda item rather than a task that has to be remembered.
FAQ
What exactly is a skills matrix in a bag factory?
It is a grid with operations on one axis and operators on the other, where each cell records whether that person is trained on that operation and at what level, together with the date and the assessor. Its purpose is not to display the workforce but to answer operational questions: who can run this operation today, how many people can cover it if one is absent, and what capability the line would have if this order were accepted. A matrix that cannot answer those three questions is a wall chart rather than a control document.
How many skill levels should a matrix use?
Four working levels are usually enough, with a fifth for the untrained state. Level one means trained but supervised, level two means qualified and independent, level three means able to train others, and level four means able to solve deviations and set the standard. Fewer levels collapse the difference between “has been shown” and “can be relied on”, which is the distinction that matters most for quality. More levels become difficult to assess consistently and tend to produce arguments rather than information.
How do we decide which operations become columns?
The column should be an operation that one person performs on one machine, with a written standard, that can be assessed by watching that person and comparing the result. Anything broader, such as “sewing” or “finishing”, cannot be assessed and therefore cannot carry a level. Anything narrower, such as one specific seam on one specific panel, produces a matrix too large to maintain. The practical calibration is to look at the operation breakdown used for costing, since those operations are already defined at the right granularity for measuring work.
How many qualified operators should each critical operation have?
Three is a common minimum for a critical operation, two for a complex one, and two for a standard one, with the exact number depending on the size of the line and the consequence of a stoppage. The number that matters is not the total across the team but the minimum available on any given day, which is why the backup count belongs at the foot of each column. An operation with eleven qualified operators who all work the same shift has a coverage problem that the total conceals.
Can training be delivered without stopping production?
It can, but not by borrowing time informally. The methods that work are a dedicated training cell with its own machine and material allowance, guided practice during planned low-load periods, and refresher sessions scheduled between orders. The methods that fail are the ones where a supervisor improvises a few minutes on a live line, because that time is the first thing surrendered when the line falls behind. Training hours should appear in the capacity plan as an item with a cost, so that the decision to cut them is a visible decision rather than an invisible one.
How do we make multi-skilling attractive to operators?
By connecting it to something the operator can see. A defined skill level, a recorded assessment, and a pay grade that moves with the level turns the matrix into a progression path rather than an administrative record. Where multi-skilling is presented only as flexibility for the factory, it is received as extra work for the same pay, and the resistance is rational. Publishing the levels, the criteria, and the grading consequence in advance, and applying them consistently, is what makes the programme credible.
How often should the matrix be updated?
On every event that changes a cell, and on a fixed review cycle for everything else. Events include a new operator, a passed assessment, a departure, a new operation, and any process change that invalidates prior competence. The fixed cycle, usually monthly or tied to the quality review, catches lapsed assessments and expired certificates. The failure mode is not a decision to abandon the matrix but a busy month followed by another, until the document describes a factory that no longer exists.
What is the connection between the matrix and quoting new orders?
The matrix is the fastest way to test whether a quoted delivery date is achievable. Before accepting a style, the planner can compare the required operations against the current capability and see which ones have no qualified operator, which have only one, and which would need a training lead time. That check converts an optimistic promise into a planned commitment, and it is the difference between discovering a capability gap at the sampling stage and discovering it a week before shipment.
Conclusion
Training in a bag factory is usually managed as an event at the start of employment and then left to individual habit. The result is a workforce whose capability is real but undocumented, which means it cannot be planned around, cannot be defended in an audit, and cannot be recovered when a key operator leaves.
The work divides into four parts. The first is definition: break the process into operations at the granularity used for costing, assign each a difficulty class, and write the standard that the operation will be assessed against.
The second is the matrix itself, with people on one axis and operations on the other, four working levels, a date and an assessor in every cell, and a backup count at the foot of every column, because coverage rather than average skill is what protects output.
The third is delivery and assessment. Training happens at the machine, so it needs a cell with its own equipment, material allowance, and scheduled hours, and it needs trainers at level three who are working to the written standard rather than to personal preference.
Assessment has to be practical and criterion-based, performed by someone independent and recorded with a name and a date, because an unattributed judgement cannot be defended when a defect surfaces later.
The fourth is the use of the record. The matrix should be read before a quotation is issued, before a new order is accepted, when an absence is notified, and when a defect is traced. At that point it stops being a human resources document and becomes what it should have been from the beginning: the factory’s statement of what it can actually do, on which day, and with how much margin.
For buyers, the practical questions are whether the factory can show a current matrix, whether critical operations have more than one qualified operator, and whether assessments are dated and attributable. For factories, the return is a line that can absorb absence, change style, and take on unfamiliar work without discovering its limits in the middle of a shipment.